Metal Hardware Coating Line: Fast Colour Change and Cost per Part (2026)
Quick answer: A hardware coating line is judged on changeover and hanging density, not top speed. A well-configured line runs 400 to 2,000 parts per hour at 1.0 to 3.0 m/min, changes colour in 10 to 25 minutes, and holds 95 to 98 percent powder utilisation. Direct cost lands around USD 0.06 to 0.45 per part depending on size. Line cost is USD 120,000 to 600,000.
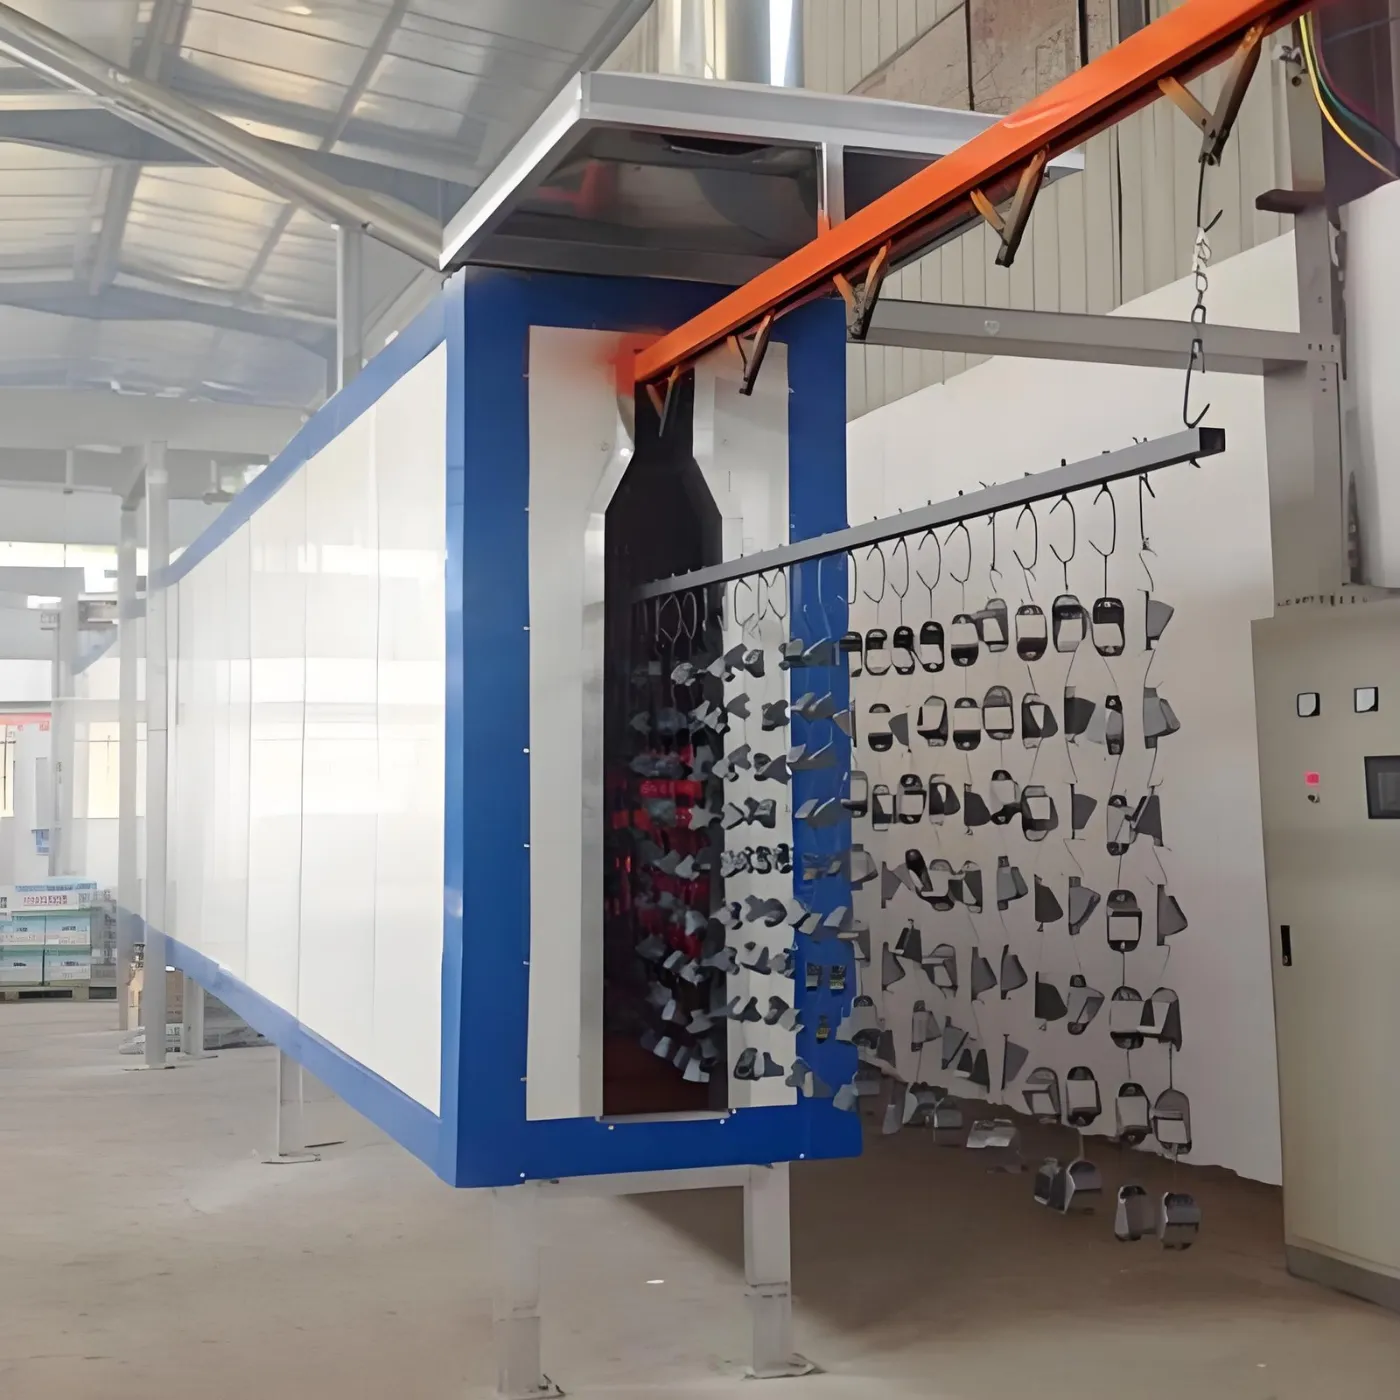
Why hardware lines are designed backwards from other lines
Most coating lines are sized from throughput. A hardware line is sized from variety. The plant coats hand tools this morning, lighting brackets this afternoon and fasteners tomorrow, in five colours, against orders that change weekly.
Under those conditions a faster conveyor buys very little. What buys capacity is cutting the time the line stands still — colour changes, rack changes and setup — and getting more parts through per metre of conveyor.
Where does a hardware line actually lose capacity?
| Loss | Typical hours lost per shift | Fix |
|---|---|---|
| Colour changeover | 1.5-4 h | Quick colour-change booth, module recovery |
| Low hanging density | Equivalent to 1-2 h | Multi-part racks, closer pitch |
| Rack changeover between part families | 0.5-1.5 h | Universal rack bodies with swappable hooks |
| Rework from film variation | 0.3-1 h | Hook cleaning discipline, earthing checks |
| Waiting for oven at line start | 0.3-0.7 h | Timer start, or IR booster zone |
Colour changeover dominates. A conventional steel booth needs 60 to 120 minutes; a purpose-built quick-change booth needs 10 to 25. At four changes a shift that is roughly 4.7 hours of production recovered per shift, which is more capacity than any realistic conveyor speed increase would deliver. The quick colour-change booth guide works through the payback maths.
How do you increase hanging density safely?
| Minimum part spacing | 150-250 mm between parts, so they do not shadow each other electrostatically. |
|---|---|
| Multi-level racks | three to six levels on one carrier for small parts, rather than one part per hook. |
| Contact point discipline | one contact point per part where possible, positioned where a witness mark is acceptable. |
| Rack mass | every kilogram of steel is heated to 200 C and cooled on every pass. Light racks cut oven fuel by 5-12 percent. |
| Hook cleaning | burn-off or chemical strip on a schedule. Powder build-up raises resistance until parts stop earthing and film goes thin. |
| Delivery record | 800+ coating lines for 500+ clients in 36 countries (MUSI engineering team, cumulative since 2011) |
| Services | Design, manufacturing, installation, commissioning, operator training and after-sales support from one company |
Density has a hard limit. Pushing past it produces thin film on facing surfaces, which shows up as a corrosion complaint months later rather than as a visible defect at the line.
What does it actually cost per part?
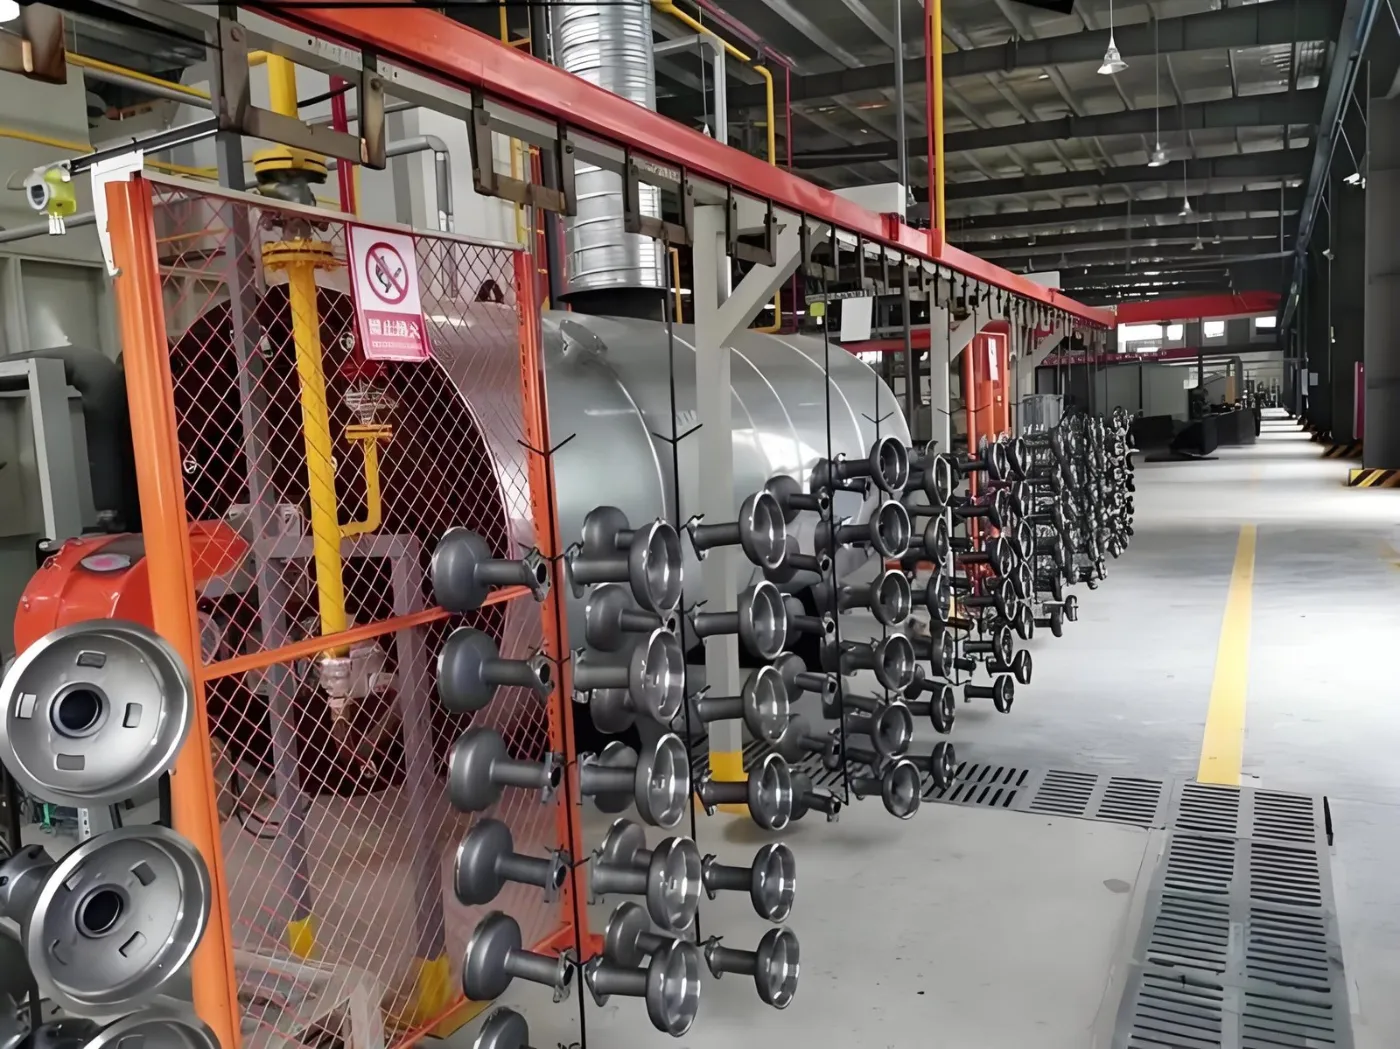
| Part example | Surface area | Powder cost | Energy | Total direct |
|---|---|---|---|---|
| Small bracket | 0.03 m2 | USD 0.04-0.11 | USD 0.02-0.06 | USD 0.06-0.17 |
| Lighting housing | 0.12 m2 | USD 0.14-0.42 | USD 0.10-0.26 | USD 0.24-0.68 |
| Hand tool body | 0.05 m2 | USD 0.06-0.18 | USD 0.05-0.11 | USD 0.11-0.29 |
| Power tool housing | 0.08 m2 | USD 0.10-0.28 | USD 0.07-0.18 | USD 0.17-0.46 |
Figures exclude labour and assume 60-80 micron film with working powder recovery. Powder and energy together are 70 to 85 percent of direct running cost, which is why recovery efficiency and oven insulation matter far more over the life of the line than the purchase price difference between two suppliers.
Which line configuration fits which plant?
| Configuration | Parts per hour | Colours | Indicative price (USD) |
|---|---|---|---|
| Manual booth plus batch oven | 80-250 | 1-2 | 25,000-60,000 |
| Semi-automatic, overhead chain, 5-stage | 250-600 | 2-4 | 120,000-260,000 |
| Automatic, quick colour change, 5-stage | 600-1,200 | 4-8 | 260,000-450,000 |
| Automatic, power-and-free, module recovery | 1,200-2,000 | 6-12 | 450,000-600,000 |
Power-and-free becomes worth its price premium when the plant runs many part families that need different oven dwell times or manual touch-up, because carriers can be buffered without stopping the line. Below that, plain overhead chain at USD 180-450 per metre is the more economical answer.
How do you coat fasteners and very small parts?
- Prepare in bulk with a tumble belt shot blast machine rather than hanging individually.
- Coat in baskets or on dense multi-level racks, accepting a witness mark at the contact point.
- Sieve reclaimed powder at 150-200 mesh; small-part work generates fines quickly and fines build thin film.
- Where volume justifies it, a dedicated small-parts line with its own recovery avoids contaminating the main line’s powder.
Working with MUSI Technology on a hardware line
MUSI Technology (Changzhou MUSI Environmental Technology Co., Ltd.) designs and builds turnkey finishing lines from its plant in Changzhou, China, with 800+ coating lines delivered to 500+ clients across 36 countries, from single booths to complete finishing plants.
- Every line is engineered against a written performance specification. Line speed, carrier pitch, colour change time and film build are stated in the contract and demonstrated on your own parts at the factory trial run before shipment.
- Rack and jig design is treated as part of the line rather than an afterthought, because hanging density and earthing decide both throughput and film consistency on hardware work.
- One engineering team owns the whole chain — pretreatment, application, recovery, curing, conveying and dust collection — so the trade-offs between them are settled on the drawing board, not on your factory floor.
Send your part list, colour schedule and target parts per hour for a line layout and a cost-per-part estimate: contact MUSI Technology. See also metal hardware coating solutions and the quick colour-change powder booth.
Frequently asked questions
What kind of coating line suits small metal hardware?
An overhead chain line with dense multi-level racking and a quick colour-change powder booth. Hardware plants run many short jobs, so changeover time governs capacity more than conveyor speed: a booth that switches colour in 10-25 minutes instead of 60-120 recovers roughly 4.7 hours per shift at four changes, which exceeds what any realistic speed increase would give.
How much does it cost to powder coat a hardware part?
Direct cost is roughly USD 0.06-0.17 for a small bracket of 0.03 m2, USD 0.11-0.29 for a hand tool body, USD 0.17-0.46 for a power tool housing, and USD 0.24-0.68 for a lighting housing, at 60-80 micron film with working powder recovery and excluding labour. Powder and energy together account for 70-85 percent of that.
How close together can parts be hung on the conveyor?
Keep 150-250 mm between parts. Closer than that and parts shadow each other electrostatically, producing thin film on facing surfaces. That failure is invisible at the line and surfaces months later as a corrosion complaint, so hanging density has to be verified with film measurements rather than pushed until something looks wrong.
How many colours can one hardware line run?
With a quick colour-change booth, cartridge module recovery and colour-dedicated hoppers, six to twelve colours on one line is routine. Above about three colour changes per shift a quick-change booth typically pays back its USD 15,000-70,000 price premium within the first year in recovered production time.
How are fasteners and very small parts coated?
In bulk rather than individually: prepared in a tumble belt shot blast machine, then coated in baskets or on dense multi-level racks with a witness mark accepted at the contact point. Reclaimed powder must be sieved at 150-200 mesh, because small-part work generates fines quickly and a high fines fraction builds thin, uneven film.
What does a metal hardware coating line cost?
Indicative 2026 ex-works ranges are USD 25,000-60,000 for a manual booth with batch oven at 80-250 parts per hour, USD 120,000-260,000 for a semi-automatic overhead chain line at 250-600 parts per hour, USD 260,000-450,000 for an automatic line with quick colour change at 600-1,200 parts per hour, and USD 450,000-600,000 for a power-and-free line at 1,200-2,000 parts per hour.
About the figures in this guide. Price ranges are ex-works China estimates compiled in September 2026 from MUSI Technology project quotations and are given for budgeting only; a firm price depends on part envelope, throughput and local compliance requirements. Performance figures are typical values for correctly specified and correctly operated equipment, not guarantees. Last reviewed: 10 September 2026.
Send us your part size, throughput and coating type — our engineers reply within 24 hours, and a layout and budget follow once your part data is complete. Contact MUSI Technology or browse our equipment range.
Further Reading
- ProductsHardware Coating Line
Quick Color-Change Booth - IndustryMetal Hardware Coating
- Technical guidesQuick Colour-Change Powder Booth: How to Cut Changeover to 15 Minutes (2026)
- Case StudiesHardware Robotic Flexible Coating Line
Lighting Hardware Powder Coating Line
Power Tool Housing Coating Solution
QQuestions buyers ask before ordering
quotation · price · lead time · installation · warranty
What information do you need to prepare a quotation?
Send part drawings or photos, the largest part size and weight, the material, the required output per shift, the paint or powder type and number of colours, and the available floor space, ceiling height and power or gas supply. MUSI engineers reply within 24 hours; a recommended configuration and quotation follow once your part data is complete.
How much does this equipment cost?
Budget depends on part size, throughput and the level of automation. Indicative ex-works ranges are published in our complete coating line cost guide; a configured quotation is prepared from your part data. Published indicative ex-works ranges: a complete powder coating line is roughly USD 75,000–230,000 semi-automatic, USD 200,000–600,000 for a standard automatic line and USD 600,000–2,000,000 for a high-throughput automated plant.
What is the lead time?
Standard configurations ship in 30–60 days from contract signing and down payment; custom configurations take longer. The delivery date is fixed in the contract.
Do you install and train operators overseas?
Yes. MUSI engineers carry out on-site installation and commissioning and give 3–5 days of operator and maintenance training. MUSI has delivered 800+ coating lines to customers in 36 countries.
What warranty and after-sales support are included?
12 months full-machine warranty, 36 months on critical components and up to 60 months on structural parts. International customers get 24-hour phone response and 72-hour on-site arrival; spare parts ship from the Changzhou headquarters.
Can the environmental equipment be supplied with the line?
Yes. VOC treatment (RTO, RCO, activated carbon, zeolite rotor), dust collection and paint wastewater treatment are supplied with the coating line under one contract; MUSI has equipped 50+ coating facilities whose projects all passed local environmental compliance reviews.