Case Study: Aluminium Profile Powder Coating Line, Indonesia
Summary
A complete electrostatic powder coating line, about 108 tonnes of equipment, for an aluminium extrusion and fenestration company headquartered in Jakarta that runs five extrusion presses with a stated capacity of 1,000 tonnes of profile a month and finishes its own profiles by anodizing, powder coating and wood-grain. Pretreatment, powder booths with automatic reciprocators, cyclone recovery, curing and a conveyor for long profiles were engineered as one package, shipped from China in June 2026 with a spare-parts package following in August 2026.
Project Background
The client is one of Indonesia’s aluminium extrusion manufacturers and a facade, door and window specialist, headquartered in Jakarta. It runs five extrusion presses (four 1,000 MT and one 3,500 MT) with a stated capacity of 1,000 MT of profiles per month, and finishes its own profiles by anodizing, powder coating and wood-grain finishing. MUSI supplied a complete electrostatic powder coating line, shipped from China in June 2026, followed by spare parts in August 2026.
The Challenge
Architectural profiles are long, slim and exposed on every face once installed in a window, door or curtain wall. The coating has to be even along the full length and around every edge and groove, colour has to match from batch to batch across a whole building, and the line has to keep pace with an extrusion plant working at around a thousand tonnes a month.
MUSI's Solution
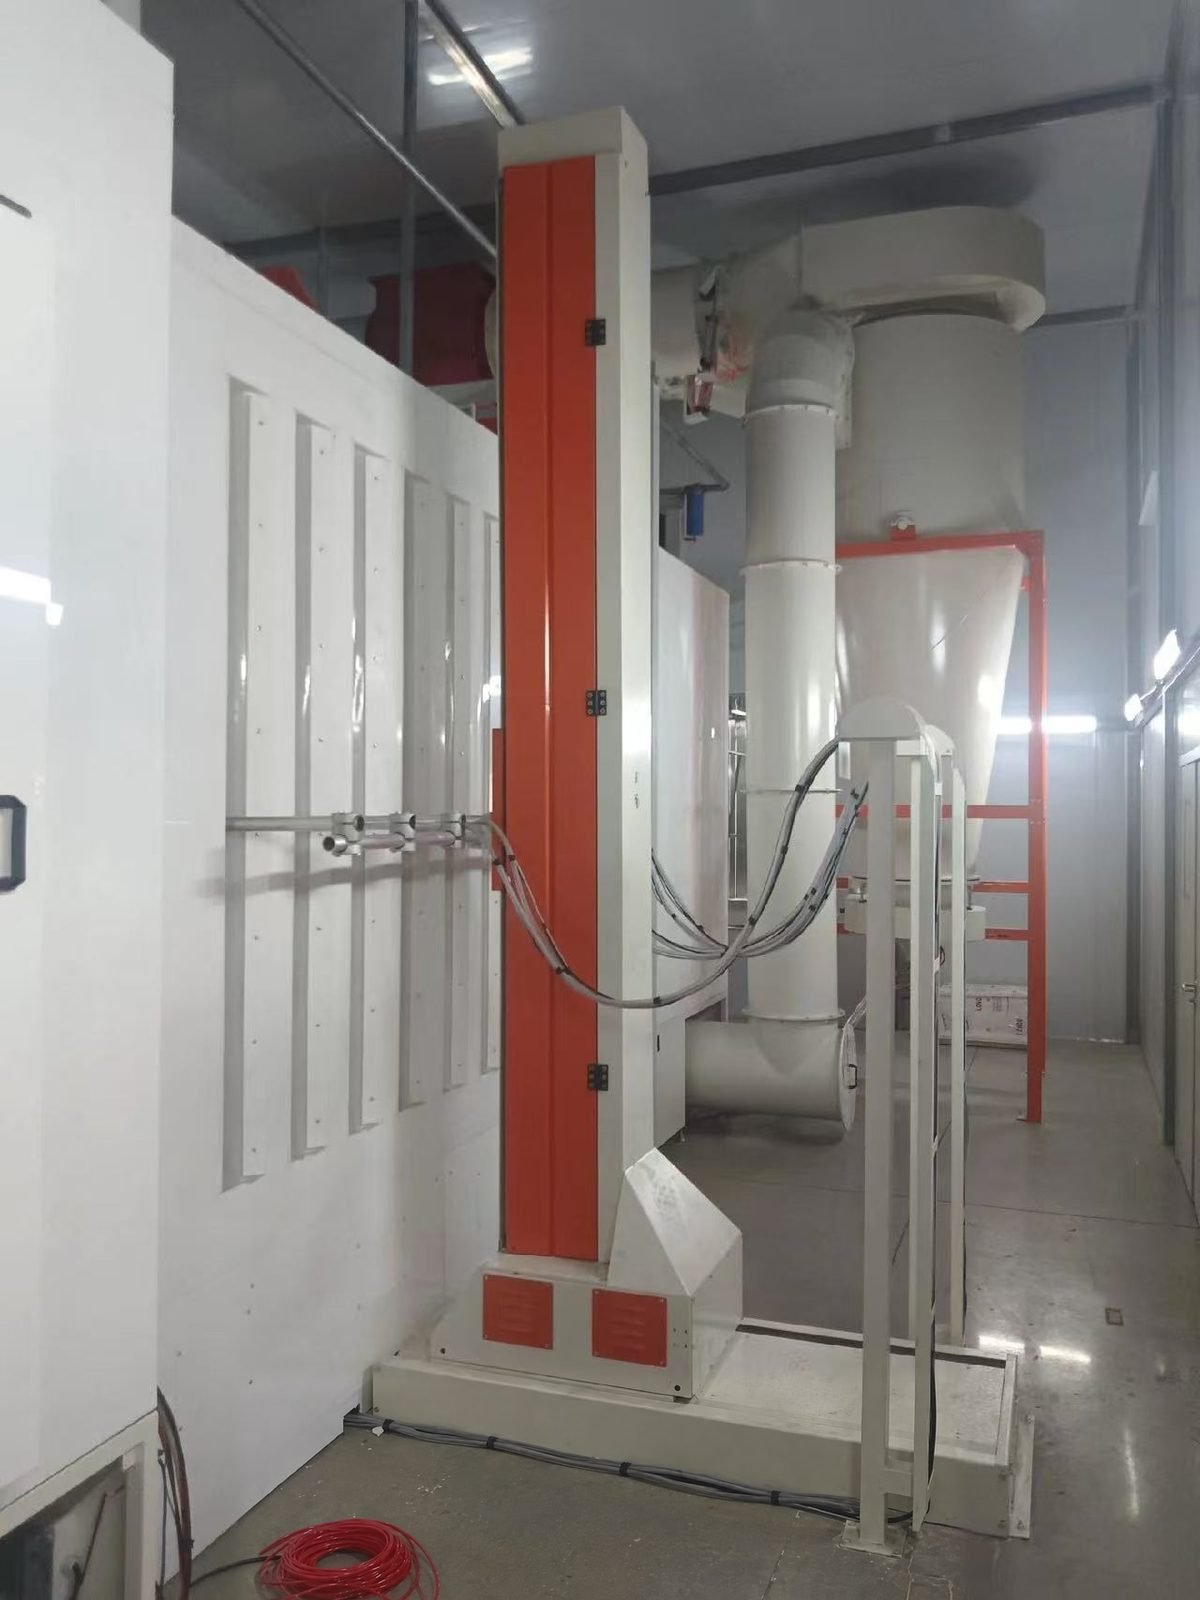
MUSI supplied the line as one complete package — around 108 tonnes of equipment shipped as a single project — so pretreatment, powder application, recovery, curing and conveying were engineered to work together rather than sourced piece by piece. Electrostatic powder booths with automatic reciprocators apply the powder along the profile length, cyclone recovery returns overspray for reuse, and the curing oven is matched to the line speed. A follow-up shipment of spare parts keeps wear items on hand at the plant.
Equipment Scope
- Complete electrostatic powder coating production line with accessories
- Powder booths with automatic reciprocators
- Cyclone powder recovery
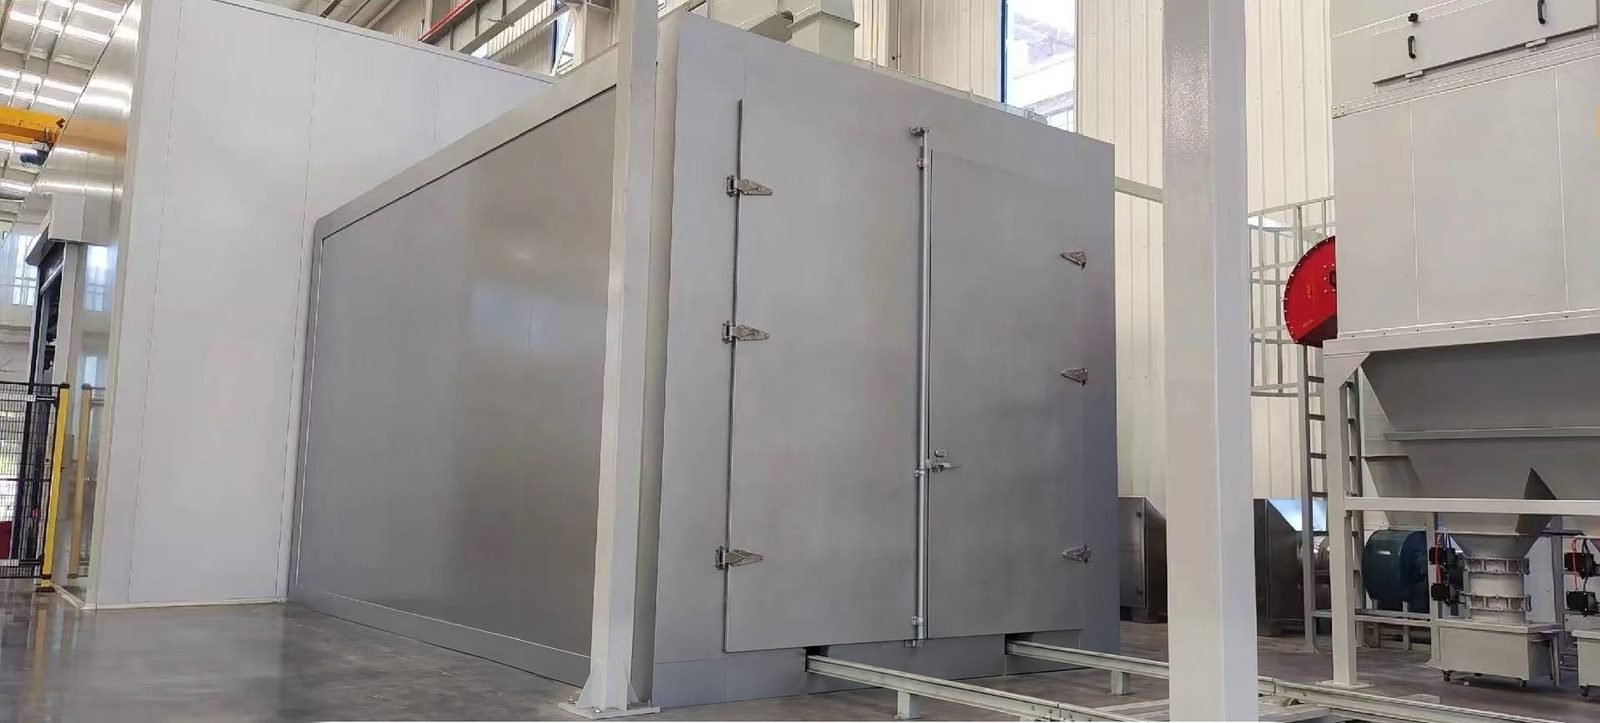
- Pretreatment and curing sections matched to line speed
- Conveyor for long aluminium profiles
- Spare parts package for wear items
Results
The complete line reached the client in June 2026, with spare parts following in August, adding MUSI powder coating capacity to one of Indonesia’s established aluminium extrusion and fenestration producers.
Selection logic: why this configuration
A complete package from one supplier was chosen over sourcing booth, oven and conveyor separately so that line speed, oven length and reciprocator stroke were matched at design rather than on site. Automatic reciprocators with cyclone recovery were specified because architectural profiles need even film along the full length and the plant runs a limited colour palette at high volume. A spare-parts shipment was added so wear items are on hand at the plant.
Scope of supply and key components
| Item | Specification | Notes |
|---|---|---|
| Complete powder coating line | About 108 t of equipment with accessories | Shipped June 2026 |
| Powder booths | Automatic reciprocators | |
| Powder recovery | Cyclone | |
| Pretreatment and curing | Matched to line speed | |
| Conveyor | For long aluminium profiles | |
| Spare parts | Wear-item package | Shipped August 2026 |
Key components
Key components are available from international brands, configurable per customer specification, so that spare parts can be sourced locally over the life of the line. Brand names below are the usual options for this type of equipment; the brands actually fitted are fixed in the contract specification.
| Component | Brands available on request |
|---|---|
| Automatic powder guns and powder feed | Gema OptiGun, Nordson Encore, WAGNER PEA-X1, Sames (formerly SAMES KREMLIN) |
| Oven and dryer gas burners | Riello RS series, Weishaupt monarch WM-G, Baltur TBG, Honeywell Maxon OVENPAK, Eclipse |
| PLC and HMI | Siemens SIMATIC S7-1500, Mitsubishi Electric MELSEC iQ-R, Schneider Electric Modicon, OMRON NX, Rockwell Automation Allen-Bradley |
| Variable-frequency drives | ABB ACS580, Siemens SINAMICS G120, Danfoss VLT, Schneider Electric Altivar, Yaskawa, Mitsubishi Electric |
| Conveyor gear motors | SEW-EURODRIVE, NORD DRIVESYSTEMS, Bonfiglioli, Siemens, Sumitomo Drive Technologies |
| Pretreatment pumps and chemistry | Grundfos CR, KSB Etanorm, Xylem; Henkel BONDERITE, Chemetall Gardobond, PPG Zircobond, Nippon Paint |
| Dust collector filter cartridges | Donaldson Ultra-Web, Parker BHA, Camfil, MANN+HUMMEL |
| Compressed air for powder feed and instruments | Atlas Copco GA, Ingersoll Rand RS, KAESER ASD, Sullair |
Not included in the scope of supply
- Civil works, foundations and pits
- Building services up to the battery limit: power supply, gas, compressed air, water and drainage
- Local permits, emission approvals and third-party inspections
- Paint or powder supply, unless stated in the contract
- Installation labour and site utilities at the Jakarta plant
Services included with every line: engineering design, manufacturing, shipping documentation, installation supervision, commissioning, operator training, warranty and spare parts.
Typical programme
The durations below are typical for equipment of this class and are given for planning; they are not the recorded schedule of this project. A complete line usually runs 90–180 days from contract to acceptance, a single unit 30–60 days.
| Stage | Typical duration | What happens |
|---|---|---|
| Site survey and workpiece review | 5–10 days | Remote review of drawings and photos, or an engineer visit |
| Layout and detail design | 15–30 days | Layout drawing, utilities list and specification sign-off |
| Manufacturing | 45–90 days | Booths, ovens, conveyor, pretreatment and controls built and pre-assembled at the works |
| Shipping | 20–45 days | Sea freight; equipment shipped in sections for on-site assembly |
| Installation | 15–40 days | MUSI supervision with the client's installation crew or MUSI crew |
| Commissioning, training and acceptance | 7–15 days | Trial runs on the client's parts, operator training, acceptance record |
Applicability and limits
Line capacity is matched to the client's extrusion output and profile range; wider or heavier sections change hanging density and oven length. Shipment dates come from the shipping records, and production figures at the plant have not been published.
Results shown in this case study reflect the stated operating conditions and should not be interpreted as guaranteed performance under different feed, production, environmental, or site conditions.
After-sales and spare parts
Warranty on a MUSI coating line runs from acceptance: 12 months on the complete line excluding consumables, 36 months on critical components such as motors, drives and the PLC, and 60 months on structural parts such as steel structure, ducting and oven bodies. Failures within warranty, excluding misuse, are repaired free of charge.
Support starts remotely: the service line is staffed around the clock, a preliminary diagnosis with recommendations is given within 2 hours, and where a site visit is needed an engineer reaches any major city within 72 hours. A spare-parts inventory is held at the Changzhou headquarters with same-day shipping, and customers can keep a dedicated parts stock at MUSI for emergencies. Details are on the after-sales service page.
FAQ
What does a complete aluminium profile powder line include? Pretreatment, a conveyor for long profiles, powder booths with reciprocators, cyclone recovery and a curing oven, all sized to one line speed, plus accessories and spare parts.
Vertical or horizontal for this plant? The line was engineered to the client's hall and profile range; the general comparison of the two layouts is in the aluminium profile coating guide linked below.
Why order spare parts with the line? So that wear items such as gun parts, filters and hooks are on hand when the line starts, instead of waiting for a shipment during production.
How was the line shipped? As one project of about 108 tonnes in June 2026, followed by a spare-parts consignment in August 2026.
What pretreatment do architectural profiles need? A multi-stage spray tunnel with a chromate-free conversion coating, matched to the architectural powder specification and the plant's water conditions.
Next step: a configuration proposal for a similar line
If your parts, volumes or plant conditions are close to this project, MUSI can return a line configuration and layout proposal. To prepare it we need four things:
- Photos and dimensions of the workpieces, with weight and material
- Required output (pieces per hour or per day, and shifts)
- Number of colours and how often colour changes are needed
- Available floor space and ceiling height, with the utilities on site
Message us on WhatsApp with these details, or use the quotation form.
Published 2026-09-26 · Updated 2026-09-30 · Last technical review: 2026-09-30
Get a Similar Solution
If your industry and requirements match this case, contact MUSI to schedule a free consultation. We'll design an optimal solution based on your specific workpieces, capacity, and facility.
Provided by Lin Cong, Technical Director, MUSI Technology