Energy-Storage Cabinet Coating Lines in Southeast Asia: Controlling Humidity, Flash Rust and Cure
Quick answer: In Vietnam, Thailand, Malaysia and Indonesia, humidity is the paint shop’s main enemy. Wet air causes flash rust between pretreatment and painting, condensation on cold steel, blushing in solvent paints and slow flash-off in waterborne ones. A cabinet line for the region needs a dry-off oven, conditioned booth air and a short, closed path from pretreatment to the first coat.
How humidity shows up as defects
| Flash rust | freshly cleaned steel oxidises within hours in tropical air. Pretreatment should be followed immediately by a dry-off oven and then primer. |
|---|---|
| Condensation | steel colder than the dew point collects moisture. A common rule is to keep the steel surface at least 3 °C above the dew point during painting. |
| Slow flash-off | waterborne paints dry slowly in humid air, so a heated flash-off zone before the oven keeps takt time stable. |
Pretreatment for the tropics
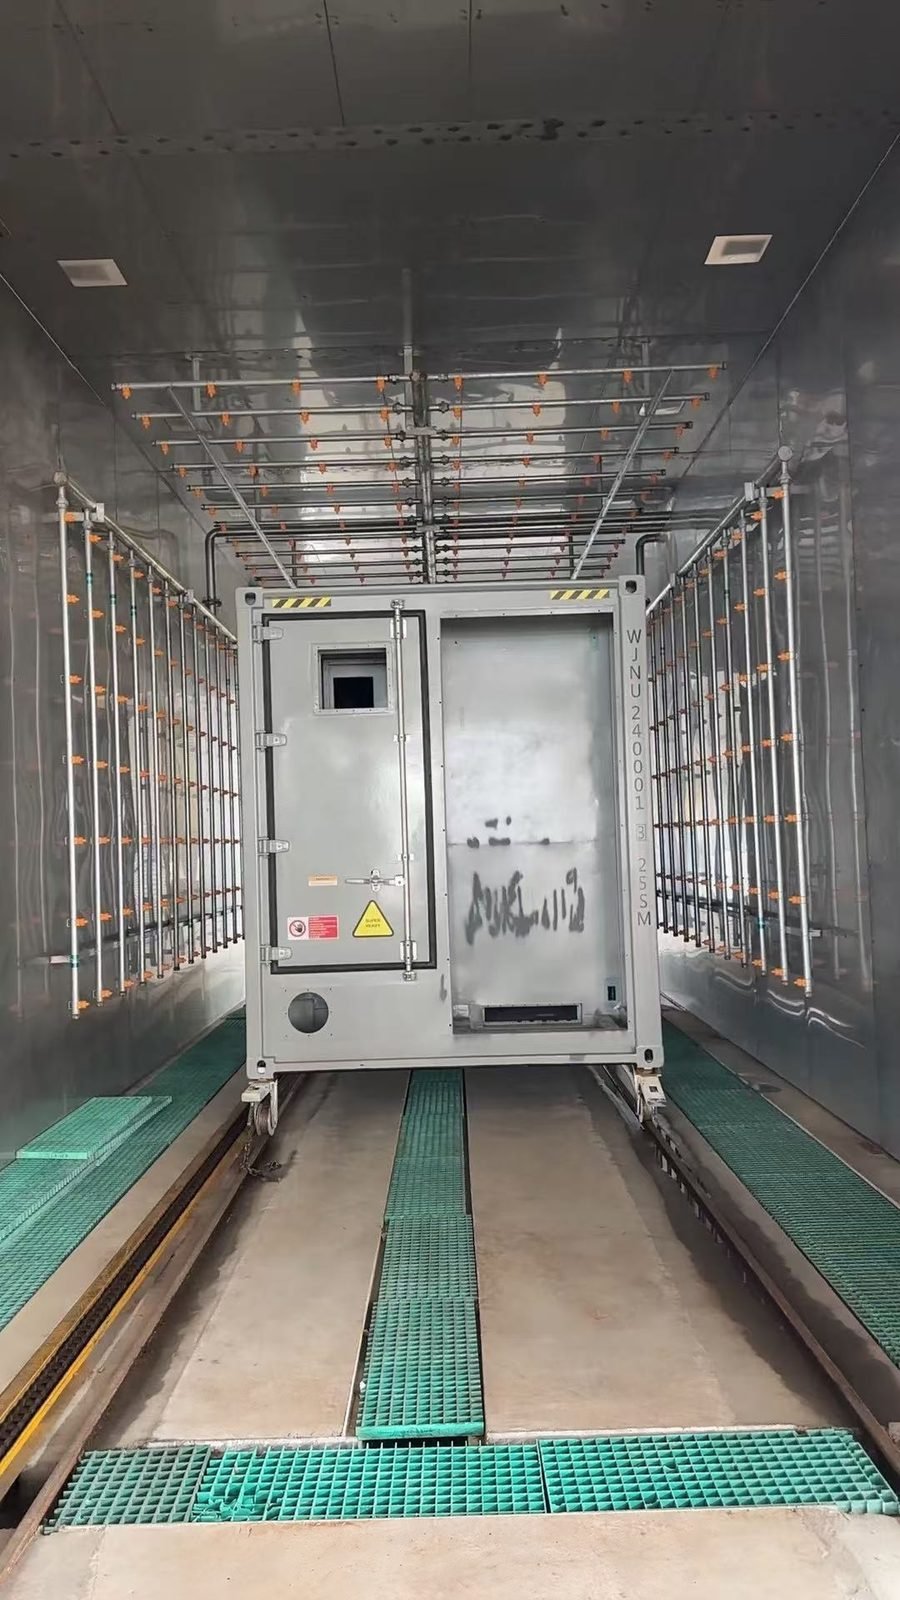
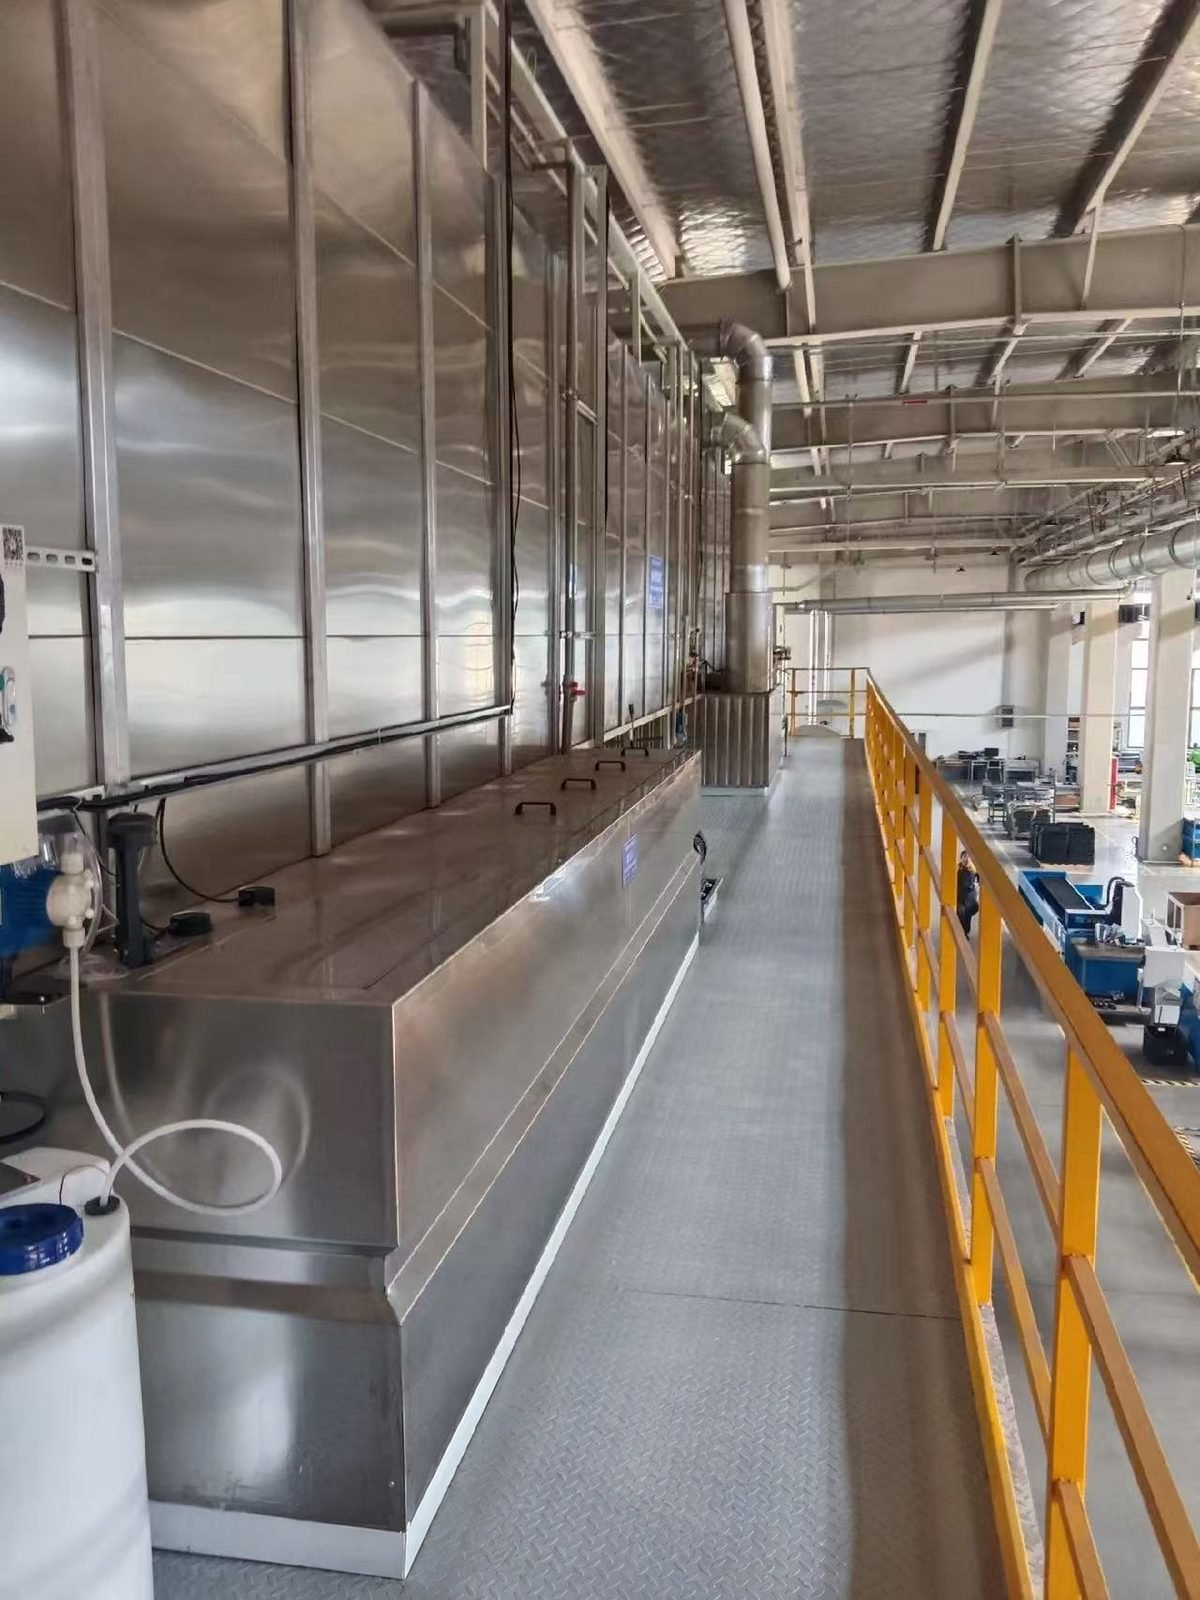
Multi-stage spray or dip pretreatment with good rinse water control gives a clean, conversion-coated surface. Chemical dosing should be automatic, because bath concentrations drift faster at high temperatures. Monsoon rain also makes a rain test at the end of the line especially useful: it catches gasket and seam leaks before cabinets ship.
Reference line configuration
For reference, a current 20-ft energy-storage box line design handles boxes of 6,058 × 2,438 × 2,591 mm up to 2,500 kg on a box-pulling chain, with automatic blasting, primer, intermediate and topcoat booths of 10 × 6.6 × 5.2 m, paint drying at 80–120 °C, powder curing at 200–220 °C, a rain test chamber and 160,000 m³/h of VOC treatment. The full table is on our container line case; MUSI’s fastest energy-storage box lines release one finished box per minute.
FAQ
Do we need air conditioning for the whole booth? Not always. Conditioning the booth supply air and keeping booths closed with fast-acting doors is usually enough.
Powder or liquid? Powder avoids solvent blushing and flash-off issues entirely and suits cabinets well; liquid gives more flexibility on film build and colour.
Where MUSI Technology fits
MUSI has supplied coating lines in Indonesia and Vietnam and builds complete cabinet lines with pretreatment, dry-off, booths, ovens and rain testing. Send cabinet size and output for a layout.
Provided by Lin Cong, Technical Director, MUSI Technology
Send us your part size, throughput and coating type — our engineers reply with a layout and budget within one working day. Contact MUSI Technology or browse our equipment range.
Further Reading
- ProductsEnergy Storage Container Coating Line
- IndustryEnergy Storage Container Coating
- Technical guidesEnergy Storage Container Coating Line: Corrosion Spec and Layout (2026)
Energy-Storage Container Coating Line for the Middle East: Designing for Heat, Sand and UV
Energy-Storage Box Painting Lines for Europe: Meeting VOC Limits Without Losing Throughput
Coating Energy-Storage Enclosures for Coastal and Offshore Sites: Designing for ISO 12944 C5 and CX
Energy-Storage Container Painting Lines for North America: Air Permits, Booth Safety and High Throughput
Energy-Storage Box Coating Lines for Africa: Compact Lines for Local Assembly
Energy-Storage Box Painting Lines for Latin America: Desert Sun, Altitude and Local Content
Energy-Storage Box Coating Lines for India: Scaling Local BESS Enclosure Production
Coating Energy-Storage Cabinets for Cold Climates: Nordic, Canadian and Central Asian Plants - Case StudiesEnergy-Storage Cabinet Spray Coating Line, Jiangsu
Energy-Storage Enclosure Painting Line for a Global Battery Maker
Energy-Storage Cabinet & Container Painting Line, Jiangyin