Energy Storage Container Coating Line: Corrosion Spec and Layout (2026)
Quick answer: A battery energy storage (BESS) container coating line must reach ISO 12944 corrosivity class C4 or C5 (ISO 12944:1998: C5-M), which typically means blasting to Sa2.5, a zinc-rich epoxy primer at 60-80 microns, an epoxy micaceous iron oxide intermediate coat for C4 and C5 systems, and a polyester or polyurethane topcoat at 60-80 microns, for a total dry film of 160-240 microns (C4) or 240-320 microns (C5); a two-coat 120-160 micron system covers C3 only. A dedicated line for 20 ft and 40 ft enclosures costs roughly USD 400,000-1,500,000.
Related equipment and projects: Energy Storage Container Coating Line · Energy-Storage Enclosure Painting Line for a Global Battery Maker · Energy-Storage Cabinet & Container Painting Line, Jiangyin
Why does BESS enclosure coating have a tougher specification than general steelwork?
Storage containers sit outdoors, unattended, for a design life of 15-25 years, frequently in coastal or industrial atmospheres. Repainting in service is expensive and often contractually excluded, so the coating system has to survive the whole warranty period first time.
Three specific stresses drive the specification: salt and humidity at the site, thermal cycling from the battery cooling system, and condensation on the inner shell. The interior needs its own system, not just an exterior finish.
What corrosion class and film build do you need?
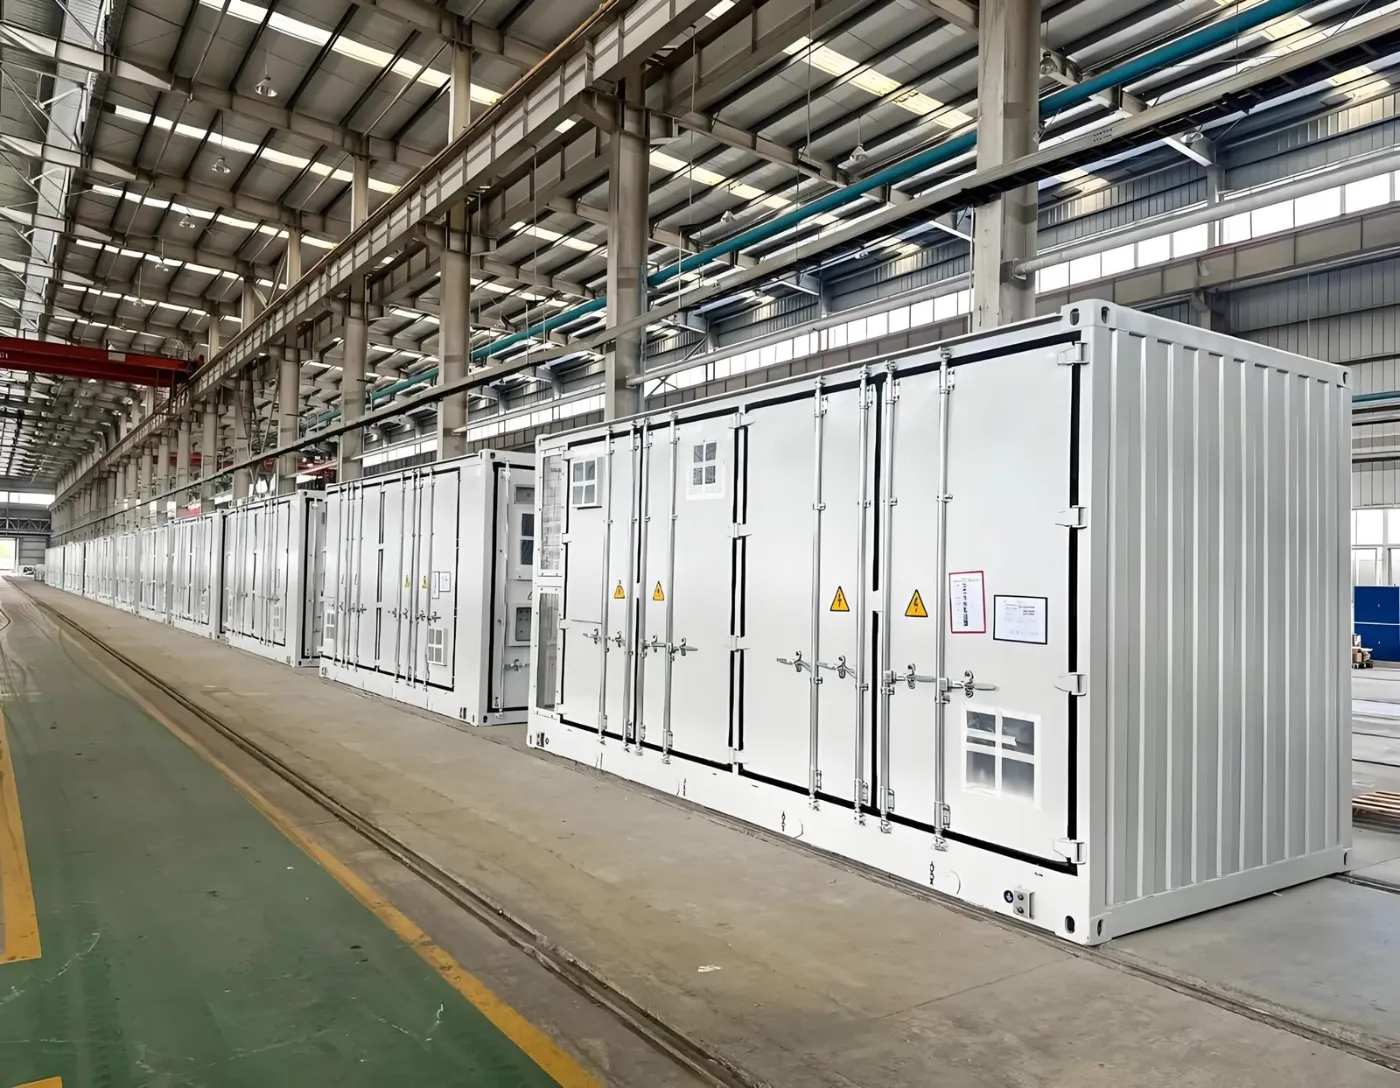
Specifications reference ISO 12944 corrosivity categories. C4 covers industrial and coastal inland; C5 covers marine and high-salinity coastal.
| Environment | ISO 12944 class | Typical system | Total DFT | Design life |
|---|---|---|---|---|
| Inland, low pollution | C3 | Epoxy primer + polyester topcoat | 120-160 microns | 15+ years |
| Industrial or coastal inland | C4 | Zinc-rich epoxy + epoxy MIO + PU topcoat | 160-240 microns | 15-25 years |
| Marine, high salinity | C5 | Zinc-rich epoxy + epoxy MIO + PU topcoat | 240-320 microns | 15-25 years |
Powder-only systems are used on smaller enclosures and battery pack housings but are less common on full containers, where the part size exceeds most oven envelopes and multi-coat liquid systems dominate.
What does the line have to include?
- Shot blasting to Sa2.5 with a 40-75 micron profile. On full containers this means a blast room rather than a wheel machine.
- Blast media recovery and dust collection sized for the room cross-section.
- Priming booth with controlled temperature and humidity for zinc-rich epoxy.
- Flash-off zone sized to the solvent system, typically 10-20 minutes.
- Topcoat booth, often airless or electrostatic to control overspray on large flat panels.
- Drying or forced-cure oven at 60-80 C for liquid systems.
- VOC exhaust treatment where solvent-borne coatings are used.
How big does the equipment have to be?
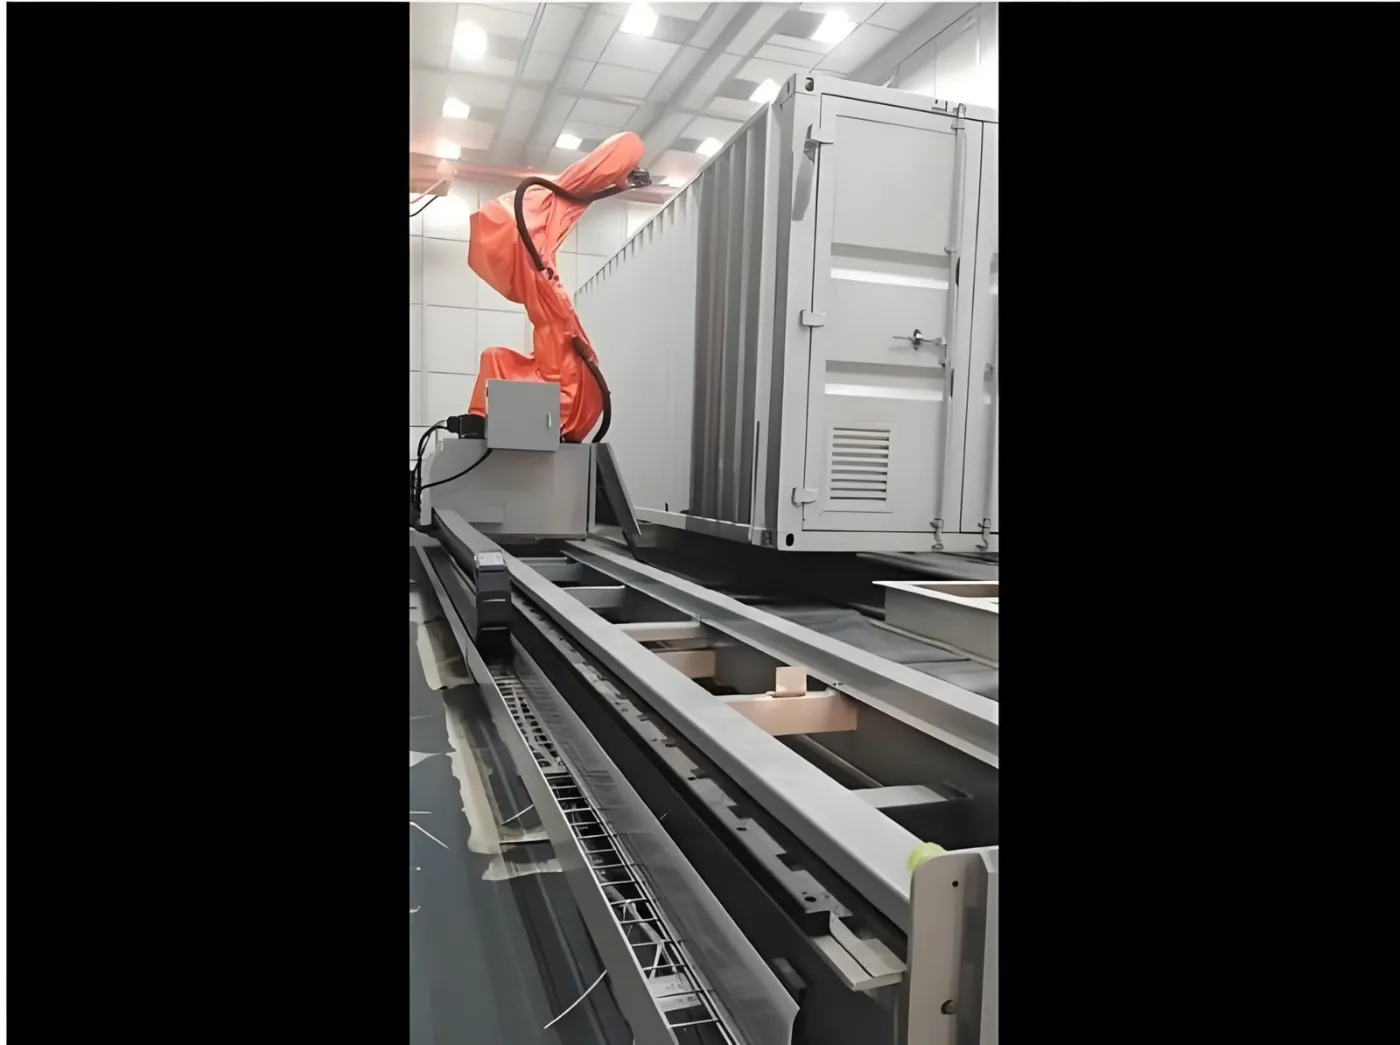
| Enclosure | Blast room / booth internal size | Typical airflow per booth |
|---|---|---|
| 20 ft container | 9 x 4.5 x 4.5 m | 30,000-45,000 m3/h |
| 40 ft container | 15 x 4.5 x 4.5 m | 45,000-70,000 m3/h |
| Battery pack housing | 3 x 2 x 2 m | 8,000-15,000 m3/h |
Airflow follows the standard cross-draft rule of 0.4-0.6 m/s across the booth cross-section. Under-sizing extraction on a 40 ft booth is the most common cause of overspray settling on the wet film. These figures are design ranges: extraction airflow = effective booth cross-section (internal width x height for a cross-draft booth) x 0.4-0.6 m/s face velocity, measured in the empty booth at the working cross-section, plus a margin for filter loading; the final value is fixed in the line layout and verified at commissioning by velocity measurement across that cross-section.
How much does a BESS container coating line cost in 2026?
| Scope | Indicative price (USD, ex-works) |
|---|---|
| Blast room for 40 ft container, with recovery | 120,000-350,000 |
| Combined spray and drying booth, 40 ft | 90,000-280,000 |
| Dust collection for blast room | 35,000-120,000 |
| VOC treatment (RTO or carbon) | 60,000-350,000 |
| Transfer system and rails | 30,000-120,000 |
| Typical complete line | 400,000-1,500,000 |
What are the common quality failures?
| Rust bleeding at welds within 2-3 years | welds not ground and re-blasted before priming. |
|---|---|
| Zinc primer under-cured before topcoat | insufficient flash-off, trapping solvent and causing blistering. |
| Condensation corrosion inside the enclosure | interior treated as cosmetic. Specify the same primer inside. |
| Film build below specification at edges | stripe-coat all edges and corners by hand before the main coat. |
| Salt contamination before priming | test surface salts after blasting on coastal sites; wash and re-blast if above the specified limit. |
| Delivery record | 800+ coating lines for 500+ clients in 36 countries (MUSI engineering team, cumulative since 2011) |
| Services | Design, manufacturing, installation, commissioning, operator training and after-sales support from one company |
Why source a BESS coating line from MUSI Technology?
MUSI Technology (Changzhou MUSI Environmental Technology Co., Ltd.) is a China-based manufacturer of turnkey coating lines and environmental equipment, with 800+ coating lines delivered to 500+ clients across 36 countries, including energy storage container and battery housing coating plants.
- Blast rooms, spray booths and drying ovens sized to 20 ft and 40 ft enclosures.
- Matched dust collection and VOC treatment supplied as part of the same line.
- Standard configurations ship in 30-60 days with a 12-month full-machine and 36-month critical-component warranty. Structural parts are covered for up to 60 months.
- Every line is engineered against a written performance specification. Line speed, cure profile, film build and emission level are stated in the contract and demonstrated on your own part at the factory trial run before shipment.
- One engineering team owns the whole chain — pretreatment, application, curing, conveying and emission control — so the trade-offs between them are settled on the drawing board, not on your factory floor.
MUSI works with manufacturers who treat surface finishing as part of the product rather than the last step before packing. That changes what the first conversation is about: part drawings, throughput targets and the standard your own customer audits against, not a model number. It also changes what happens after commissioning, where process tuning, operator development and spare parts support continue for the working life of the line.
See the energy storage container coating solutions or the blasting equipment range.
Frequently asked questions
What corrosion class does a battery energy storage container need?
ISO 12944 class C4 for industrial and coastal inland sites, or C5 for marine and high-salinity coastal locations. C4 systems typically run 160-240 microns total dry film thickness and C5 systems 240-320 microns, both designed for a 15-25 year life to first major maintenance.
What coating system is used on BESS enclosures?
The usual system is shot blasting to Sa2.5, a zinc-rich epoxy primer at 60-80 microns, an epoxy micaceous iron oxide intermediate coat for C4 and C5 systems (160-240 and 240-320 microns total dry film), and a polyurethane or polyester topcoat at 60-80 microns. The interior needs the same primer, because condensation from the cooling system attacks unprotected inner surfaces.
How big does the blasting and coating booth need to be?
For a 40 ft container, roughly 15 x 4.5 x 4.5 m internal, with 45,000-70,000 m3/h extraction to hold a 0.4-0.6 m/s cross-draft. A 20 ft container needs about 9 x 4.5 x 4.5 m and 30,000-45,000 m3/h. Battery pack housings are handled in much smaller booths at 8,000-15,000 m3/h.
Can BESS containers be powder coated?
Full containers usually cannot, because the part exceeds typical curing oven envelopes and multi-coat liquid systems are needed to reach C5 film builds. Powder is common on smaller battery pack housings and internal enclosures, where a single 60-100 micron polyester coat over a properly pretreated surface is sufficient.
What does an energy storage container coating line cost?
Indicative 2026 ex-works ranges are USD 120,000-350,000 for a 40 ft blast room with media recovery, USD 90,000-280,000 for a combined spray and drying booth, USD 35,000-120,000 for dust collection and USD 60,000-350,000 for VOC treatment. A complete line typically falls between USD 400,000 and USD 1,500,000.
Why do BESS enclosures rust at the welds first?
Because weld spatter and slag are not ground flat and re-blasted before priming. Rough weld profiles leave film thickness far below specification at the peaks, so corrosion starts there within 2-3 years. Grinding welds smooth and stripe-coating all edges by hand before the main coat is the standard fix.
About the figures in this guide. Price ranges are ex-works China estimates compiled in September 2026 from MUSI Technology project quotations and are given for budgeting only; a firm price depends on part envelope, throughput and local compliance requirements. Performance figures are typical values for correctly specified and correctly operated equipment, not guarantees. Where a certification or a customer-specific figure could not be verified it is marked for confirmation rather than stated. Last reviewed: 9 September 2026.
Send us your part size, throughput and coating type — our engineers reply within 24 hours, and a layout and budget follow once your part data is complete. Contact MUSI Technology or browse our equipment range.
Further Reading
- ProductsEnergy Storage Container Coating Line
- IndustryEnergy Storage Container Coating
- Technical guidesEV Battery Pack Housing Coating Line: Powder vs Liquid, Specs and Cost (2026)
- Case StudiesEV Battery Pack Housing Coating Line
- NewsPowder Coating in the EV Industry: Growth and Outlook
QQuestions buyers ask before ordering
quotation · price · lead time · installation · warranty
What information do you need to prepare a quotation?
Send part drawings or photos, the largest part size and weight, the material, the required output per shift, the paint or powder type and number of colours, and the available floor space, ceiling height and power or gas supply. MUSI engineers reply within 24 hours; a recommended configuration and quotation follow once your part data is complete.
How much does this equipment cost?
Budget depends on part size, throughput and the level of automation. Indicative ex-works ranges are published in our complete coating line cost guide; a configured quotation is prepared from your part data. Published indicative ex-works ranges: a complete powder coating line is roughly USD 75,000–230,000 semi-automatic, USD 200,000–600,000 for a standard automatic line and USD 600,000–2,000,000 for a high-throughput automated plant.
What is the lead time?
Standard configurations ship in 30–60 days from contract signing and down payment; custom configurations take longer. The delivery date is fixed in the contract.
Do you install and train operators overseas?
Yes. MUSI engineers carry out on-site installation and commissioning and give 3–5 days of operator and maintenance training. MUSI has delivered 800+ coating lines to customers in 36 countries.
What warranty and after-sales support are included?
12 months full-machine warranty, 36 months on critical components and up to 60 months on structural parts. International customers get 24-hour phone response and 72-hour on-site arrival; spare parts ship from the Changzhou headquarters.
Can the environmental equipment be supplied with the line?
Yes. VOC treatment (RTO, RCO, activated carbon, zeolite rotor), dust collection and paint wastewater treatment are supplied with the coating line under one contract; MUSI has equipped 50+ coating facilities whose projects all passed local environmental compliance reviews.
References and further reading
Standards and manufacturer guides behind the figures in this article:
- ISO 12944-2:2017 Corrosion protection of steel structures by protective paint systems, Part 2: Classification of environments | ISO
- ISO 12944-5:2019 Corrosion protection of steel structures by protective paint systems, Part 5: Protective paint systems | ISO
- ISO 8501-1:2007 Preparation of steel substrates, Part 1: Rust grades and preparation grades | ISO
- ISO 12944: guide to the 2018 revision | AkzoNobel International
- How to select the right paint system: Guidelines for corrosion protection in accordance with ISO 12944 | Hempel