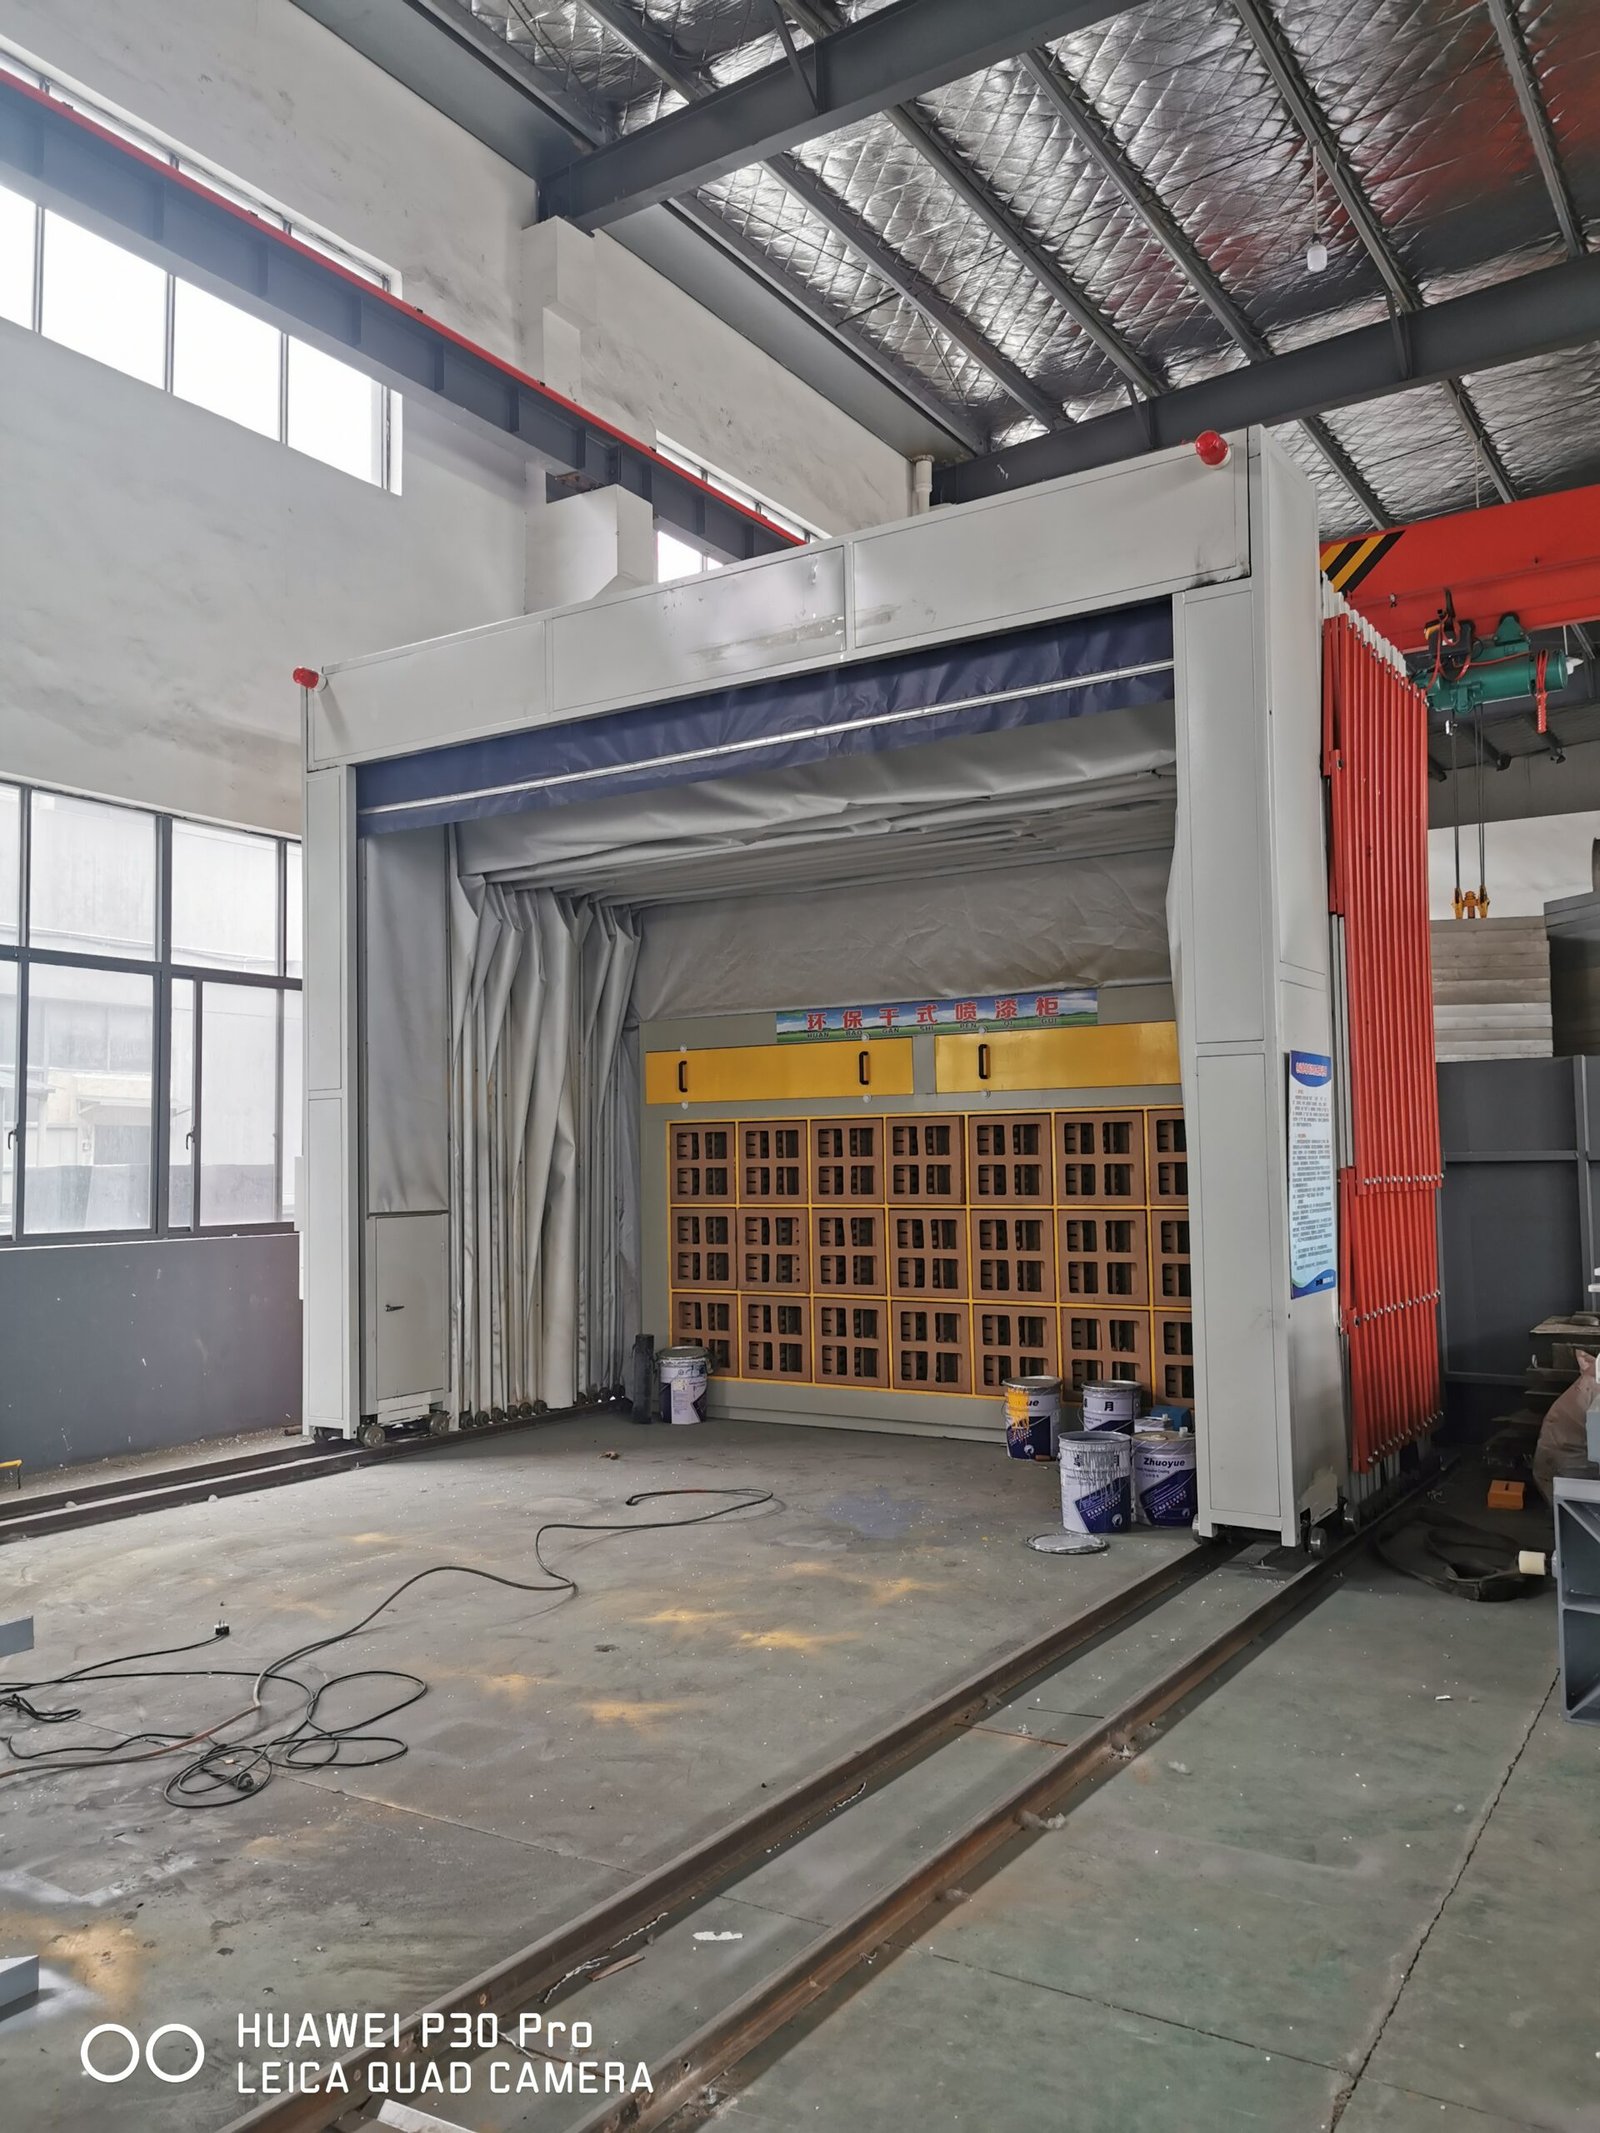
Case Study: Oil-Film Telescopic Spray Booth for a Process Skid Fabricator, Malaysia
Summary
| Object | Pump and filtration skids up to 12 m long for a Oil and gas process skid fabricator in Malaysia |
|---|---|
| Equipment | 13 x 5 x 3 m oil-film telescopic booth |
| Operating conditions | crane-handled batch painting, two oil-film purifiers 1, cross-draft 0.3 m/s or more |
| Result | Skids painted with instruments in place, in an enclosure that inspectors could witness |
| Source | project specification and commissioning scope; client name withheld at the client's request |
Project Background
A Malaysian fabricator of pump, metering and filtration skids for offshore and downstream clients painted skids to client-specified epoxy and polyurethane systems after piping and instrumentation were fitted. Skids were moved by crane and could not be tilted, so a booth that came to the skid was the only practical enclosure.
Pain Points Before the Project
- Skids with instruments fitted cannot be moved on their side through a booth door
- Client inspectors required painting in a controlled, lit enclosure
- Limited floor in a leased shed
- Solvent-borne topcoats with a strict workplace exposure rule
Why This Configuration Was Chosen
- A 13 x 5 x 3 m telescopic booth fits the leased bay and retracts against the end wall
- Two oil-film purifiers handle the daily overspray of high-solids epoxy without filter waste
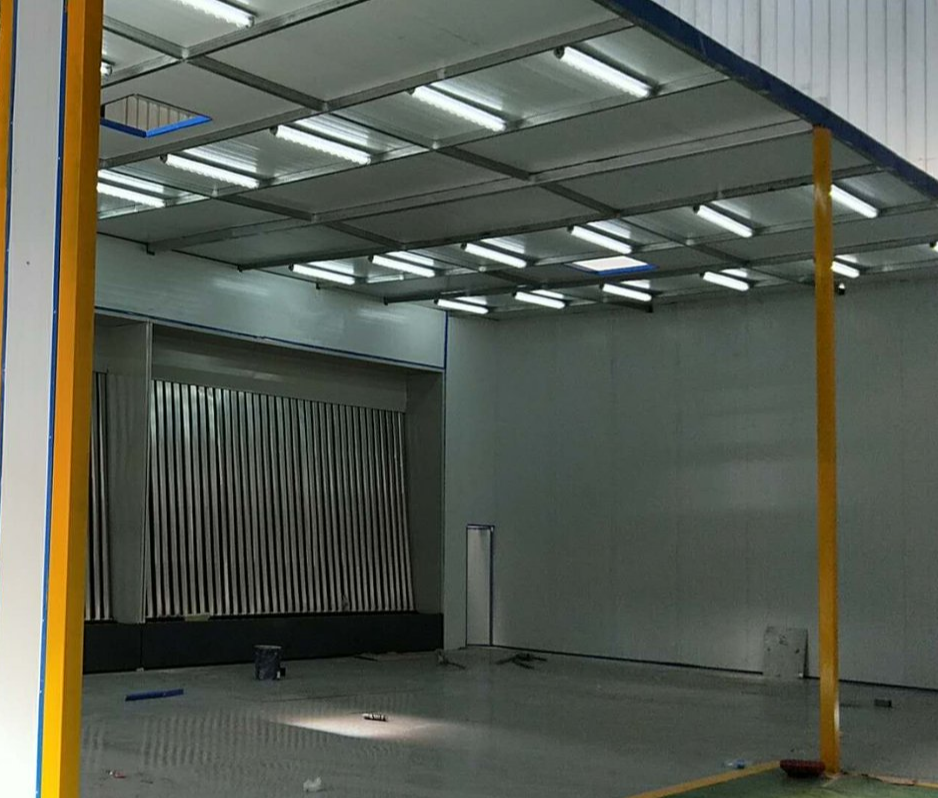
- Carbon adsorption after the oil-film stage met the emission limit at this paint volume; 300 lux or more of explosion-proof lighting satisfied the inspection requirement
Scope of Supply
| Telescopic enclosure | 13 x 5 x 3 m internal; Q235 frames 50 x 70 x 2 mm, flame-retardant PVC fabric |
|---|---|
| Drive and safety | 2 x 1.5 kW explosion-proof geared motors, 8-10 m/min; interlocked drives, double limit switches, rail sweeper, jog control |
| Lighting | Explosion-proof LED, 300 lux or more |
| Paint mist capture | Two oil-film purifiers 1,800 x 1,800 x 3,450 mm, 98% or more mist capture |
| Exhaust treatment | Activated carbon adsorption boxes after the oil-film stage |
| Fan, duct and stack | Centrifugal exhaust fan sized at 0.3 m/s cross-draft (about 16,000 m3/h minimum), 15 m stack |
| Control | Two-station control cabinet, VFD on exhaust fan, emergency stop, audible-visual travel alarm |
| Installed power | about 30-40 kW installed |
Component brands. Key components are sourced from international first-tier brands at the client's choice; the table lists the options offered on this project.
| Component | Brand options |
|---|---|
| Exhaust fan | Nicotra Gebhardt, Kruger, Systemair |
| Geared drive motors | SEW-Eurodrive, NORD, Bonfiglioli |
| Explosion-proof lighting | Eaton Crouse-Hinds, R. STAHL, ABB |
| Low-voltage switchgear | Schneider Electric, Siemens, ABB |
| Variable frequency drive | ABB, Danfoss, Siemens |
| PLC (RCO control) | Siemens, Mitsubishi Electric, Omron |
| Filter media | Andreae Filters, Freudenberg Viledon, Camfil |
| Activated carbon | Calgon Carbon, Jacobi Carbons, Cabot Norit |
| Oxidation catalyst | BASF, Johnson Matthey, Clariant |
| Flame-retardant fabric | Serge Ferrari, Sioen, Mehler Texnologies |
| Flexible cables | LAPP, Nexans, Prysmian |
| Airless spray units (client side) | Graco, WIWA, WAGNER |
Not included: rail levelling and civil foundations, site lifting, third-party emission testing, workpiece stands unless ordered, and the drying room where forced cure is required.
Programme
Typical programme for this booth class; the dates for each project are fixed in the contract.
| Stage | Typical duration |
|---|---|
| Site survey and data collection | 3-7 days |
| Layout and detail design | 10-15 days |
| Manufacture and factory trial | 30-45 days |
| Sea freight and customs | 15-40 days |
| Rail levelling by site, installation | 7-14 days |
| Commissioning, emission test, training | 3-5 days |
Before and After
Design values from the project specification; the "before" column describes the open-floor condition found at survey, for which no measurements existed.
| Item | Before | After |
|---|---|---|
| Enclosure of the painting area | open bay or shed, no enclosure | telescopic booth, 13 x 5 x 3 m |
| Floor available when not painting | painting area blocked or shared | booth retracted, about 85% of footprint freed |
| Cross-draft over the work | not controlled | 0.3 m/s or more (design) |
| Paint mist capture | none | 98% or more (design) |
| VOC treatment efficiency | none | 85-90% (carbon) (design) |
| Lighting at the work surface | workshop lighting | 300 lux or more, explosion-proof (design) |
| Noise inside the booth | not controlled | 80 dB(A) or less (design) |
Results
- Skids painted with instruments in place, in an enclosure that inspectors could witness
- Floor returned to assembly between paint jobs
- Cross-draft of 0.3 m/s or more verified at commissioning
Applicability
This configuration suits workshops where the crane moves the workpiece, painting is done in batches and the floor must return to assembly use between batches: structural steel, vessels and tanks, machinery frames, crane girders, trailer chassis and hull blocks. It is not the right choice for conveyorised lines painting every shift, for coatings that need forced cure inside the same enclosure, or where a water-curtain booth and water treatment already exist.
The results above apply to the configuration and conditions described. A different part mix, paint system, climate or emission limit changes the numbers, which is why every booth is sized from its own data.
After-Sales
Warranty options of 12, 36 or 60 months, remote diagnosis within 2 hours and on-site attendance within 72 hours where a local partner is available, plus filter media, carbon and catalyst supply for the life of the booth. Details are on our after-sales service page.
FAQ
Can the same booth paint different products?
Yes. Nothing in the enclosure is shaped to the part; the booth on this project handled the full range of pump and filtration skids.
Why was oil-film capture chosen here?
Daily painting and a downstream treatment unit favour oil-film purifiers: oil is changed rather than filters replaced, and the catalyst is protected.
What did the client have to prepare?
Levelled rails to our drawing, a concrete pad for the fan and treatment unit, three-phase power to the cabinet and a crane for installation.
How was performance checked?
Travel and limit switches in both directions, drive interlock, cross-draft velocity, lighting level, noise, and stack sampling against the local limit.
Can this booth be extended later?
Frames are added in 1 m modules and the rails extended; the fan and filter wall are sized for the final length at the outset.
Get a Similar Solution
Send us the following and we return a booth layout with fan, filter and treatment sizing within a few working days:
- Largest workpiece length, width, height and weight, and how it is handled
- Daily paint and thinner consumption and the paint system
- Indoor or outdoor installation, crane hook height and available floor
- Local emission limit and workplace exposure rule
WhatsApp us about this case Contact form
Related
- Telescopic mobile spray booth (product page)
- What is a telescopic spray booth and how does it work?
- How to size a telescopic spray booth
- VOC treatment: carbon, UV or RCO
- Paint mixing room
Provided by Lin Cong, Technical Director, MUSI Technology
Published 2026-10-01 · Updated 2026-10-01 · Last technical review: 2026-10-01