EV Battery Pack Housing Coating Line: Powder vs Liquid, Specs and Cost (2026)
Quick answer: An EV battery pack housing coating has to deliver three things at once: dielectric strength, thermal stability through the pack’s operating range, and 500 to 1,000 hours of corrosion resistance. Epoxy or hybrid powder at 80 to 150 microns is the usual answer for aluminium and steel enclosures. A dedicated line runs USD 250,000 to 900,000 depending on housing size and throughput.
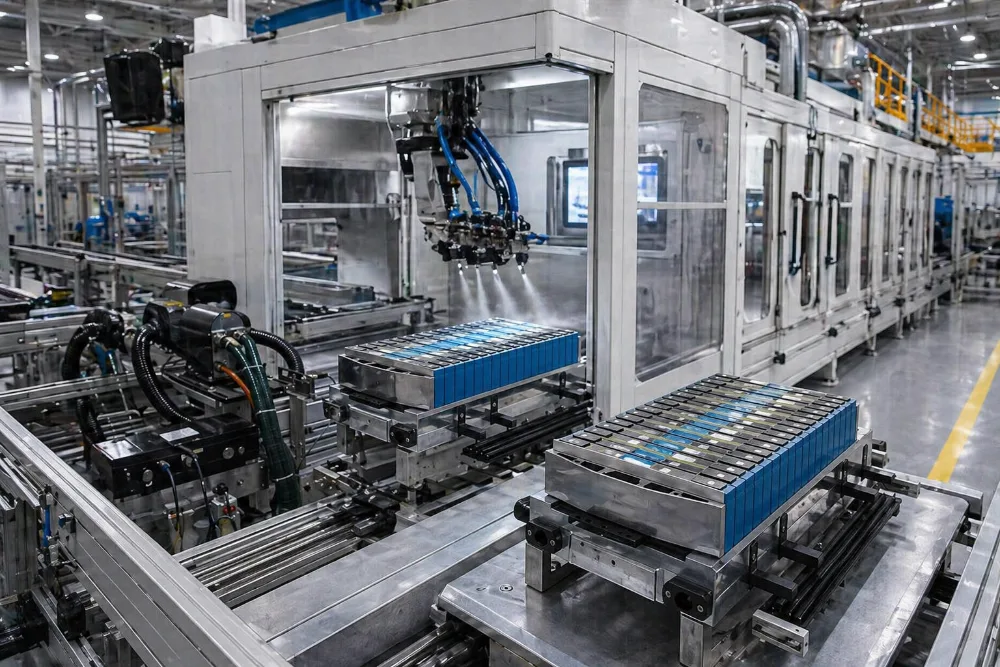
What does a battery pack housing coating actually have to do?
Unlike a body panel, the coating on a pack housing is a functional layer. It insulates conductive surfaces from cell and busbar contact, survives the temperature swing of a liquid-cooled pack, and protects an enclosure that sits under the vehicle floor and is exposed to road salt, stone impact and standing water.
That combination rules out most decorative systems. Specifications typically call for a measured dielectric breakdown value, a defined film build window with both a minimum and a maximum, and edge coverage on every flange and weld.
Powder or liquid for a battery pack housing?
| Criterion | Epoxy or hybrid powder | Two-component liquid |
|---|---|---|
| Typical film build | 80-150 microns single coat | 60-120 microns, often two coats |
| Dielectric strength | High, uniform across the panel | High, more variable at edges |
| Edge coverage | Good with correct kV and flow | Needs stripe coating |
| VOC emission | Near zero | Requires exhaust treatment |
| Cure | 180-200 C, 10-20 min | 60-80 C forced cure or ambient |
| Substrate limit | Metal only | Metal and composite |
| Material utilisation | 95-98% with recovery | 45-70% transfer efficiency |
Powder wins on almost every axis for metal enclosures, and it is the default for aluminium and steel pack housings. Liquid systems appear where the housing is a composite or hybrid assembly that cannot see 180 C, or where a specific dielectric primer is mandated by the customer.
What film build should you target?
Both a minimum and a maximum matter here, which is unusual in industrial coating. Too thin and dielectric performance fails; too thick and the coating becomes brittle and chips at flanges during assembly.
| Surface | Target film | Why |
|---|---|---|
| Internal faces contacting modules | 100-150 microns | Dielectric requirement governs |
| External underbody surfaces | 80-120 microns | Corrosion and stone chip |
| Sealing flanges | 60-90 microns | Gasket compression tolerance |
| Threaded and mating features | Masked | Assembly fit |
Masking is the operation most often underestimated. A pack housing can carry 40 to 120 masked features, and manual masking time frequently exceeds coating time. Reusable silicone caps and purpose-made jigs are worth engineering into the line from the start rather than adding later.
What does the line look like?
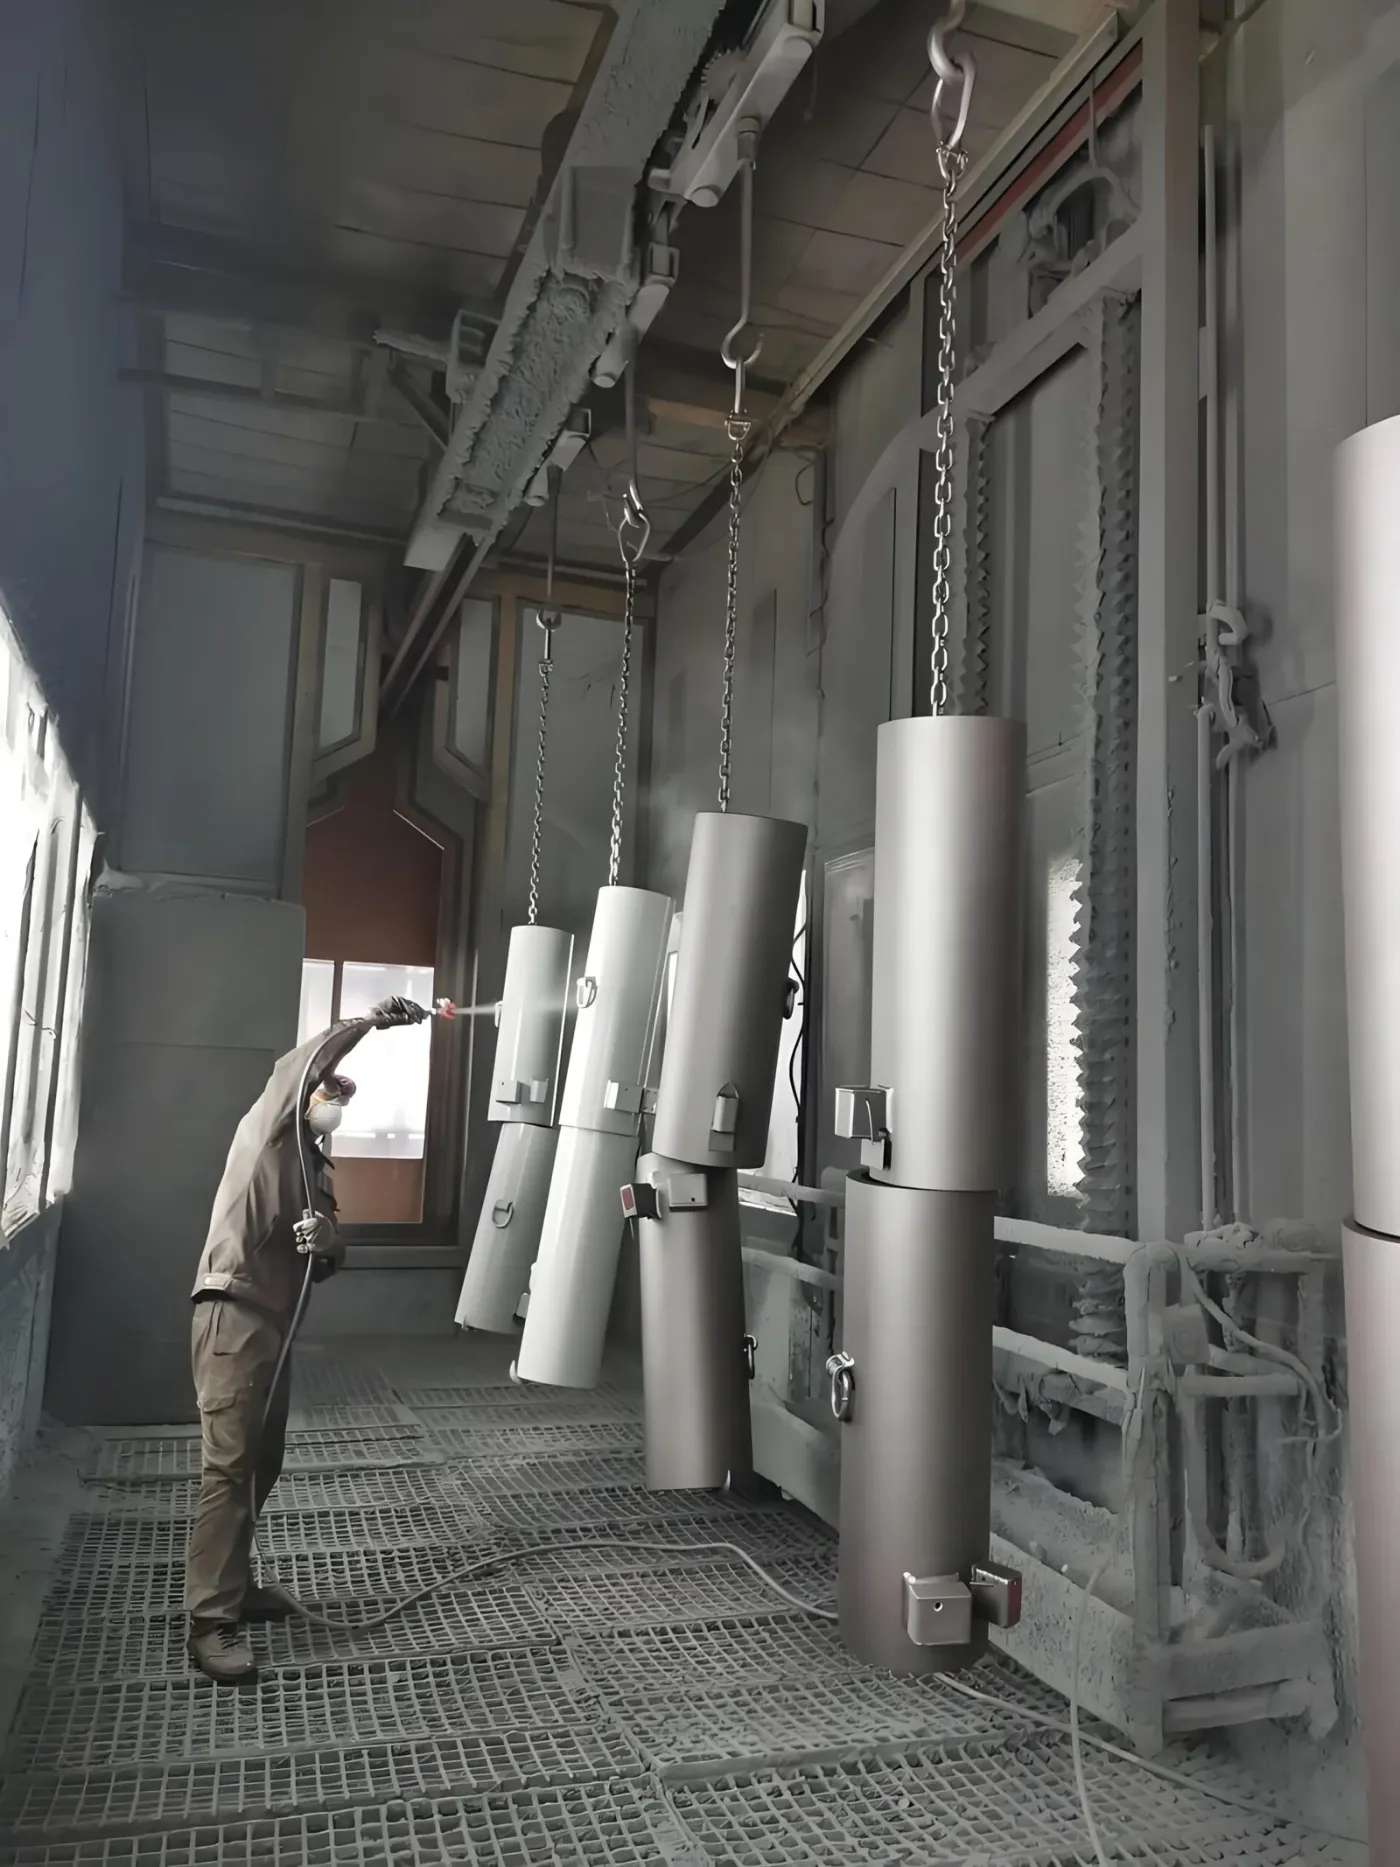
- Pretreatment: five to seven stages, chrome-free zirconium conversion where aluminium and steel share the line.
- Dry-off: 10-15 minutes at 100-120 C, lower for aluminium to avoid soft-coat issues.
- Masking station: a defined station with jig storage, not a bench beside the booth.
- Powder booth: quick colour-change if more than one system runs, with cyclone plus cartridge recovery.
- Curing oven: 180-200 C part metal temperature, with data logging on every batch.
- Cooling and demasking: forced cooling before handling to avoid marking a still-soft film.
- Inspection: film thickness at defined points plus dielectric spot testing.
How much throughput can you get?
| Housing size | Parts per hour | Line speed | Conveyor |
|---|---|---|---|
| Small module case, under 0.5 m2 | 120-300 | 1.5-3.0 m/min | Overhead chain |
| Mid pack housing, 1-2 m2 | 40-120 | 1.0-2.0 m/min | Overhead chain or power-and-free |
| Full floor-pan enclosure, over 3 m2 | 15-45 | 0.8-1.5 m/min | Power-and-free or inverted |
Large floor-pan enclosures usually move to power-and-free or inverted conveying, because the part cannot hang from a hole without distorting and because masking and demasking need the carrier to stop while the line continues.
What does an EV pack housing coating line cost in 2026?
| Configuration | Indicative price (USD, ex-works) |
|---|---|
| Module case line, 5-stage pretreatment, single booth | 250,000-450,000 |
| Pack housing line, 7-stage, quick colour change | 450,000-750,000 |
| Floor-pan enclosure line, power-and-free, full logging | 750,000-900,000 |
| Add: masking station, jigs and storage | 15,000-60,000 |
| Add: dielectric test station | 12,000-40,000 |
What goes wrong on these lines?
| Dielectric failures at flange edges | field concentration thins the film at sharp edges. Break the edge radius at the press stage, and lower gun voltage to 40-60 kV. |
|---|---|
| Chipping during assembly | film above the maximum becomes brittle. Enforce the upper limit, not only the lower one. |
| Masking residue in threads | caps left too long in the oven bond to the surface. Match cap material to the cure profile. |
| Outgassing pinholes on cast components | preheat above cure temperature before powder application. |
| Mixed-metal corrosion | steel and aluminium on the same line need a conversion chemistry that treats both. Zirconium handles it; phosphate does not. |
| Delivery record | 800+ coating lines for 500+ clients in 36 countries (MUSI engineering team, cumulative since 2011) |
| Services | Design, manufacturing, installation, commissioning, operator training and after-sales support from one company |
Working with MUSI Technology on a battery enclosure line
MUSI Technology (Changzhou MUSI Environmental Technology Co., Ltd.) designs and builds turnkey finishing lines from its plant in Changzhou, China, with 800+ coating lines delivered to 500+ clients across 36 countries, from single booths to complete finishing plants.
- Every line is engineered against a written performance specification. Line speed, cure profile, film build window and dielectric requirement are stated in the contract and demonstrated on your own housing at the factory trial run before shipment.
- One engineering team owns the whole chain — pretreatment, masking, application, curing, conveying and emission control — so the trade-offs between them are settled on the drawing board, not on your factory floor.
- Standard configurations ship in 30-60 days with a 12-month full-machine and 36-month critical-component warranty, and on-site installation, commissioning and operator training are available worldwide. Structural parts are covered for up to 60 months.
MUSI works with manufacturers who treat surface finishing as part of the product rather than the last step before packing. Send your housing drawing, masking schedule and annual volume for a layout and budget: contact MUSI Technology. See also the energy storage and battery enclosure coating solutions.
Frequently asked questions
What coating is used on EV battery pack housings?
Epoxy or hybrid powder at 80-150 microns is standard for aluminium and steel enclosures, because it delivers dielectric strength, thermal stability and 500-1,000 hours of corrosion resistance in a single coat with 95-98 percent material utilisation. Two-component liquid systems are used where the housing is a composite or hybrid assembly that cannot see a 180 C cure.
What film thickness does a battery enclosure need?
Internal faces contacting modules typically need 100-150 microns because dielectric performance governs, external underbody surfaces 80-120 microns for corrosion and stone chip, and sealing flanges 60-90 microns so gasket compression stays within tolerance. Unusually for industrial coating, the maximum matters as much as the minimum: film above the upper limit becomes brittle and chips during assembly.
Why do battery housings fail dielectric testing at the edges?
Electrostatic field lines concentrate at sharp edges, so powder deposits thinner there than on flat faces. Two fixes work together: break the edge radius at the pressing stage so there is no knife edge to concentrate the field, and lower gun voltage to 40-60 kV so the field is less aggressive at the perimeter.
How much masking does a pack housing need?
A typical pack housing carries 40-120 masked features, and manual masking time frequently exceeds actual coating time. Reusable silicone caps sized to the cure profile and purpose-built jigs should be engineered into the line from the start, with a defined masking station rather than a bench beside the booth.
What throughput can a battery enclosure coating line reach?
Small module cases under 0.5 m2 run 120-300 parts per hour at 1.5-3.0 m/min. Mid-size pack housings of 1-2 m2 run 40-120 parts per hour. Full floor-pan enclosures above 3 m2 run 15-45 parts per hour and usually need power-and-free or inverted conveying, because the part cannot hang without distorting.
What does an EV battery pack coating line cost?
Indicative 2026 ex-works ranges are USD 250,000-450,000 for a module case line with five-stage pretreatment, USD 450,000-750,000 for a pack housing line with seven stages and quick colour change, and USD 750,000-900,000 for a floor-pan enclosure line with power-and-free conveying and full data logging. A masking station adds USD 15,000-60,000.
About the figures in this guide. Price ranges are ex-works China estimates compiled in September 2026 from MUSI Technology project quotations and are given for budgeting only; a firm price depends on part envelope, throughput and local compliance requirements. Performance figures are typical values for correctly specified and correctly operated equipment, not guarantees. Last reviewed: 10 September 2026.
Send us your part size, throughput and coating type — our engineers reply within 24 hours, and a layout and budget follow once your part data is complete. Contact MUSI Technology or browse our equipment range.
Further Reading
- ProductsEnergy Storage Container Coating Line
- IndustryEnergy Storage Container Coating
- Technical guidesEnergy Storage Container Coating Line: Corrosion Spec and Layout (2026)
- Case StudiesEV Battery Pack Housing Coating Line
- NewsPowder Coating in the EV Industry: Growth and Outlook
QQuestions buyers ask before ordering
quotation · price · lead time · installation · warranty
What information do you need to prepare a quotation?
Send part drawings or photos, the largest part size and weight, the material, the required output per shift, the paint or powder type and number of colours, and the available floor space, ceiling height and power or gas supply. MUSI engineers reply within 24 hours; a recommended configuration and quotation follow once your part data is complete.
How much does this equipment cost?
Budget depends on part size, throughput and the level of automation. Indicative ex-works ranges are published in our powder coating line guide (indicative ex-works budgets from USD 75,000 to 2,000,000); a configured quotation is prepared from your part data.
What is the lead time?
Standard configurations ship in 30–60 days from contract signing and down payment; custom configurations take longer. The delivery date is fixed in the contract.
Do you install and train operators overseas?
Yes. MUSI engineers carry out on-site installation and commissioning and give 3–5 days of operator and maintenance training. MUSI has delivered 800+ coating lines to customers in 36 countries.
What warranty and after-sales support are included?
12 months full-machine warranty, 36 months on critical components and up to 60 months on structural parts. International customers get 24-hour phone response and 72-hour on-site arrival; spare parts ship from the Changzhou headquarters.
Can the environmental equipment be supplied with the line?
Yes. VOC treatment (RTO, RCO, activated carbon, zeolite rotor), dust collection and paint wastewater treatment are supplied with the coating line under one contract; MUSI has equipped 50+ coating facilities whose projects all passed local environmental compliance reviews.
More questions from buyers
Is dielectric powder coating applied to EV and ESS housings?
Yes. Dielectric powder coating with epoxy or hybrid powder is the standard on EV battery housings: internal faces that touch the modules are coated to 100-150 microns because the insulation requirement governs. Energy storage (ESS) enclosures follow the same principle.