Powder Coating Guns and Equipment Guide (2026)
Quick answer: A powder coating gun gives each powder particle an electrostatic charge so it is attracted to the earthed part. Corona guns do this with a high-voltage electrode, typically 30-100 kV at negative polarity, and work with almost any powder; tribo guns charge the powder by friction inside the gun barrel with no high-voltage supply, which largely avoids the Faraday cage effect in recesses but needs powder formulated for tribo charging. Manual guns suit touch-up and small batches; automatic guns on reciprocators or robots coat the main volume on a conveyorised line, fed by venturi or dense-phase pumps and backed by a cyclone or cartridge recovery system.
MUSI Technology, a powder and liquid spray coating line manufacturer in Changzhou, China, fits corona guns as standard on its powder lines and supplies guns and control units from Gema, Nordson or Wagner when the customer specifies a brand.
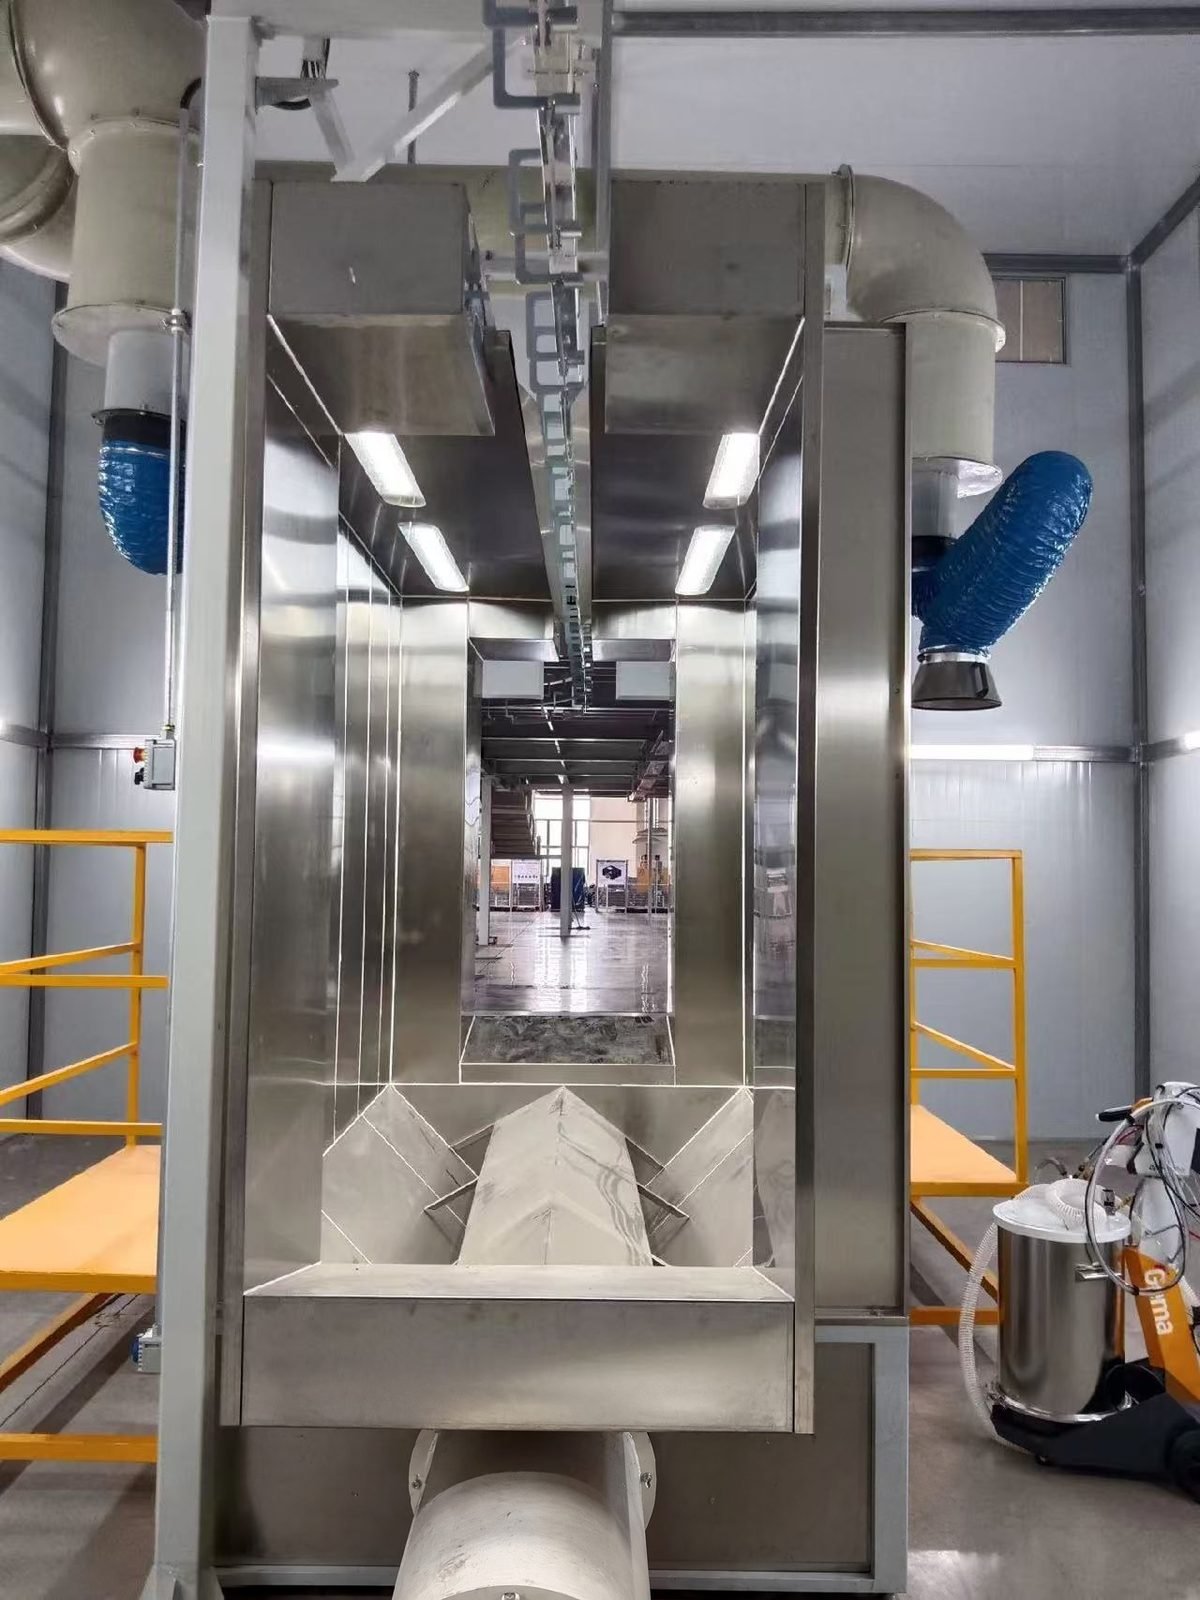
What does a powder coating gun system include?
A gun is only one part of the application system. Powder is fluidised in a feed hopper or drawn from the box, carried by a pump through a hose to the gun, charged at the gun tip and sprayed into the booth. Whatever does not stick is pulled into the recovery unit and returned to the hopper. The control unit sets voltage, current and powder flow for each gun. On an automatic line the guns are mounted on a reciprocator or robot and the control unit stores recipes per part.
| Component | Job | Typical options |
|---|---|---|
| Gun | Charges the powder and shapes the spray pattern | Corona (electrode) or tribo (friction) |
| Pump | Moves powder from hopper to gun | Venturi or dense phase |
| Control unit | Sets kV, µA and powder / air flow | Recipes per part on automatic lines |
| Gun mover | Carries automatic guns | Reciprocator, fixed stand or robot |
| Booth | Contains the cloud at a steady inflow | Steel, stainless or plastic walls |
| Recovery | Returns overspray to the hopper | Cyclone plus final filter, or cartridge |
Corona or tribo charging: which should you choose?
Corona charging is the industrial default. The electrode at the gun tip ionises the air and the ions charge the powder in flight; negative polarity is used because it produces more ions and arcs less than positive. The charged cloud follows the field lines to the nearest earthed surface, which is efficient on flat and open parts but tends to build powder on edges and leave deep corners thin, the Faraday cage effect. Tribo guns charge the powder by friction against the barrel wall instead, so there is no strong external field: powder penetrates recesses and edges build up less, at the price of being more dependent on the chemistry and particle size of the powder, which must be tested before use.
| Corona | Tribo | |
|---|---|---|
| Charging method | High-voltage electrode ionises the air | Friction against the barrel wall |
| Voltage | Typically 30-100 kV, negative polarity | No high-voltage supply |
| Powder choice | Almost any standard powder | Powder must be suitable for tribo; test first |
| Recesses and corners | Faraday cage effect, edges build up | Better penetration, more uniform film |
| Flat and open parts | Fast, high deposition | Slower build |
| Typical use | Most industrial lines | Deep profiles, cages, wire goods |
If you coat deep channels, wire baskets or radiator fins, ask for a trial with tribo or with a corona gun at reduced kV and current limiting; many lines solve recesses with corona plus a manual touch-up station rather than switching technology.
Manual or automatic guns?
Manual guns are used for low volumes, frequent part changes, and as touch-up stations before and after the automatic zone, where an operator fills recesses the automatic guns cannot reach. Automatic guns carry the main load on a conveyorised line: they are mounted on reciprocators for flat and repetitive parts, or on robots where geometry and model mix justify it. The number of automatic guns follows conveyor speed, part height and film thickness, not the booth size. The trade-off between reciprocators and robots is covered in robotic spray painting vs reciprocator.
| Manual guns | Automatic guns | |
|---|---|---|
| Volume | Small batches, jobbing | Continuous conveyor production |
| Consistency | Depends on the operator | Repeatable film from stored recipes |
| Recesses | Operator can aim into them | Need touch-up or robot paths |
| Labour | One operator per gun | Guns run unattended; staff for touch-up and loading |
| Typical place on a line | Pre and post touch-up stations | Main coating zone on reciprocators or robots |
Venturi or dense-phase powder pumps?
Conventional venturi pumps entrain powder in a fast air stream: they use about 3-4 cfm of air to deliver powder, which leaves the throat at roughly 50-55 ft/s with a cloud density of about 0.2 lb/ft3. Dense-phase pumps move the same amount of powder with about 0.5-1.0 cfm of air, giving a denser, slower cloud of about 0.45 lb/ft3 that charges more efficiently, through hoses under 1/4 inch instead of 1/2 inch, which makes colour change faster and lets powder be pumped back to the supply. One Nordson user reported around 30% powder savings after moving from venturi to dense-phase pumps; savings depend on the parts and the line.
| Venturi pump | Dense-phase pump | |
|---|---|---|
| Air to deliver powder | About 3-4 cfm | About 0.5-1.0 cfm |
| Powder velocity at throat | About 50-55 ft/s | Lower, softer cloud |
| Cloud density | About 0.2 lb/ft3 | About 0.45 lb/ft3 |
| Hose bore | About 1/2 in | Under 1/4 in |
| Colour change | Longer hose purge | Faster; powder can be reversed to supply |
| Purchase cost | Lower | Higher |
Which gun brands are fitted to industrial lines?
Three Western brands supply most of the guns specified by export buyers. The figures below are from the manufacturers’ own product information; MUSI fits any of them on request and integrates them with its own booths, recovery units and conveyors.
| Brand | Example product | Published data |
|---|---|---|
| Gema (Switzerland) | OptiFlex Pro manual system with OptiSelect Pro gun | 110 kV and 110 µA with PowerBoost; OptiStar 4.0 control; ATEX-certified gun and nozzles |
| Nordson (USA) | Encore HD manual system | Encore HDLV dense-phase pump; automatic pump purge; ATEX-approved touchscreen controller |
| Wagner (Germany) | PEM-X1 manual corona gun | 100 kV output; gun weight 0.5 kg; air inlet 0.3 MPa |
What settings matter on the line?
Start with the gun 200-300 mm (8-12 in) from the part and adjust from there; closer raises deposition and the risk of back-ionisation, further reduces wrap. Keep the booth inflow steady at around 0.5 m/s (100 ft/min) across the openings so the cloud stays inside without stripping powder from the part. The application room is best held at about 20-27 °C and 47-55% relative humidity, since damp powder fluidises and charges poorly. First-pass transfer efficiency is limited, typically no more than about 50% with guns running continuously, which is why recovery matters: with a cyclone or cartridge returning overspray to the hopper, overall powder utilisation on a single-colour line often exceeds 95%.
| Parameter | Typical value | Why it matters |
|---|---|---|
| Gun-to-part distance | 200-300 mm (8-12 in) to start | Adjust per part |
| Booth inflow at openings | About 0.5 m/s (100 ft/min) | Keeps the cloud in the booth |
| Room temperature | About 20-27 °C | Stable powder flow |
| Relative humidity | About 47-55% | Dry powder charges better |
| First-pass transfer efficiency | Typically up to about 50% | Continuous gun operation |
| Overall utilisation with recovery | Often above 95% | Single-colour reclaim |
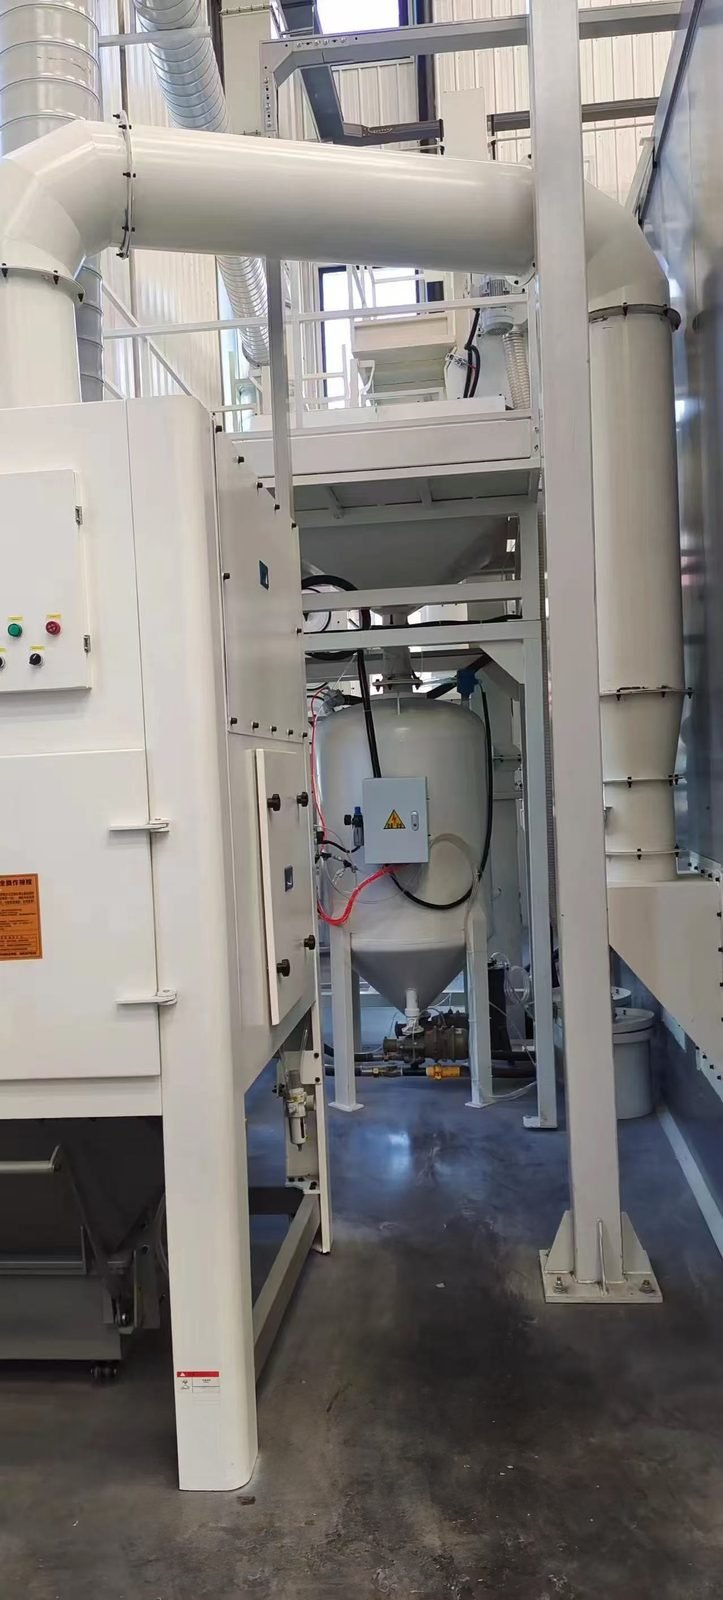
How the booth airflow and recovery are laid out is explained in how a powder coating booth works, and fast colour change in the quick colour change booth guide. If film thickness or finish is the problem rather than the gun, see powder coating defects, causes and solutions.
FAQ
How many kV should a powder gun run at? Corona guns are rated up to about 100-110 kV, but the right setting depends on the part; recesses and second coats often need lower voltage with current limiting to avoid back-ionisation.
Can one gun spray any powder? A corona gun handles almost all standard powders; a tribo gun needs powder formulated for tribo charging, so test the powder first.
Do I need dense-phase pumps? They pay off where colour changes are frequent or powder cost is high; on a single-colour line with long runs, venturi pumps are still common.
Can a line mix brands? Yes. Guns and control units from one brand are normally kept together, while the booth, recovery unit and conveyor come from the line builder.
Where MUSI Technology fits
MUSI Technology designs and builds complete powder coating lines, from pretreatment and drying ovens to booths, recovery units, curing ovens and conveyors, and sizes the gun count and pump type to the parts and throughput. The overall line is described in the powder coating line guide and budgets in how much a complete coating line costs.
Provided by Lin Cong, Technical Director, MUSI Technology
Send us your part size, throughput and coating type — our engineers reply with a layout and budget within one working day. Contact MUSI Technology or browse our equipment range.
Related technical guides
- Powder Coating Line: Types, Specs & Cost (2026)
A powder coating line pretreats, coats and cures metal parts on a conveyor. Full guide to line types, key specifications and 2026 price ranges. - Powder Coating Pretreatment Line: Stages & Cost
A pretreatment line degreases, rinses and chemically converts the metal surface before coating. Three, five and seven-stage layouts, phosphate versus. - BESS Container Coating Line: Spec & Corrosion
Battery energy storage containers need C4 to C5-M corrosion protection: shot blasting to Sa2.5, zinc-rich primer and weather-resistant polyester topcoat. - EV Battery Pack Housing Coating Line: Specs & Cost
Battery pack housings need dielectric strength, thermal stability and corrosion life in one coating. Powder versus liquid compared, film build targets,. - Spray Coating Line: Types, Specs & Cost (2026)
What a spray coating line costs, how the main types compare on throughput and finish, and the specs to fix before you ask for quotations.