Shot Blasting vs Sandblasting: Which Surface Preparation for Your Parts? (2026)
Quick answer: Shot blasting throws abrasive mechanically using rotating wheels; sandblasting propels it with compressed air through a nozzle. Shot blasting cleans 3-8 times faster and uses roughly one fifth of the energy per m2, so it suits high volume. Sandblasting reaches recesses and complex geometry, handles delicate or very large parts, and costs far less to buy.
MUSI Technology, which builds shot blasting equipment and sandblasting rooms in Changzhou, China, recommends shot blasting for high-volume parts, since it cleans 3-8 times faster at roughly one fifth of the energy per m2, and a sandblasting room for recesses, complex geometry, delicate or very large parts, and lower purchase budgets.
What is the actual difference between the two processes?
The difference is how the abrasive gets its energy. A blast wheel spins at 2,000-3,000 rpm and flings abrasive by centrifugal force, delivering a wide, high-mass stream. An air nozzle accelerates abrasive with compressed air at 5-7 bar, delivering a narrow, precisely aimed stream.
That single difference drives everything else: coverage rate, energy consumption, achievable geometry, and how much of the part the operator has to reach.
Shot blasting vs sandblasting compared
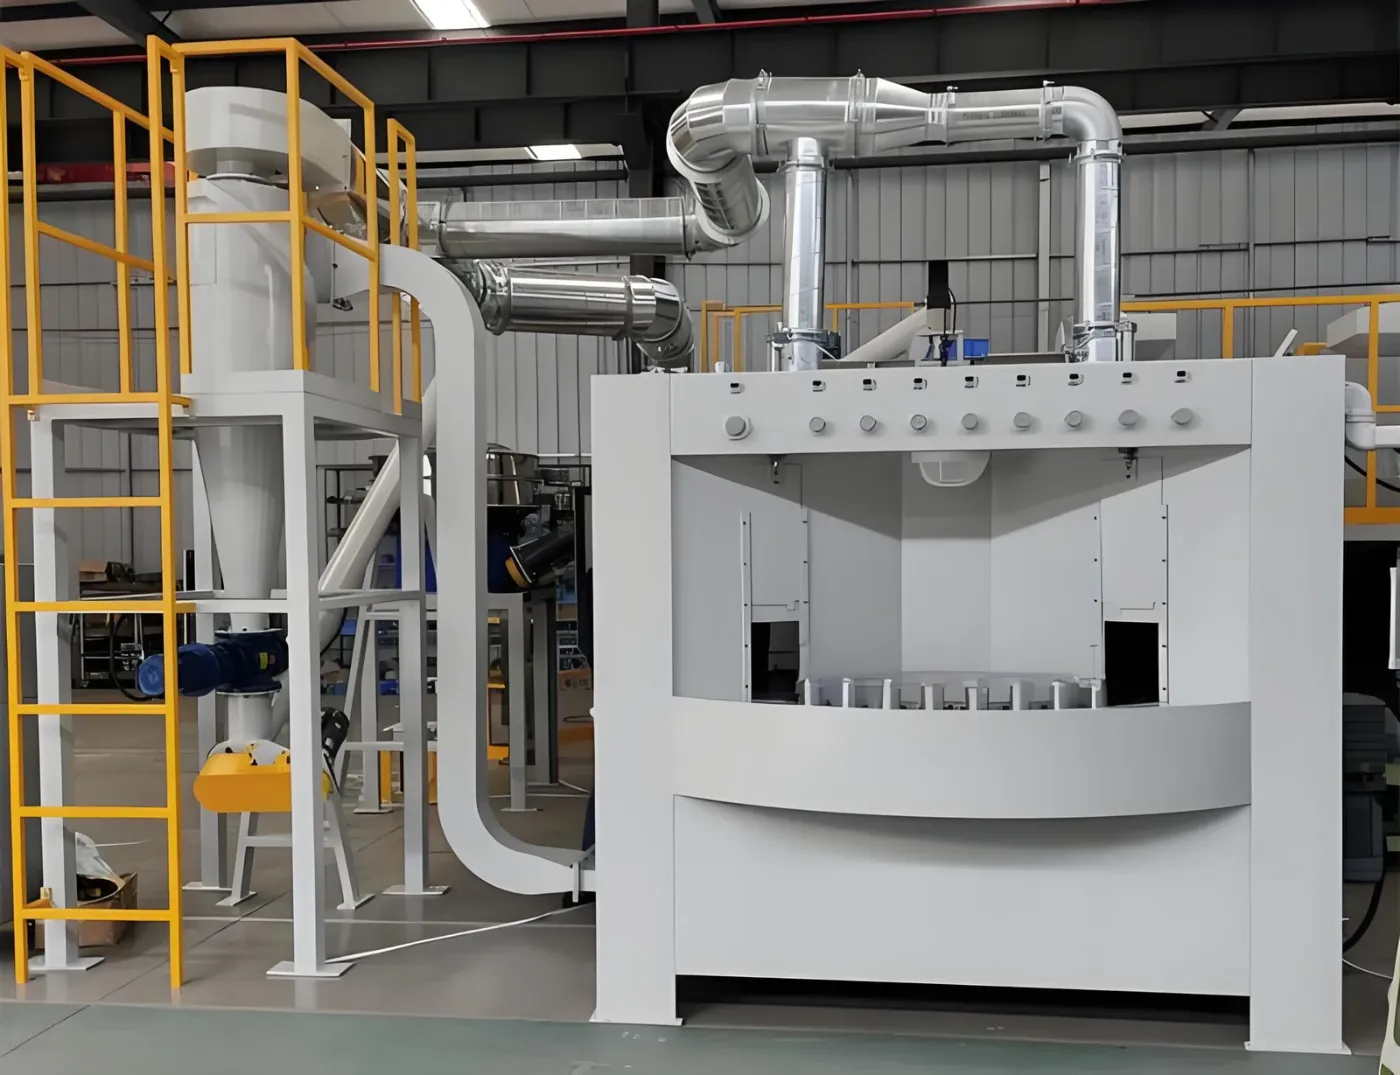
| Criterion | Shot blasting (wheel) | Sandblasting (air) |
|---|---|---|
| Coverage rate | 15-60 m2/h per wheel | 4-12 m2/h per nozzle |
| Energy per m2 cleaned | Low (approx. 0.2-0.5 kWh) | High (approx. 1.0-2.5 kWh) |
| Typical abrasive | Steel shot, steel grit | Garnet, alumina, glass bead, steel grit |
| Surface profile achievable | 25-100 microns | 15-125 microns |
| Complex geometry and recesses | Limited | Excellent |
| Part size limit | Fits machine chamber | Any size in a blast room |
| Machine price (indicative) | USD 15,000-180,000 | USD 2,000-45,000 |
| Labour | Load and unload only | Operator blasts continuously |
Which process should you choose for your parts?
| Castings, forgings, fasteners in volume | tumble belt shot blasting. Highest throughput per operator. |
|---|---|
| Heavy weldments and structural parts | hook type shot blasting, up to several tonnes per hook. |
| Steel plate, H-beam, profiles | roller conveyor shot blast line, in-line ahead of coating. |
| Complex housings, internal surfaces, welds | air blasting in a cabinet or blast room. |
| Aluminium, stainless, thin sheet | air blasting with glass bead or alumina, to avoid impregnating steel particles. |
| Very large fabrications, on-site work | blast room or open-air blasting with air equipment. |
| Delivery record | 800+ coating lines for 500+ clients in 36 countries (MUSI engineering team, cumulative since 2011) |
| Services | Design, manufacturing, installation, commissioning, operator training and after-sales support from one company |
Many plants use both: a shot blast line to remove scale in bulk, followed by spot air blasting for welds and areas the wheels cannot reach.
What surface standard do you need before coating?
Coating specifications normally reference ISO 8501-1 cleanliness grades. Sa2.5, near-white metal, is the usual requirement before industrial powder or liquid coating, and both processes reach it with correct media and dwell time.
| Grade | Description | Typical use |
|---|---|---|
| Sa1 | Light blast cleaning | Temporary protection only |
| Sa2 | Thorough blast cleaning | Indoor, mild service |
| Sa2.5 | Very thorough, near-white | Industrial coating standard |
| Sa3 | Blast cleaning to visually clean steel | Marine, offshore, tank lining |
Surface profile matters as much as cleanliness. Most powder systems want 25-75 microns; too smooth and adhesion suffers, too rough and film build has to increase to cover the peaks.
Which abrasive should you use?
| Media | Effect | Best for | Reuse cycles |
|---|---|---|---|
| Steel shot (round) | Peens, cleans, low profile | Descaling, shot peening | 1,500-3,000 |
| Steel grit (angular) | Cuts, high profile | Rust removal, coating anchor | 800-2,000 |
| Garnet | Sharp, low dust, no free silica | Air blasting steel | 3-8 |
| Aluminium oxide | Very sharp, aggressive | Hard alloys, stainless | 5-15 |
| Glass bead | Cleans without profile change | Aluminium, cosmetic finish | 5-12 |
Silica sand is banned or restricted in many markets because of the silicosis risk. Garnet and alumina are the normal substitutes for air blasting.
How much do the machines cost in 2026?
| Machine | Indicative price (USD, ex-works) |
|---|---|
| Manual blast cabinet | 2,000-9,000 |
| Blast room, 4 x 3 x 8 m, with recovery | 25,000-90,000 |
| Tumble belt shot blast machine | 15,000-55,000 |
| Hook type shot blast machine | 28,000-110,000 |
| Roller conveyor shot blast line | 45,000-180,000 |
Every machine above needs a dust collector, which is quoted separately at roughly 10-20% of machine value. See our guide to sizing dust collection for coating and blasting shops.
Why source blasting equipment from MUSI Technology?
MUSI Technology (Changzhou MUSI Environmental Technology Co., Ltd.) is a China-based manufacturer of surface preparation and coating equipment, with 800+ coating lines delivered to 500+ clients across 36 countries, from single booths to complete finishing plants. The blasting range covers rotary table, hook type, tumble belt and roller conveyor shot blast machines plus manual blast cabinets, each supplied with a matched dust collector.
- Machine selection based on your part weight, geometry and required cleanliness grade.
- Standard configurations ship in 30-60 days with a 12-month full-machine and 36-month critical-component warranty. Structural parts are covered for up to 60 months.
- On-site installation, commissioning and operator training available worldwide.
- Every line is engineered against a written performance specification. Line speed, cure profile, film build and emission level are stated in the contract and demonstrated on your own part at the factory trial run before shipment.
- One engineering team owns the whole chain — pretreatment, application, curing, conveying and emission control — so the trade-offs between them are settled on the drawing board, not on your factory floor.
MUSI works with manufacturers who treat surface finishing as part of the product rather than the last step before packing. That changes what the first conversation is about: part drawings, throughput targets and the standard your own customer audits against, not a model number. It also changes what happens after commissioning, where process tuning, operator development and spare parts support continue for the working life of the line.
See the sandblasting and shot peening range or read the full sandblasting and shot peening equipment guide.
Frequently asked questions
Is shot blasting faster than sandblasting?
Yes, substantially. A single blast wheel covers 15-60 m2 per hour against 4-12 m2 per hour for one air nozzle, and uses roughly one fifth of the energy per m2 because it does not rely on compressed air. Shot blasting is therefore the standard choice for volume production, while air blasting wins on geometry and flexibility.
Can shot blasting reach inside recesses and complex parts?
Not reliably. A blast wheel produces a wide stream fixed in direction, so shadowed areas, deep recesses and internal surfaces receive little abrasive. Air blasting with a hand-held nozzle reaches these areas. Many plants shot blast in bulk and then spot blast welds and recesses with air equipment.
What surface grade do I need before powder coating?
Sa2.5 to ISO 8501-1, described as near-white metal, is the normal industrial requirement. Surface profile should usually fall between 25 and 75 microns. Too smooth reduces adhesion; too rough forces higher film build to cover the peaks.
Which abrasive should I use on aluminium?
Glass bead or aluminium oxide. Steel shot and grit leave embedded iron particles in aluminium that cause corrosion spots after coating. Glass bead cleans without significantly changing the profile and gives a uniform satin appearance, while alumina is used when a coating anchor profile is required.
How much does a shot blasting machine cost?
Indicative 2026 ex-works ranges are USD 15,000-55,000 for a tumble belt machine, USD 28,000-110,000 for a hook type machine, and USD 45,000-180,000 for a roller conveyor line. A manual blast cabinet costs USD 2,000-9,000 and a 4 x 3 x 8 m blast room USD 25,000-90,000. A matched dust collector adds roughly 10-20%.
Is silica sand still allowed for blasting?
It is banned or heavily restricted in many markets because inhaled crystalline silica causes silicosis. Garnet and aluminium oxide are the usual substitutes for air blasting, and steel shot or grit is used in enclosed wheel machines where the media is recycled in a closed loop.
About the figures in this guide. Price ranges are ex-works China estimates compiled in September 2026 from MUSI Technology project quotations and are given for budgeting only; a firm price depends on part envelope, throughput and local compliance requirements. Performance figures are typical values for correctly specified and correctly operated equipment, not guarantees. Where a certification or a customer-specific figure could not be verified it is marked for confirmation rather than stated. Last reviewed: 9 September 2026.
Related guide: Shot Peening vs Shot Blasting vs Sandblasting: Purpose, Parameters and Machine Choice
Send us your part size, throughput and coating type — our engineers reply within 24 hours, and a layout and budget follow once your part data is complete. Contact MUSI Technology or browse our equipment range.
Related technical guides
- Coating Line Conveyor Types Compared (2026)
Overhead chain, floor belt, power-and-free and inverted conveyors compared on part weight, throughput, buffering, floor space and 2026 cost per metre. - Coating Line Wastewater Treatment: Process & Cost
Pretreatment lines discharge phosphates, heavy metals and surfactants. Coagulation, flocculation, sedimentation and filtration explained, with sludge. - Metal Hardware Coating Line: Design & Cost per Part
Hardware plants live on variety, not volume. Dense hanging, 10-25 minute colour change, rack design and the real cost per coated part, with line. - VOC Treatment: RTO vs RCO vs Carbon vs Rotor
Compare RTO, RCO, activated carbon adsorption and zeolite rotor concentrators for spray coating line VOC treatment: efficiency, cost and best fit. - Aluminium Profile Coating Line: Vertical vs Horizontal
Vertical aluminium profile coating lines handle 6-7 m extrusions with less handling damage and a smaller footprint; horizontal lines cost less and suit.
QQuestions buyers ask before ordering
quotation · price · lead time · installation · warranty
What information do you need to prepare a quotation?
Send part drawings or photos, the largest part size and weight, the material, the required output per shift, the paint or powder type and number of colours, and the available floor space, ceiling height and power or gas supply. MUSI engineers reply within 24 hours; a recommended configuration and quotation follow once your part data is complete.
How much does this equipment cost?
Budget depends on part size, throughput and the level of automation. Indicative ex-works ranges are published in our sandblasting and shot peening cost guide; a configured quotation is prepared from your part data.
What is the lead time?
Standard configurations ship in 30–60 days from contract signing and down payment; custom configurations take longer. The delivery date is fixed in the contract.
Do you install and train operators overseas?
Yes. MUSI engineers carry out on-site installation and commissioning and give 3–5 days of operator and maintenance training. MUSI has delivered 800+ coating lines to customers in 36 countries.
What warranty and after-sales support are included?
12 months full-machine warranty, 36 months on critical components and up to 60 months on structural parts. International customers get 24-hour phone response and 72-hour on-site arrival; spare parts ship from the Changzhou headquarters.
Can the environmental equipment be supplied with the line?
Yes. VOC treatment (RTO, RCO, activated carbon, zeolite rotor), dust collection and paint wastewater treatment are supplied with the coating line under one contract; MUSI has equipped 50+ coating facilities whose projects all passed local environmental compliance reviews.
More questions from buyers
Shot peening vs sandblasting: what is the difference?
Shot peening vs sandblasting is a difference of purpose: shot peening strikes the surface with round media to leave compressive stress and delay fatigue cracks, while sandblasting cuts the surface with angular abrasive to clean it and give a coating anchor.
Related: shot peening machine