Coating Line Conveyors: Overhead Chain vs Floor Belt vs Power-and-Free (2026)
Quick answer: Overhead chain conveyors carry hanging parts continuously at 1-6 m/min and are the default for coating lines. Floor belt conveyors suit flat panels laid down. A floor belt is what most buyers mean by a conveyor belt coating line, and it earns its place where parts are flat, heavy, or awkward to hang. Power-and-free adds stop-and-buffer capability for mixed models and manual stations. Indicative cost is USD 180-450 per metre for overhead chain and USD 600-1,600 per metre for power-and-free.
Overhead conveyor systems for coating lines
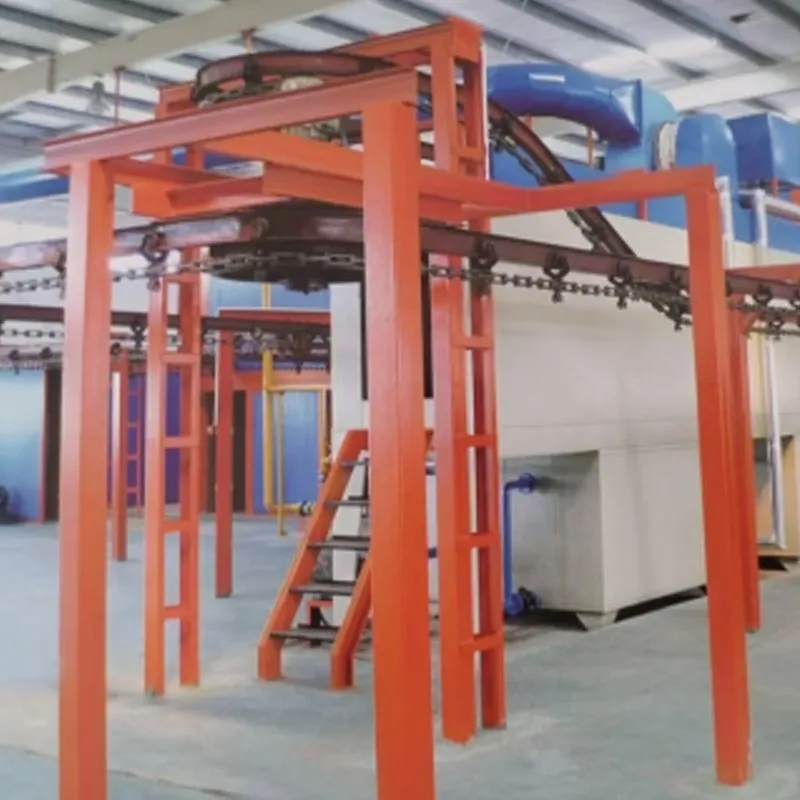
Most powder coating conveyor systems are overhead conveyors: an overhead chain conveyor with I-beam track, an enclosed track conveyor for light parts and clean powder rooms, or an overhead monorail conveyor with trolleys for heavy hangers. Power and free conveyors add a second free track so hangers can stop, accumulate and switch lines while the drive chain keeps moving. Floor belt conveyors handle flat panels that cannot hang.
- Overhead chain conveyor: continuous, simplest, the default for automatic powder coating lines; see the overhead chain conveyor spray line.
- Enclosed track conveyor: sealed track, less dust and lubricant contamination.
- Power and free conveyor: stop-and-buffer, mixed-model production, higher cost.
- Floor belt conveyor coating line: flat parts and sheets; see the floor belt conveyor coating line.
Overhead conveyor manufacturer checklist
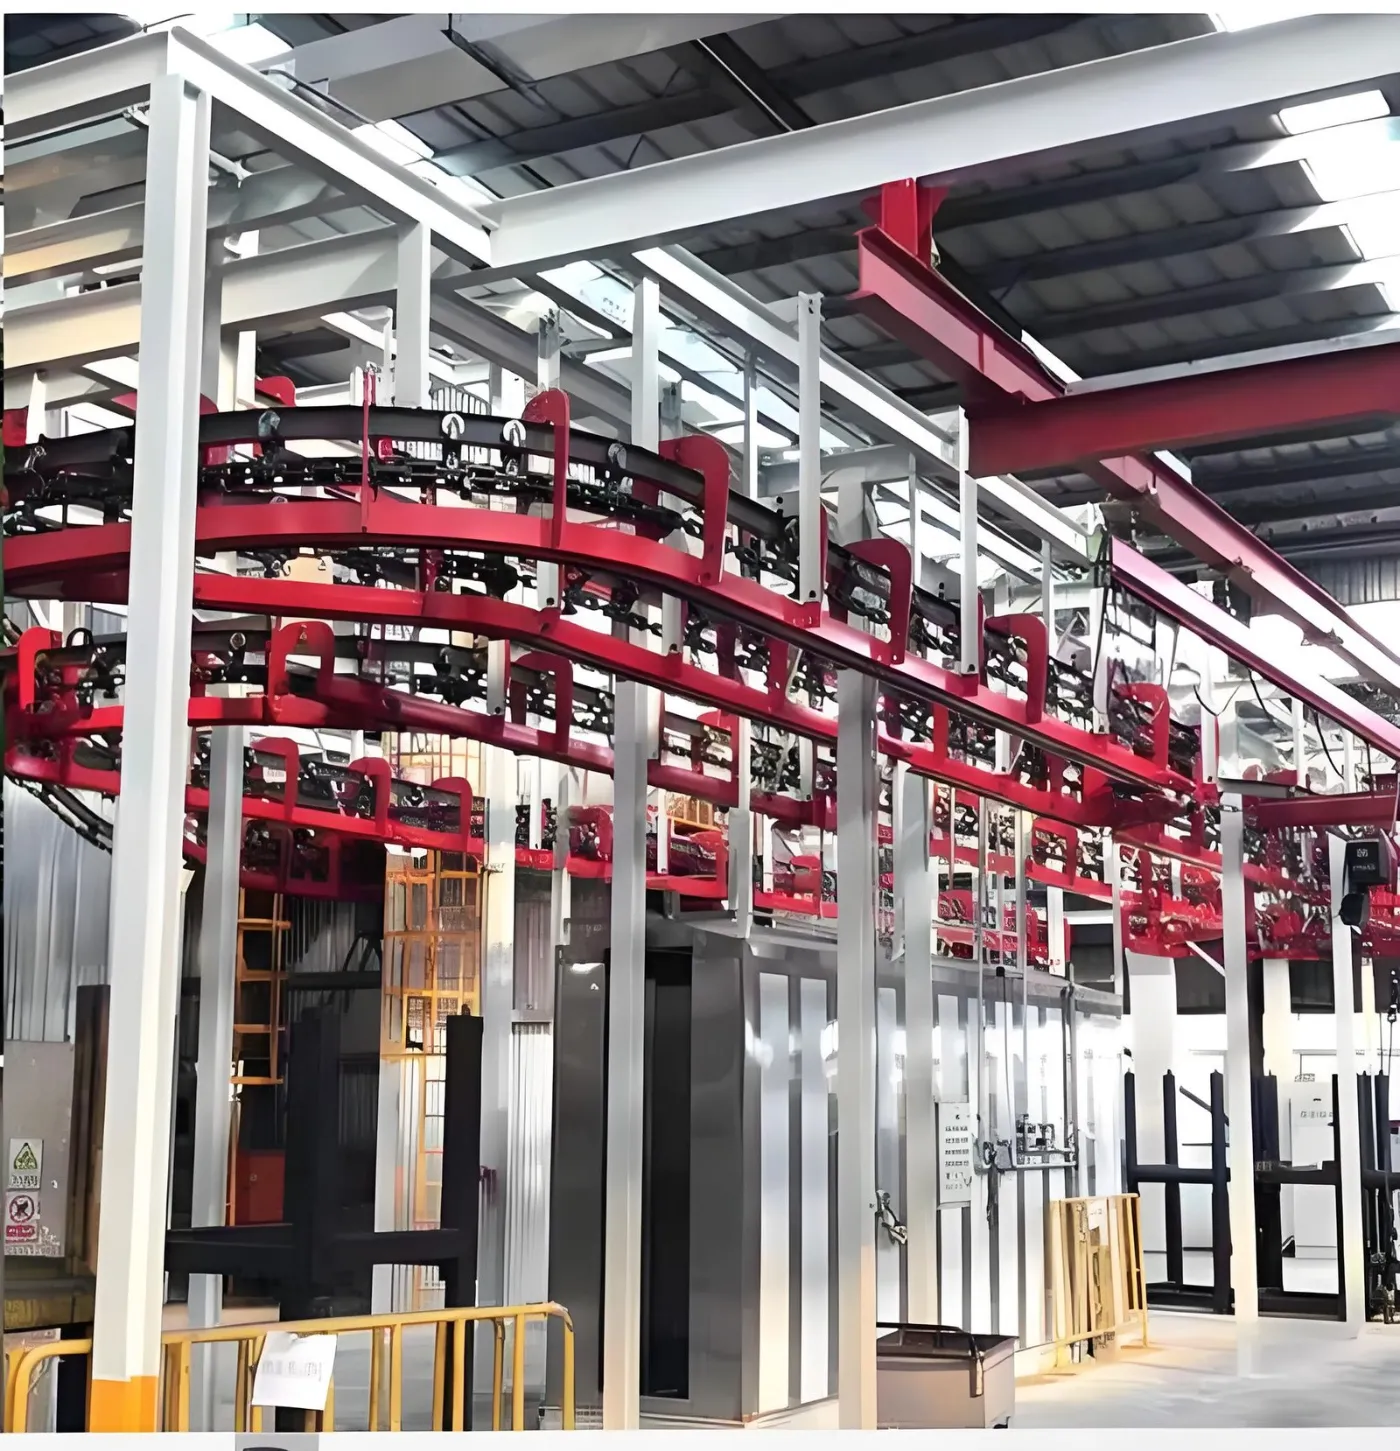
When comparing overhead conveyor manufacturers for a painting system, check load per hanger, chain pitch and pull, track radius, oven pass-through design, drive redundancy and the lubrication method used inside the booth zone. These decide line speed and uptime more than the conveyor price.
Why does the conveyor decision come first?
The conveyor fixes line speed, and line speed fixes oven length, tunnel length and therefore most of the capital cost. Changing conveyor type after the layout is frozen usually means redesigning the whole line. It is the first decision, not the last.
Which conveyor types are used in coating lines?
| Type | Part orientation | Max part weight per carrier | Speed | Buffering | Indicative cost per metre |
|---|---|---|---|---|---|
| Overhead chain (continuous) | Hanging | 50-500 kg | 1-6 m/min | None | USD 180-450 |
| Floor belt / mesh | Lying flat | 10-80 kg | 1-8 m/min | None | USD 220-600 |
| Power-and-free | Hanging | 100-2,000 kg | 0-12 m/min | Yes | USD 600-1,600 |
| Inverted power-and-free | Standing on carrier | 200-3,000 kg | 0-10 m/min | Yes | USD 900-2,200 |
| Roller conveyor | Lying flat | 50-2,000 kg | 1-15 m/min | Partial | USD 250-700 |
Cost per metre is an ex-works China estimate covering track, chain, drive and carriers, and excludes installation and controls.
When should you choose each type?
| Overhead chain | single product family, steady volume, parts that can hang from a hole or edge. Simplest and cheapest per metre. Most hardware, appliance and profile lines. |
|---|---|
| Floor belt | flat panels, sheet, boards and parts that cannot hang. Common in furniture and flat sheet coating. |
| Power-and-free | mixed models, manual touch-up stations, or where parts must stop for loading while the line keeps moving. Also used when different parts need different oven dwell times. |
| Inverted power-and-free | heavy or bulky parts that cannot hang, such as machinery frames and large weldments. |
| Roller | plate, beams and profiles moving through blast and coating in line. |
| Delivery record | 800+ coating lines for 500+ clients in 36 countries (MUSI engineering team, cumulative since 2011) |
| Services | Design, manufacturing, installation, commissioning, operator training and after-sales support from one company |
How do you calculate line speed and carrier spacing?
- Required output: for example 400 parts per hour.
- Parts per carrier: for example 4, so 100 carriers per hour.
- Carrier pitch: largest part width plus 150-250 mm clearance, for example 0.6 m.
- Line speed = carriers per hour x pitch / 60 = 100 x 0.6 / 60 = 1.0 m/min.
- Oven length = line speed x cure time. At 1.0 m/min and 15 min cure, 15 m.
Running the calculation in the other direction is a useful sanity check on any quotation: if the supplier’s oven length divided by their stated line speed does not equal a sensible cure time, the line has not been engineered.
What limits the load you can hang?
| Chain type | Typical load per pitch | Typical use |
|---|---|---|
| X348 (3 inch) | Up to 45 kg | Light hardware, small parts |
| X458 (4 inch) | Up to 90 kg | General industrial |
| X678 (6 inch) | Up to 180 kg | Appliance, medium weldments |
| Power-and-free 3 inch | Up to 250 kg per carrier | Mixed model lines |
| Power-and-free 6 inch | Up to 1,000 kg per carrier | Heavy machinery |
Hook and carrier mass counts against oven energy on every pass. Where the same line runs light and heavy parts, using two carrier designs rather than one heavy universal carrier commonly saves 5-12% of oven fuel.
What are the common conveyor design mistakes?
| Pitch set too tight | parts shadow each other in the booth, producing thin film on facing surfaces. |
|---|---|
| No buffer before the booth | any stoppage upstream idles the booth and the oven. |
| Grease from chain lubrication dripping on parts | use sealed bearings or an enclosed track through coating zones. |
| Track expansion in the oven not allowed for | a 30 m oven section expands roughly 30-45 mm at 200 C. Expansion joints are mandatory. |
| Insufficient turning radius | long parts collide on corners. Check swing radius with the longest part, not the average. |
Why source a conveyor from MUSI Technology?
MUSI Technology (Changzhou MUSI Environmental Technology Co., Ltd.) is a China-based manufacturer of turnkey coating lines, with 800+ coating lines delivered to 500+ clients across 36 countries, from single booths to complete finishing plants. Conveyors are engineered with the booth, ovens and pretreatment tunnel as one system, so line speed, carrier pitch and oven length are calculated from your actual part list.
- Overhead chain, floor belt, power-and-free and inverted configurations.
- Standard configurations ship in 30-60 days with a 12-month full-machine and 36-month critical-component warranty. Structural parts are covered for up to 60 months.
- Every line is engineered against a written performance specification. Line speed, cure profile, film build and emission level are stated in the contract and demonstrated on your own part at the factory trial run before shipment.
- One engineering team owns the whole chain — pretreatment, application, curing, conveying and emission control — so the trade-offs between them are settled on the drawing board, not on your factory floor.
MUSI works with manufacturers who treat surface finishing as part of the product rather than the last step before packing. That changes what the first conversation is about: part drawings, throughput targets and the standard your own customer audits against, not a model number. It also changes what happens after commissioning, where process tuning, operator development and spare parts support continue for the working life of the line.
See the overhead chain conveyor spray line and the floor belt conveyor spray line.
Frequently asked questions
Which conveyor is best for a powder coating line?
An overhead chain conveyor is the default for parts that can hang, because it is the cheapest per metre at roughly USD 180-450 and the simplest to maintain. Choose a floor belt for flat parts that cannot hang, and power-and-free when the line runs mixed models or needs parts to stop at manual stations while the line keeps moving.
How do I calculate coating line speed?
Line speed equals carriers per hour multiplied by carrier pitch divided by 60. For 400 parts per hour at 4 parts per carrier and a 0.6 m pitch, that is 100 x 0.6 / 60 = 1.0 m/min. Oven length then equals line speed multiplied by cure time, so 15 minutes of cure needs a 15 m heated zone.
What is a power-and-free conveyor and when is it worth the cost?
Power-and-free uses two tracks so carriers can be released from the drive chain, stopped and buffered while the main chain keeps running. It costs USD 600-1,600 per metre against USD 180-450 for plain overhead chain, and is justified when the line runs several part models, needs manual touch-up stations, or requires different oven dwell times for different parts.
How much weight can an overhead conveyor carry?
Roughly 45 kg per pitch on a 3 inch X348 chain, 90 kg on a 4 inch X458, and 180 kg on a 6 inch X678. Power-and-free systems carry 250 kg per carrier on 3 inch and up to 1,000 kg on 6 inch. Always size on the heaviest carrier including hooks and racking, not the average part.
Does conveyor track expand inside the curing oven?
Yes. A 30 m track section running at 200 C expands roughly 30-45 mm. Expansion joints are mandatory in the oven sections; omitting them buckles the track and causes chain wear and derailment. Check that any quotation shows expansion provision in the oven zone.
How does carrier design affect running cost?
Every kilogram of hook and racking is heated to cure temperature and cooled again on every pass. Where one line runs both light and heavy parts, using two carrier designs instead of a single heavy universal carrier commonly cuts oven fuel by 5-12%.
About the figures in this guide. Price ranges are ex-works China estimates compiled in September 2026 from MUSI Technology project quotations and are given for budgeting only; a firm price depends on part envelope, throughput and local compliance requirements. Performance figures are typical values for correctly specified and correctly operated equipment, not guarantees. Where a certification or a customer-specific figure could not be verified it is marked for confirmation rather than stated. Last reviewed: 9 September 2026.
Send us your part size, throughput and coating type — our engineers reply within 24 hours, and a layout and budget follow once your part data is complete. Contact MUSI Technology or browse our equipment range.
Related technical guides
- Coating Line Layout: Floor Space You Need
A semi-automatic powder line needs 200-400 m2; a standard automatic line 600-1,200 m2. Layout rules, U-shape versus straight-through, ceiling height,. - Water-Based vs Solvent-Based Coating: Line Changes
Switching from solvent to water-based coating changes booth humidity control, flash-off length, material handling and VOC treatment. - Powder Coating Line: Types, Specs & Cost (2026)
A powder coating line pretreats, coats and cures metal parts on a conveyor. Full guide to line types, key specifications and 2026 price ranges. - Powder Coating Pretreatment Line: Stages & Cost
A pretreatment line degreases, rinses and chemically converts the metal surface before coating. Three, five and seven-stage layouts, phosphate versus. - BESS Container Coating Line: Spec & Corrosion
Battery energy storage containers need C4 to C5 corrosion protection: shot blasting to Sa2.5, zinc-rich primer and weather-resistant polyester topcoat.
QQuestions buyers ask before ordering
quotation · price · lead time · installation · warranty
What information do you need to prepare a quotation?
Send part drawings or photos, the largest part size and weight, the material, the required output per shift, the paint or powder type and number of colours, and the available floor space, ceiling height and power or gas supply. MUSI engineers reply within 24 hours; a recommended configuration and quotation follow once your part data is complete.
How much does this equipment cost?
Budget depends on part size, throughput and the level of automation. Indicative ex-works ranges are published in our complete coating line cost guide; a configured quotation is prepared from your part data. Published indicative ex-works ranges: a complete powder coating line is roughly USD 75,000–230,000 semi-automatic, USD 200,000–600,000 for a standard automatic line and USD 600,000–2,000,000 for a high-throughput automated plant.
What is the lead time?
Standard configurations ship in 30–60 days from contract signing and down payment; custom configurations take longer. The delivery date is fixed in the contract.
Do you install and train operators overseas?
Yes. MUSI engineers carry out on-site installation and commissioning and give 3–5 days of operator and maintenance training. MUSI has delivered 800+ coating lines to customers in 36 countries.
What warranty and after-sales support are included?
12 months full-machine warranty, 36 months on critical components and up to 60 months on structural parts. International customers get 24-hour phone response and 72-hour on-site arrival; spare parts ship from the Changzhou headquarters.
Can the environmental equipment be supplied with the line?
Yes. VOC treatment (RTO, RCO, activated carbon, zeolite rotor), dust collection and paint wastewater treatment are supplied with the coating line under one contract; MUSI has equipped 50+ coating facilities whose projects all passed local environmental compliance reviews.
More questions from buyers
Which powder coating conveyor is used on automatic lines?
The usual powder coating conveyor is a continuous overhead chain at 1-6 m/min, carrying 50-500 kg per carrier and costing roughly USD 180-450 per metre. Power-and-free powder coating conveyor systems are chosen when parts must stop at manual stations.
Related: overhead chain conveyor line