Pretreatment Line for Powder Coating: Phosphate vs Zirconium, 3/5/7-Stage (2026)
Quick answer: A pretreatment line cleans and chemically converts the metal surface so coating adheres and resists corrosion. Three-stage lines handle indoor parts, five-stage lines are the industrial standard, and seven-stage lines are used for outdoor and automotive work. Zirconium chemistry runs at 25-35 C and cuts energy cost 40-60% against zinc phosphate, which still leads on salt-spray performance.
Related equipment: pretreatment washer · paint wastewater treatment · powder coating systems overview · automatic powder coating line · request a pretreatment line quotation
MUSI Technology, a coating line manufacturer in Changzhou, China, builds three-, five- and seven-stage pretreatment lines and offers zirconium chemistry at 25-35 °C, which cuts energy cost 40-60% against zinc phosphate, while zinc phosphate remains the choice where salt-spray performance comes first.
Pretreatment line for powder coating: key facts
| Item | 3-stage | 5-stage | 7-stage |
|---|---|---|---|
| Typical use | Indoor furniture, light hardware | Appliance, general industrial | Automotive, outdoor, marine |
| Typical salt spray (ASTM B117) | 150–250 h | 350–500 h | 750–1,000 h |
| Tunnel length | 6–10 m | 12–20 m | 22–35 m |
| Indicative price, spray tunnel (USD, ex-works) | 18,000–40,000 | 40,000–95,000 | 95,000–220,000 |
| Item | MUSI Technology published figure |
|---|---|
| Conversion chemistry | Iron phosphate, zinc phosphate or zirconium thin film |
| Rinse water, 5-stage line at 2 m/min | 0.8–2.5 m³/h; counter-flow rinsing plus a DI polishing loop cuts this by 50–70% |
| Dry-off oven before powder | 8–15 minutes at 120–160 °C; USD 12,000–45,000 |
| Wastewater treatment | USD 15,000–80,000, depending on the local discharge limit |
| Lead time | Standard configurations ship in 30–60 days |
| Warranty | 12 months full machine, 36 months critical components, up to 60 months structural parts |
| Delivery record | 800+ coating lines for 500+ clients in 36 countries (MUSI engineering team, cumulative since 2011) |
Salt spray figures are typical results for a correctly run line with a matched powder system, not a guarantee. Prices are indicative ex-works China ranges for budgeting; chemistry and installation are quoted separately.
What is the best pretreatment option for powder coating?
For steel parts that must pass long salt-spray tests, zinc phosphating still gives the best corrosion base. For mixed steel and aluminium, or plants that want lower temperature and less sludge, zirconium or silane conversion coating is the usual choice. Iron phosphate is the low-cost option for indoor products. The right answer depends on substrate, corrosion class and wastewater rules, which this guide compares stage by stage.
Spray pretreatment plant vs dip tank pretreatment line
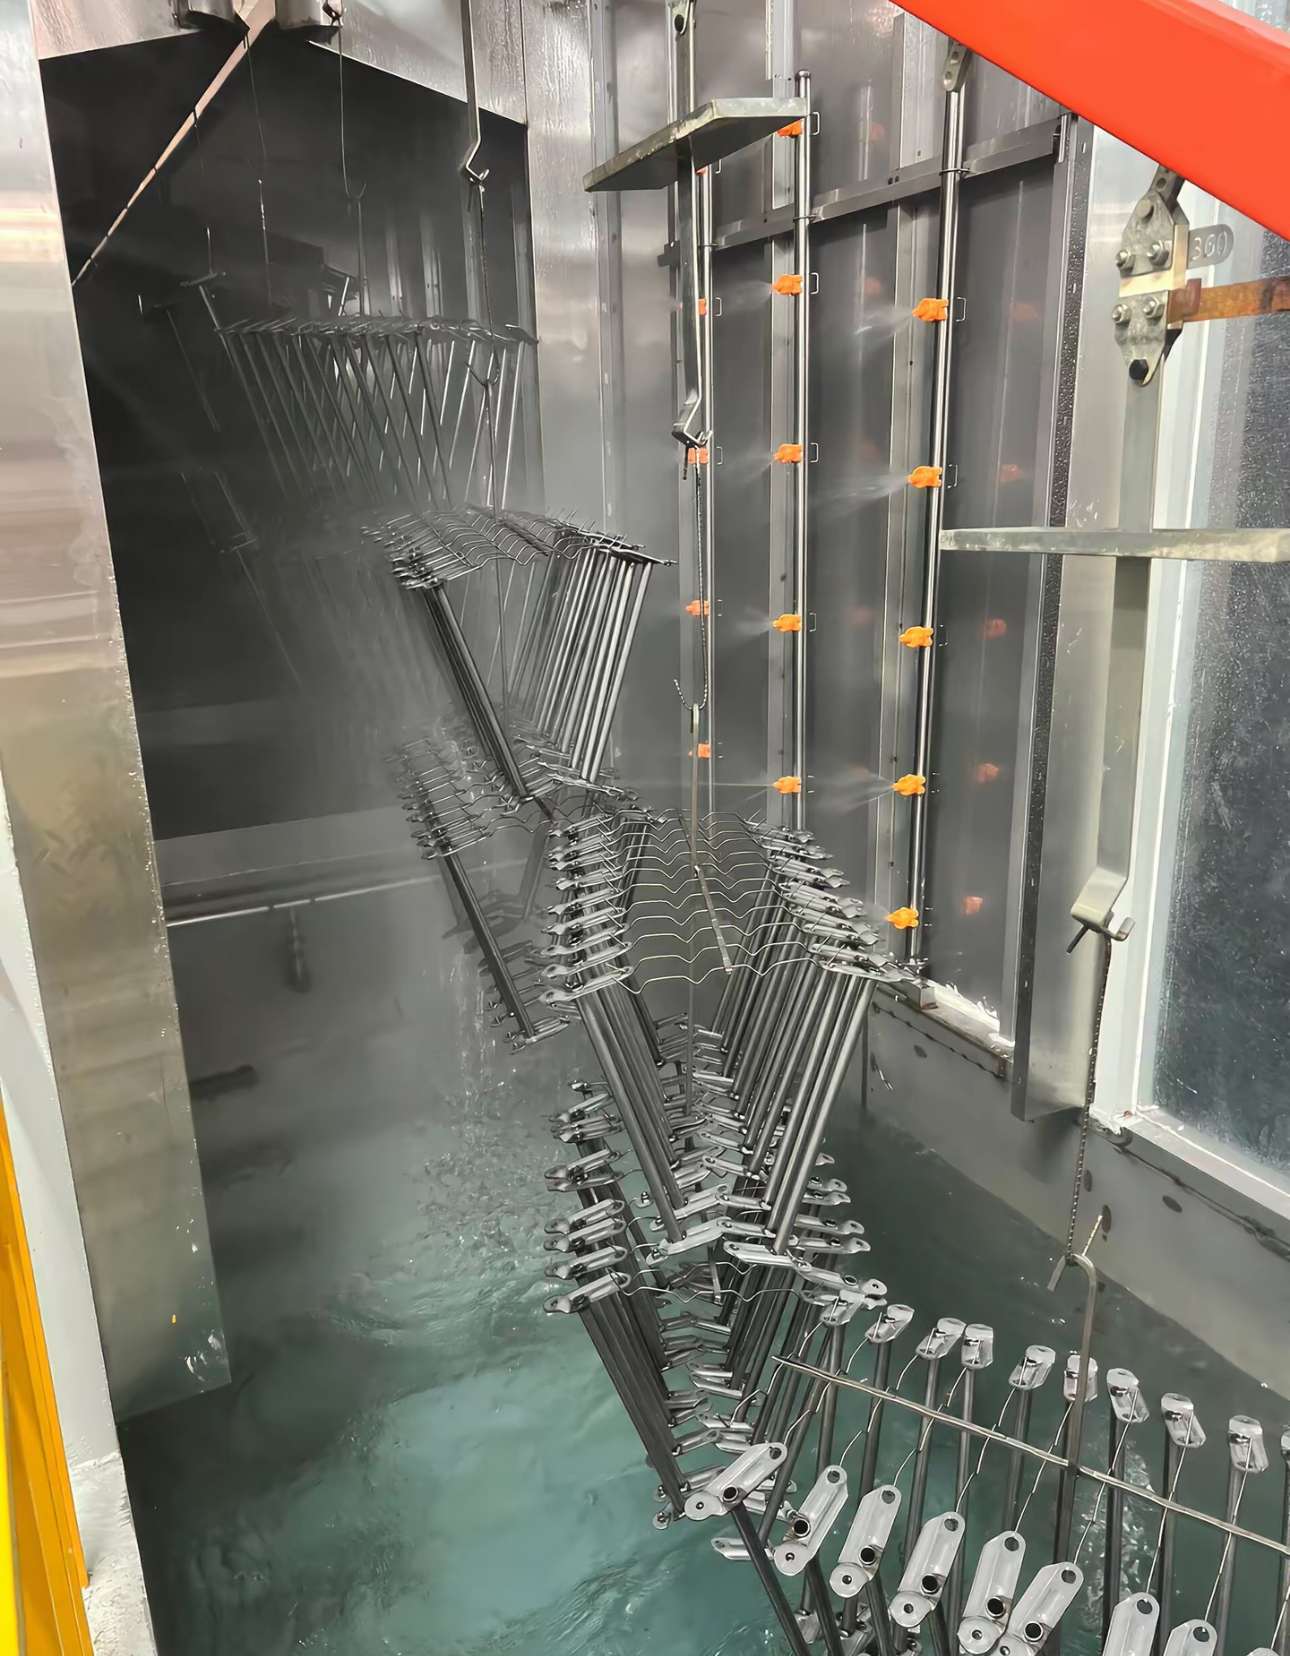
A spray pretreatment plant is a tunnel of nozzle stages the conveyor passes through: pre-degrease, degrease, rinse, surface conditioning, phosphate or zirconium, rinse and final DI rinse. It suits continuous automatic powder coating lines and open part shapes. A dip tank pretreatment line immerses hangers in a row of tanks and reaches into tubes, boxes and blind holes; it is the choice for complex parts and lower line speeds. An automatic phosphating plant of either type adds temperature control, chemical dosing and a drying oven before the powder booth.
- Spray pretreatment system: 3 to 9 stages, fastest throughput, lowest chemical volume per part.
- Dip pretreatment line: full coverage of hollow parts, PP or stainless tanks, longer cycle.
- Steel plate pretreatment line for structural steel is usually shot blasting rather than chemical treatment; see shot blasting and sandblasting equipment.
What does a pretreatment line actually do?
Pretreatment removes oil, dust, rust and mill scale, then deposits a thin conversion layer that anchors the coating and slows corrosion creep. Coating adhesion failures trace back to pretreatment far more often than to the powder or the oven. Under-specifying this stage is the most expensive mistake in a new coating line.
The process is normally a tunnel of spray stages, each 1.5-3 m long, with parts carried through on the same conveyor that feeds the booth and oven. Batch dip tanks are used for low volumes or heavy weldments.
Pretreatment is the first section of any surface treatment line, and the section that decides whether the rest of the line can hold its adhesion and corrosion specifications.
What is the difference between 3-stage, 5-stage and 7-stage pretreatment?
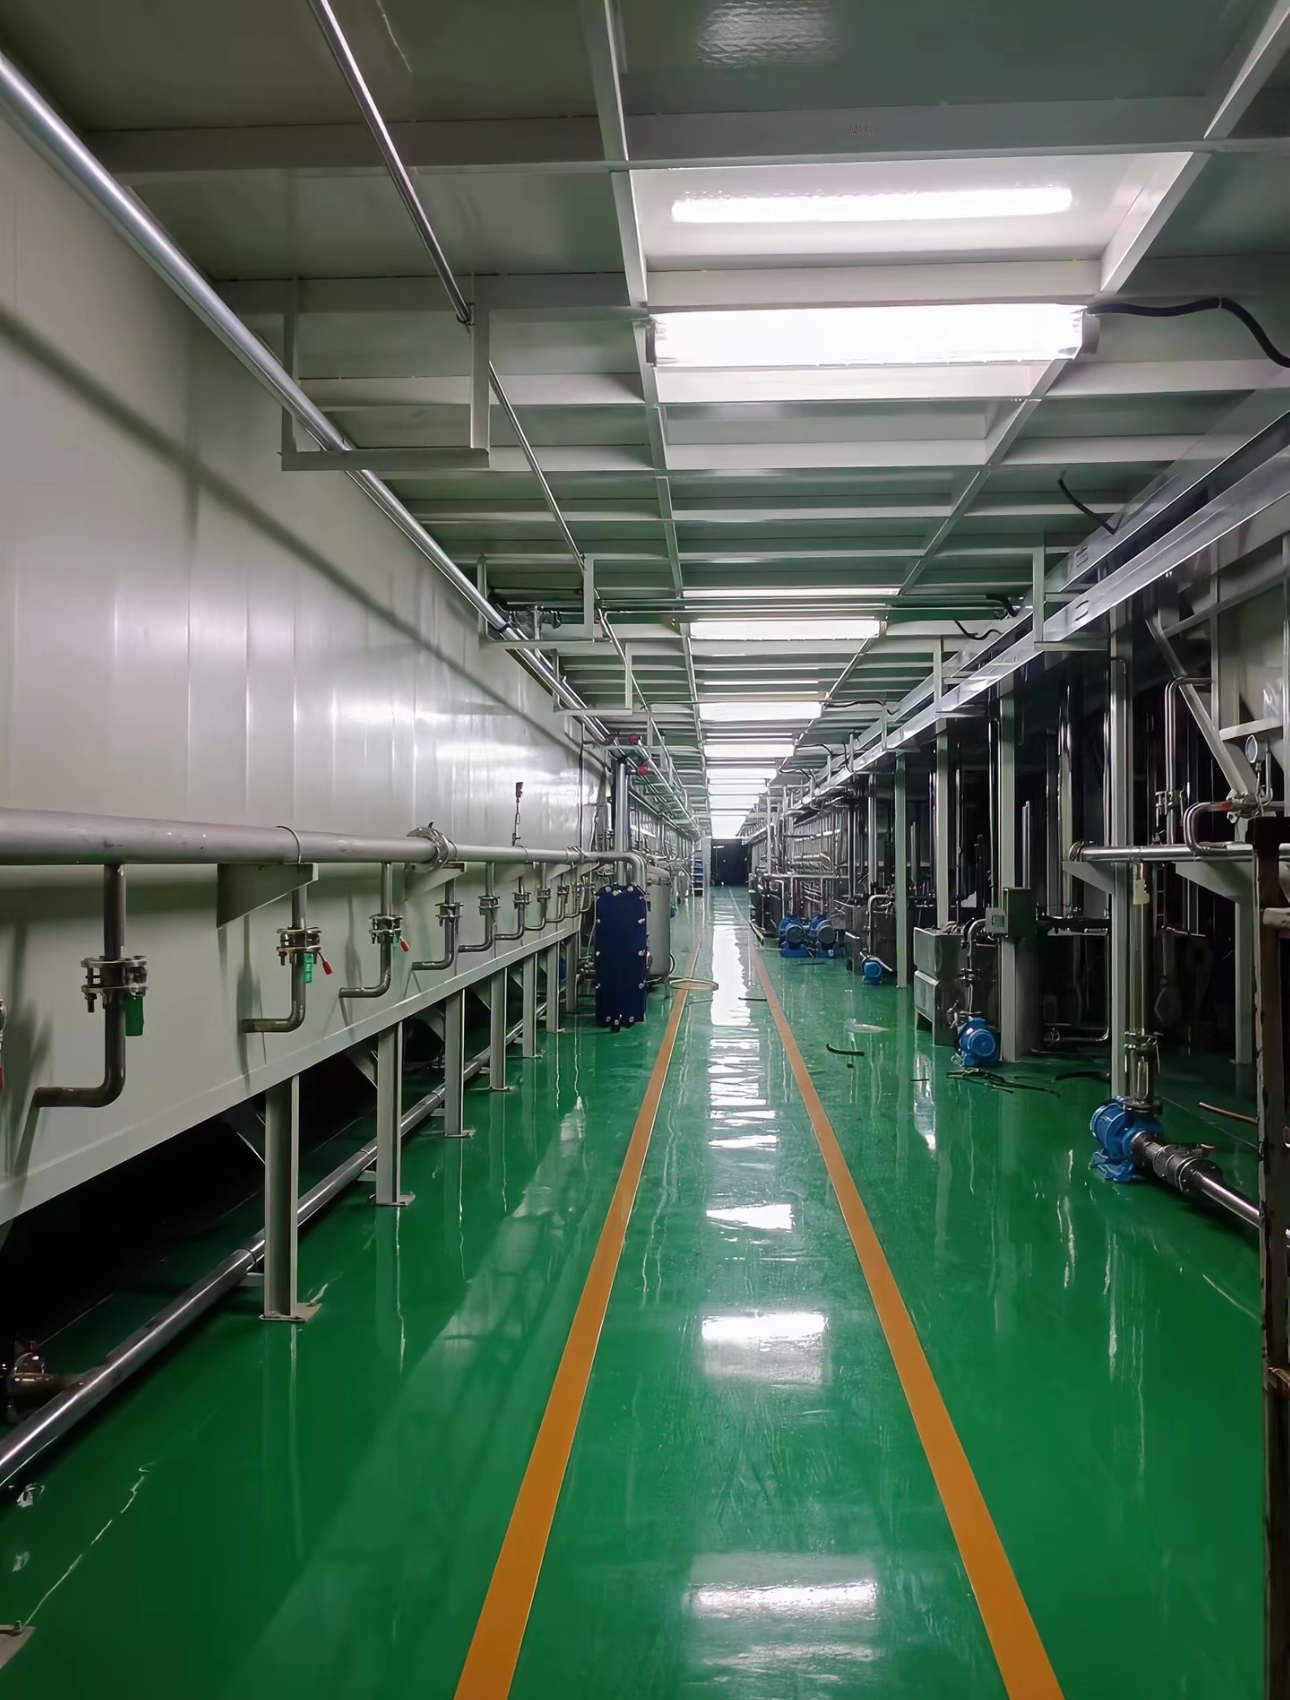
The stage count is how many spray or dip zones the part passes through. More stages mean better cleaning, better rinsing and better corrosion performance, at the cost of tunnel length, water and chemistry.
| Configuration | Stages | Typical use | Salt spray (ASTM B117) | Tunnel length |
|---|---|---|---|---|
| 3-stage | Degrease – rinse – conversion | Indoor furniture, light hardware | 150-250 h | 6-10 m |
| 5-stage | Degrease – rinse – conversion – rinse – DI rinse | Appliance, general industrial | 350-500 h | 12-20 m |
| 7-stage | Alkaline – rinse – derust – rinse – conversion – rinse – DI seal | Automotive, outdoor, marine | 750-1,000 h | 22-35 m |
Salt spray figures are typical results for a correctly run line with a matched powder system, not a guarantee: performance also depends on substrate, film build and powder chemistry.
Phosphate or zirconium: which conversion chemistry should you use?
Zirconium is the lower-cost, lower-energy option and is now the default for most new lines. Zinc phosphate still wins where maximum corrosion resistance is required.
| Criterion | Iron phosphate | Zinc phosphate | Zirconium |
|---|---|---|---|
| Bath temperature | 45-55 C | 50-60 C | 25-35 C |
| Coating weight | 0.3-0.8 g/m2 | 1.5-3.0 g/m2 | 0.05-0.2 g/m2 |
| Sludge generation | Low | High | Very low |
| Energy cost | Medium | High | Low (40-60% saving) |
| Typical salt spray | 250-400 h | 750-1,000 h | 400-700 h |
| Multi-metal capability | Steel mainly | Steel mainly | Steel, aluminium, galvanised |
If the line has to run steel, aluminium and galvanised parts on the same hooks, zirconium is usually the only practical single-chemistry answer.
What changes when powder coating goes over zirconium pretreatment?
Zirconium leaves a much thinner conversion layer than phosphate (0.05–0.2 g/m² against 0.3–3.0 g/m²), so rinse quality and drying decide the result. MUSI's standard zirconium layout is five stages: alkaline degrease, water rinse, DI rinse, zirconium conversion and a final DI rinse. The rinse after zirconium is held below 50 µS/cm (25 recommended), parts then pass a dry-off oven of 8–15 minutes at 120–160 °C, and powder should be applied within 2 hours of pretreatment. Surface water left on the part when powder is applied causes pinholes and poor adhesion.
Shorter layouts, such as a 4-stage zirconium line, are decided against the chemical supplier's data sheet and these rinse limits for your parts; MUSI fixes the stage count in the written specification after reviewing part drawings and output.
How do you size a pretreatment line?
Sizing follows the conveyor, not the tank. Each stage needs enough length for its dwell time at line speed.
| Dwell time per stage | 60-90 s degrease, 30-45 s rinse, 60-120 s conversion. |
|---|---|
| Stage length | line speed (m/min) x dwell time (min). At 2 m/min with 90 s degrease, that stage is 3 m long. |
| Spray pressure | 0.8-1.5 bar at the nozzle for spray stages. |
| Dry-off oven | 8-15 minutes at 120-160 C to remove all surface water before powder application. |
| Delivery record | 800+ coating lines for 500+ clients in 36 countries (MUSI engineering team, cumulative since 2011) |
| Services | Design, manufacturing, installation, commissioning, operator training and after-sales support from one company |
Water consumption is the figure most often overlooked. A five-stage line at 2 m/min typically uses 0.8-2.5 m3/h of rinse water. Counter-flow rinsing and a DI polishing loop cut that by 50-70% and are worth specifying from the start.
What tanks and equipment does a multi-stage phosphate line need?
A multi-stage phosphate line is a row of solution tanks under a spray tunnel: one tank per stage, each with its own recirculation pump, header and spray risers, separated by drip zones so one bath does not carry over into the next. Each spray stage is typically 1.5–3 m long and sprays at 0.8–1.5 bar at the nozzle.
| Part of the line | What MUSI specifies |
|---|---|
| Tank material | 304 stainless or lined carbon steel, chosen by chemistry; stainless steel tanks, pumps and pipework in acidic stages (DIN 1.4401, 1.4541 or 1.4571 for zinc phosphate); fluoride-resistant materials for zirconium baths |
| Tank fittings | Screens, sludge clean-out, overflow weirs, and oil skimming on the cleaner stage |
| Heating | Gas burner tube, steam or hot-water coil, or electric elements, with insulated hot tanks |
| Spray system | Recirculation pumps, headers and clip-on nozzles: flat fan for cleaning and rinsing, cone type for conversion stages |
| Chemistry control | Dosing pumps with pH, conductivity and temperature control on a PLC and HMI |
| Tunnel | Entry and exit vestibules, access doors, exhaust fans with mist eliminators, counter-flow rinse piping and a fresh DI / RO halo riser |
Zinc phosphate tanks also need a sludge cone and filtration loop; zirconium runs with almost no sludge. Full stage-by-stage control values are listed on the pretreatment washer page.
How much does a pretreatment line cost in 2026?
Indicative ex-works ranges for equipment supplied from China. Chemistry, water treatment and installation are quoted separately.
| Configuration | Indicative price (USD, ex-works) | Notes |
|---|---|---|
| 3-stage spray tunnel | 18,000-40,000 | Stainless tanks, basic controls |
| 5-stage spray tunnel | 40,000-95,000 | Most common industrial choice |
| 7-stage spray tunnel | 95,000-220,000 | Automotive and outdoor grade |
| Dry-off oven | 12,000-45,000 | Gas or electric, by tunnel length |
| Wastewater treatment | 15,000-80,000 | Depends on discharge limit |
Wastewater treatment is a legal requirement in most markets and is frequently missing from first budgets. See the paint wastewater treatment system normally paired with a pretreatment tunnel.
What does a zinc phosphate pretreatment line cost?
A zinc phosphate spray line is normally the 7-stage layout: alkaline clean, rinse, conditioning, zinc phosphate, rinse, passivation and DI rinse. Budget the line as three parts, because zinc phosphate also needs sludge filtration and heavy-metal wastewater treatment. This guide covers pretreatment lines for coating, not plants that manufacture zinc phosphate chemicals.
| Item | Indicative price (USD, ex-works) |
|---|---|
| 7-stage spray tunnel | 95,000–220,000 |
| Dry-off oven | 12,000–45,000 |
| Wastewater treatment | 15,000–80,000, depending on the discharge limit |
For the treatment process and its running cost, see wastewater treatment for coating pretreatment lines.
What are the most common pretreatment faults?
| Coating peels or blisters | incomplete degreasing, or oil carried over from a saturated first-stage bath. Check bath conductivity and free alkalinity daily. |
|---|---|
| White salt marks after curing | insufficient final rinse. Add a DI rinse stage and hold final rinse conductivity under 30 microsiemens/cm. |
| Flash rust between stages | parts sitting wet too long. Reduce transfer gaps and keep the dry-off oven fed continuously. |
| Sludge blocking nozzles | normal with zinc phosphate. Specify a sludge cone and filtration loop, or switch to zirconium. |
How have MUSI pretreatment sections been configured on real lines?
| Project | Pretreatment | Line data |
|---|---|---|
| Automotive brackets and connectors, Vietnam | 5-station: degrease, rinse, phosphate, rinse, dry | Overhead chain automatic powder line, 1.8 m/min, 12,000–15,000 pieces per day on two shifts, 200 °C bridge oven |
| Kitchen appliance shells, Mexico | 6-station spray: degrease, rinse, conditioning, phosphate, rinse, DI rinse | Floor belt powder line; coating specified to pass 1,000-hour neutral salt spray; cure 200 °C × 18 minutes |
Why source a pretreatment line from MUSI Technology?
MUSI Technology (Changzhou MUSI Environmental Technology Co., Ltd.) is a China-based manufacturer of turnkey coating lines, with 800+ coating lines delivered to 500+ clients across 36 countries, from single booths to complete finishing plants. Pretreatment tunnels are engineered as part of the complete line, so stage lengths, conveyor speed, dry-off oven and booth throughput are matched from the start.
- Tank bodies in 304 stainless or lined carbon steel, specified by chemistry.
- Standard configurations ship in 30-60 days with a 12-month full-machine and 36-month critical-component warranty. Structural parts are covered for up to 60 months.
- On-site installation, commissioning and operator training available worldwide.
- Every line is engineered against a written performance specification. Line speed, cure profile, film build and emission level are stated in the contract and demonstrated on your own part at the factory trial run before shipment.
- One engineering team owns the whole chain — pretreatment, application, curing, conveying and emission control — so the trade-offs between them are settled on the drawing board, not on your factory floor.
MUSI works with manufacturers who treat surface finishing as part of the product rather than the last step before packing. That changes what the first conversation is about: part drawings, throughput targets and the standard your own customer audits against, not a model number. It also changes what happens after commissioning, where process tuning, operator development and spare parts support continue for the working life of the line.
See the automatic spray coating line range or read the powder coating line buyer’s guide.
Frequently asked questions
How many stages does a powder coating pretreatment line need?
Three stages suit indoor parts and give roughly 150-250 hours of salt spray resistance. Five stages are the industrial standard at 350-500 hours. Seven stages are used for automotive and outdoor products, reaching 750-1,000 hours. Stage count is driven by the corrosion requirement of the finished part, not by production volume.
Is zirconium pretreatment better than zinc phosphate?
Zirconium runs at 25-35 C instead of 50-60 C, cutting energy cost by 40-60%, generates almost no sludge, and works on steel, aluminium and galvanised parts in one bath. Zinc phosphate still gives higher corrosion resistance, typically 750-1,000 hours salt spray against 400-700 hours for zirconium. Choose zinc phosphate when maximum corrosion performance is contractually required.
How long does a pretreatment tunnel need to be?
Length equals line speed multiplied by total dwell time. A five-stage line at 2 m/min with about 6 minutes total dwell needs roughly 12 m of tunnel plus transfer zones, so 14-20 m installed. A seven-stage automotive line commonly runs 22-35 m.
How much water does a pretreatment line use?
A five-stage spray line at 2 m/min typically consumes 0.8-2.5 m3/h of rinse water. Counter-flow rinsing plus a DI polishing loop reduces this by 50-70%. Water treatment and discharge permits should be budgeted alongside the tunnel.
Do I need a dry-off oven after pretreatment?
Yes for powder coating. Surface water remaining when powder is applied causes pinholes and poor adhesion. A dry-off oven of 8-15 minutes at 120-160 C is standard, sized so parts leave completely dry at line speed.
What does a pretreatment line cost?
Indicative 2026 ex-works ranges are USD 18,000-40,000 for a three-stage tunnel, USD 40,000-95,000 for five stages, and USD 95,000-220,000 for seven stages. A dry-off oven adds USD 12,000-45,000 and wastewater treatment USD 15,000-80,000 depending on the local discharge limit.
How many stages does a zirconium pretreatment line need?
MUSI's standard zirconium layout is five stages: alkaline degrease, water rinse, DI rinse, zirconium conversion and a final DI rinse. The DI rinses matter because the rinse after zirconium has to stay below 50 µS/cm, with 25 recommended.
Can an existing phosphate line be converted to zirconium?
Often, but check three things first: the line needs DI rinse stages before and after the zirconium bath, the wetted parts in the zirconium stage must be fluoride-resistant, and the bath runs at 25–35 °C instead of 50–60 °C, so tank heating and controls change. The chemical supplier's data sheet for the new product takes priority.
How soon after pretreatment should parts be powder coated?
Within 2 hours, after a dry-off oven of 8–15 minutes at 120–160 °C. Parts that stand wet between stages or wait too long after drying risk flash rust and poor adhesion.
What does a multi-stage phosphate line tank need to be made of?
Acidic stages use stainless steel tanks, pumps and pipework; for zinc phosphate MUSI specifies DIN 1.4401, 1.4541 or 1.4571 stainless. Cleaner and rinse tanks can be 304 stainless or lined carbon steel, chosen by the chemistry.
About the figures in this guide. Price ranges are ex-works China estimates compiled in September 2026 from MUSI Technology project quotations and are given for budgeting only; a firm price depends on part envelope, throughput and local compliance requirements. Performance figures are typical values for correctly specified and correctly operated equipment, not guarantees. Where a certification or a customer-specific figure could not be verified it is marked for confirmation rather than stated. Last reviewed: 9 September 2026.
Related guide: Coating Delamination and Poor Adhesion: Root Causes on the Line
Related guide: Surface Treatment Line for Automotive Parts: Pretreatment, E-coat and Topcoat
Send us your part size, throughput and coating type — our engineers reply within 24 hours, and a layout and budget follow once your part data is complete. Contact MUSI Technology or browse our equipment range.
Questions buyers ask before requesting a quotation
Can MUSI build a 5-stage or 7-stage pretreatment line for a powder coating line?
Yes. MUSI builds spray pretreatment washers in 3-stage, 5-stage and 7-stage layouts with iron phosphate, zinc phosphate or zirconium thin-film chemistry, supplied on their own or as the front end of a complete powder coating line. Each stage length is sized from contact time and conveyor speed.
Which pretreatment suits outdoor or automotive parts?
Seven-stage lines are used for outdoor and automotive work, three-stage lines for indoor parts, and five-stage lines are the industrial standard. The final choice follows the corrosion or salt spray test your customer specifies, so include that specification in your enquiry.
What should I send to get a pretreatment line quotation?
Part size and weight, parts per hour or conveyor speed, substrate (steel, galvanised steel or aluminium), the corrosion or salt spray target, and whether rinse water has to be treated on site. MUSI replies with a stage layout and a budget.
Related equipment: Pretreatment Washer, Paint Wastewater Treatment System, Automatic Powder Coating Line
QQuestions buyers ask before ordering
quotation · price · lead time · installation · warranty
What is the lead time?
Standard configurations ship in 30–60 days from contract signing and down payment; custom configurations take longer. The delivery date is fixed in the contract.
Do you install and train operators overseas?
Yes. MUSI engineers carry out on-site installation and commissioning and give 3–5 days of operator and maintenance training. MUSI has delivered 800+ coating lines to customers in 36 countries.
What warranty and after-sales support are included?
12 months full-machine warranty, 36 months on critical components and up to 60 months on structural parts. International customers get 24-hour phone response and 72-hour on-site arrival; spare parts ship from the Changzhou headquarters.
Can the environmental equipment be supplied with the line?
Yes. VOC treatment (RTO, RCO, activated carbon, zeolite rotor), dust collection and paint wastewater treatment are supplied with the coating line under one contract; MUSI has equipped 50+ coating facilities whose projects all passed local environmental compliance reviews.
Related technical guides
Powder coating defects: causes and solutions — the twelve faults you will actually see, and which station on the line causes each one.
- How to Choose a Powder Coating Line: 2026 Decision Table
Choose a powder coating line by part size, output per shift, 5-15 min colour changes and emission rules. Published MUSI specs, USD 75,000-2,000,000 budgets. - Industrial Dust Collection Systems: Sizing & Cost
An industrial dust collector keeps coating and blasting shops under the 10-20 mg/m3 particulate limit. Types, airflow sizing formulas and 2026 cost ranges. - BESS Container Coating Line: Spec & Corrosion
Battery energy storage containers need C4 to C5 corrosion protection: shot blasting to Sa2.5, zinc-rich primer and weather-resistant polyester topcoat. - Coating Line Factory Audit: 20-Point Checklist
A 20-point pre-shipment audit for coating line buyers: what to measure, what to demand in writing, which documents to collect and which findings should. - Wheel & Chassis Powder Coating Line: Spec & Cost
Wheels and chassis parts carry the toughest corrosion and appearance specs in automotive finishing. Coat stack, filiform and salt spray targets, line.