Automotive Wheel and Chassis Powder Coating: Spec, Line Design and Cost (2026)
Quick answer: Automotive wheels typically run a three-layer powder stack — primer, base and clear — at 90 to 140 microns, tested to 750 to 1,000 hours salt spray plus a filiform corrosion requirement. Chassis parts run a single functional coat at 60 to 100 microns. A dedicated wheel line costs USD 600,000 to 1,600,000; a chassis line USD 400,000 to 900,000.
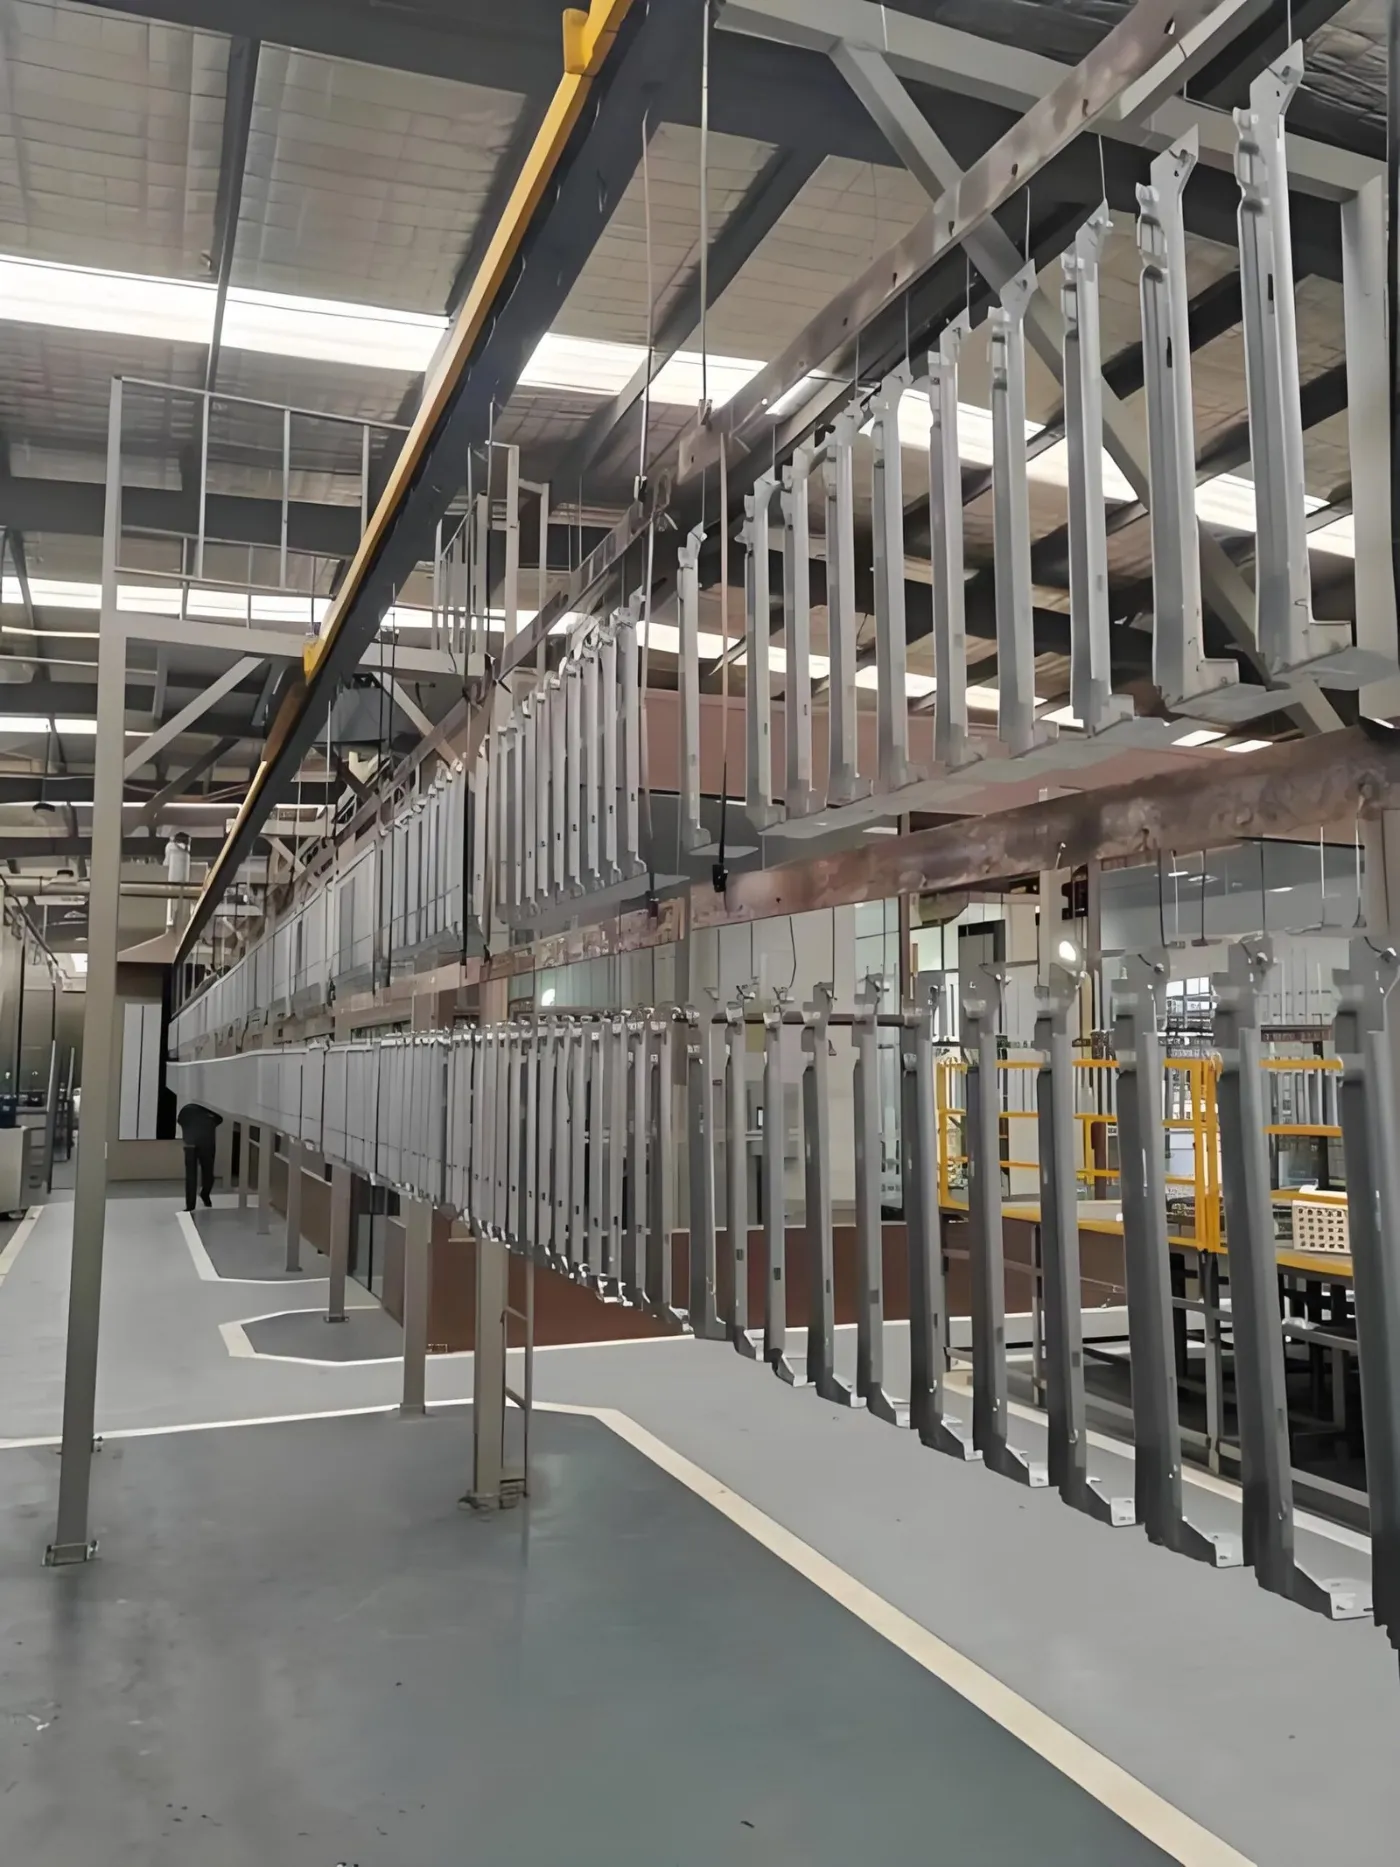
Why wheels and chassis parts are specified separately
They fail differently. A chassis bracket fails by general corrosion after years of road salt, so the specification is about barrier thickness and pretreatment quality. A wheel fails cosmetically first — filiform corrosion creeping from a stone chip, or clear coat yellowing — while sitting in full view of the customer.
That difference drives coat count. Chassis parts get one functional coat. Wheels get a stack, because no single layer delivers adhesion, barrier, colour and UV resistance at once.
What does the coat stack look like?
| Part group | Coat stack | Total film | Corrosion target |
|---|---|---|---|
| Alloy wheel, painted finish | Powder primer, powder base, powder clear | 90-140 microns | 750-1,000 h plus filiform |
| Alloy wheel, machined face | Powder primer, base, diamond cut, clear | 100-160 microns | 750-1,000 h plus filiform |
| Steel wheel | Powder primer plus topcoat | 70-110 microns | 500-750 h |
| Chassis bracket, subframe | Single epoxy or hybrid powder | 60-100 microns | 500-1,000 h |
| Suspension spring | Zinc flake or epoxy powder | 15-80 microns | 480-720 h |
Filiform corrosion is the specification most often missed by suppliers coming from general industrial work. It is tested separately from salt spray, it is driven by pretreatment quality on aluminium rather than by film thickness, and adding more topcoat does not fix a filiform failure.
What pretreatment do these parts need?
| Alloy wheels | chrome-free zirconium or titanium conversion, with a controlled etch of 0.5-2 g/m2. Etch weight is the primary filiform control. |
|---|---|
| Steel chassis parts | seven-stage with zinc phosphate where 750 h or more is required, zirconium where the line also runs aluminium. |
| Final rinse | deionised, conductivity under 30 microsiemens/cm. Residual salts under the film are a direct filiform initiator. |
| Dry-off | 10-15 min at 100-120 C for aluminium; higher for steel. |
| Delivery record | 800+ coating lines for 500+ clients in 36 countries (MUSI engineering team, cumulative since 2011) |
| Services | Design, manufacturing, installation, commissioning, operator training and after-sales support from one company |
Our pretreatment line guide covers the phosphate versus zirconium decision in detail.
How is a wheel line laid out?
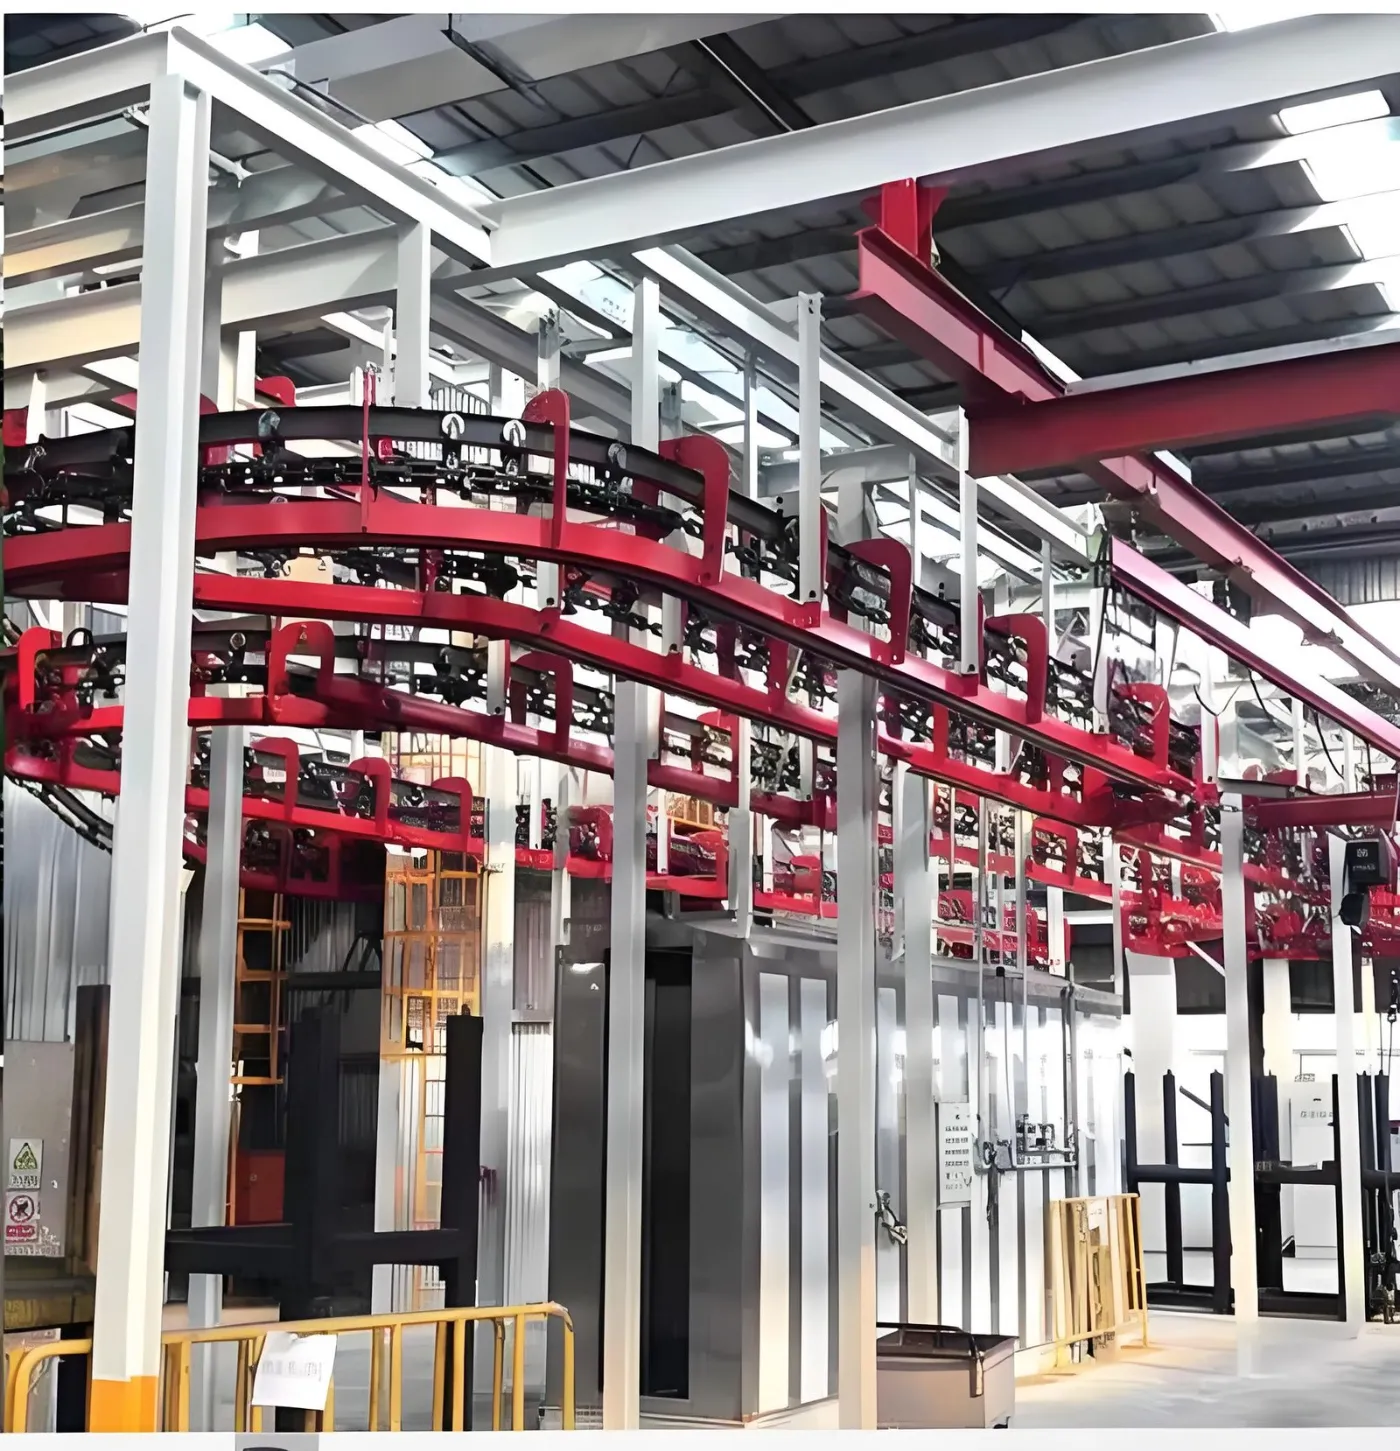
- Load onto dedicated wheel jigs — never free-hanging hooks, because swing destroys film uniformity on a curved face.
- Seven-stage pretreatment with etch control and DI final rinse.
- Dry-off oven.
- Primer booth, then gel or full cure depending on the powder system.
- Base coat booth with robots or reciprocators, colour-change capable.
- Optional diamond-cut machining cell for machined-face wheels.
- Clear coat booth in a controlled-cleanliness area.
- Final cure oven with part metal temperature logging.
- Cooling, film measurement and 100 percent visual inspection.
| Programme | Wheels per hour | Line speed | Booths |
|---|---|---|---|
| Aftermarket, mixed sizes | 60-150 | 1.0-2.0 m/min | 2 |
| OEM supply, single family | 150-400 | 2.0-3.5 m/min | 3 |
| High volume, machined face | 400-700 | 3.0-5.0 m/min | 3 plus machining cell |
What does film control require in practice?
Wheel geometry is hostile to electrostatics: deep spoke recesses, a rim well that shadows itself, and a machined face that must stay dimensionally exact. Four controls do most of the work.
- Fixed jigs that present the wheel at a defined angle and rotate it under the guns.
- Voltage staging: lower kV of 40-60 for recesses, higher for flat faces, programmed per zone.
- Earthing discipline: jig contact resistance under 1 megohm, verified every shift.
- Measurement at defined points: rim flange, spoke root, hub face and back face, logged per batch.
What does the line cost in 2026?
| Configuration | Indicative price (USD, ex-works) |
|---|---|
| Chassis parts line, 7-stage, single booth | 400,000-700,000 |
| Chassis line with robot cell and full logging | 700,000-900,000 |
| Wheel line, two booths, aftermarket volume | 600,000-1,000,000 |
| Wheel line, three booths, OEM volume | 1,000,000-1,600,000 |
| Add: diamond-cut machining cell | 180,000-450,000 |
Working with MUSI Technology on an automotive line
MUSI Technology (Changzhou MUSI Environmental Technology Co., Ltd.) designs and builds turnkey finishing lines from its plant in Changzhou, China, with 800+ coating lines delivered to 500+ clients across 36 countries, from single booths to complete finishing plants.
- Every line is engineered against a written performance specification. Line speed, cure profile, film build at named measurement points and corrosion target are stated in the contract and demonstrated on your own part at the factory trial run before shipment.
- One engineering team owns the whole chain — pretreatment chemistry, jig design, application, curing, conveying and emission control — so the trade-offs between them are settled on the drawing board, not on your factory floor.
- Control panels are specified with film thickness, cure and bath logging from the start, so the evidence your customer audits exists from day one rather than being retrofitted.
Send your part drawings, annual volume and the customer specification you have to meet: contact MUSI Technology. See also automotive parts coating solutions and the wheel hub powder coating line case study.
Frequently asked questions
What coating stack do alloy wheels use?
A three-layer powder stack of primer, base and clear totalling 90-140 microns for painted finishes, or primer, base, diamond-cut machining and clear at 100-160 microns for machined-face wheels. No single layer delivers adhesion, barrier, colour and UV resistance at once, which is why wheels get a stack while chassis parts get one functional coat.
What is filiform corrosion and why does it matter on wheels?
Filiform corrosion is thread-like creep that spreads under the coating from a stone chip or edge, and it is tested separately from salt spray. On aluminium wheels it is driven by pretreatment quality rather than film thickness, so adding topcoat does not fix a filiform failure. Etch weight of 0.5-2 g/m2 and a deionised final rinse below 30 microsiemens/cm are the primary controls.
How many hours of salt spray do wheels and chassis parts need?
Alloy wheels typically require 750-1,000 hours plus a separate filiform requirement, steel wheels 500-750 hours, chassis brackets and subframes 500-1,000 hours, and suspension springs 480-720 hours. The customer part specification always overrides these generic figures.
Why do wheels need fixed jigs rather than hooks?
Because wheel geometry is hostile to electrostatic application: deep spoke recesses, a self-shadowing rim well and a machined face that must stay dimensionally exact. A free-hanging hook lets the part swing, changing gun distance continuously and destroying film uniformity on curved faces. Fixed jigs present the wheel at a defined angle and rotate it under the guns.
What throughput does a wheel coating line achieve?
Aftermarket lines running mixed sizes typically produce 60-150 wheels per hour at 1.0-2.0 m/min with two booths. OEM lines on a single wheel family reach 150-400 per hour at 2.0-3.5 m/min with three booths. High-volume machined-face lines reach 400-700 per hour with three booths plus a dedicated diamond-cut machining cell.
What does an automotive wheel or chassis coating line cost?
Indicative 2026 ex-works ranges are USD 400,000-700,000 for a chassis parts line with seven-stage pretreatment and a single booth, USD 700,000-900,000 with a robot cell and full logging, USD 600,000-1,000,000 for a two-booth aftermarket wheel line, and USD 1,000,000-1,600,000 for a three-booth OEM wheel line. A diamond-cut machining cell adds USD 180,000-450,000.
About the figures in this guide. Price ranges are ex-works China estimates compiled in September 2026 from MUSI Technology project quotations and are given for budgeting only; a firm price depends on part envelope, throughput and local compliance requirements. Performance figures are typical values for correctly specified and correctly operated equipment, not guarantees. Last reviewed: 10 September 2026.
Send us your part size, throughput and coating type — our engineers reply within 24 hours, and a layout and budget follow once your part data is complete. Contact MUSI Technology or browse our equipment range.
Further Reading
- ProductsAutomotive Coating Line
Robotic Flexible Coating Line - IndustryAutomotive Parts Coating
- Technical guidesCoating Line for Automotive Parts: Requirements, Layout and Throughput (2026)
Robotic Spray Painting vs Reciprocator: When Does a Robot Pay Off? (2026) - Case StudiesAutomotive Parts Coating Line for Tier-1 Supplier
Automotive Bumper Robotic Coating
Automotive Wheel Hub Powder Coating Line
Automotive Interior UV Curing Line - NewsRobotic Spray Painting in the Automotive Industry: A Practical Guide
QQuestions buyers ask before ordering
quotation · price · lead time · installation · warranty
What information do you need to prepare a quotation?
Send part drawings or photos, the largest part size and weight, the material, the required output per shift, the paint or powder type and number of colours, and the available floor space, ceiling height and power or gas supply. MUSI engineers reply within 24 hours; a recommended configuration and quotation follow once your part data is complete.
How much does this equipment cost?
Budget depends on part size, throughput and the level of automation. Indicative ex-works ranges are published in our powder coating line guide (indicative ex-works budgets from USD 75,000 to 2,000,000); a configured quotation is prepared from your part data.
What is the lead time?
Standard configurations ship in 30–60 days from contract signing and down payment; custom configurations take longer. The delivery date is fixed in the contract.
Do you install and train operators overseas?
Yes. MUSI engineers carry out on-site installation and commissioning and give 3–5 days of operator and maintenance training. MUSI has delivered 800+ coating lines to customers in 36 countries.
What warranty and after-sales support are included?
12 months full-machine warranty, 36 months on critical components and up to 60 months on structural parts. International customers get 24-hour phone response and 72-hour on-site arrival; spare parts ship from the Changzhou headquarters.
Can the environmental equipment be supplied with the line?
Yes. VOC treatment (RTO, RCO, activated carbon, zeolite rotor), dust collection and paint wastewater treatment are supplied with the coating line under one contract; MUSI has equipped 50+ coating facilities whose projects all passed local environmental compliance reviews.