Aluminium Profile Powder Coating Line: Vertical vs Horizontal (2026)
Quick answer: A vertical aluminium profile coating line hangs 6-7 m extrusions upright, giving even film build, minimal handling marks and a footprint roughly 40-60% smaller than an equivalent horizontal line. Horizontal lines cost 30-50% less and suit profiles under 6 m or mixed part shapes. Both require chromate-free pretreatment to meet Qualicoat class specifications.
Related equipment: vertical powder coating line · horizontal automatic powder coating line · powder coating systems overview · aluminium profile coating lines · installation and commissioning
Why is aluminium profile coating a special case?
Extruded profiles are long, thin and light. Three problems follow: they bow under their own weight when carried horizontally, they mark easily where hooks touch, and their thin walls heat and cool much faster than the steel racking around them. Line design has to answer all three.
Aluminium also needs its own pretreatment chemistry. Iron and zinc phosphate developed for steel are not suitable; chrome-free titanium or zirconium conversion is now the standard for architectural work.
Vertical or horizontal: which line should you build?
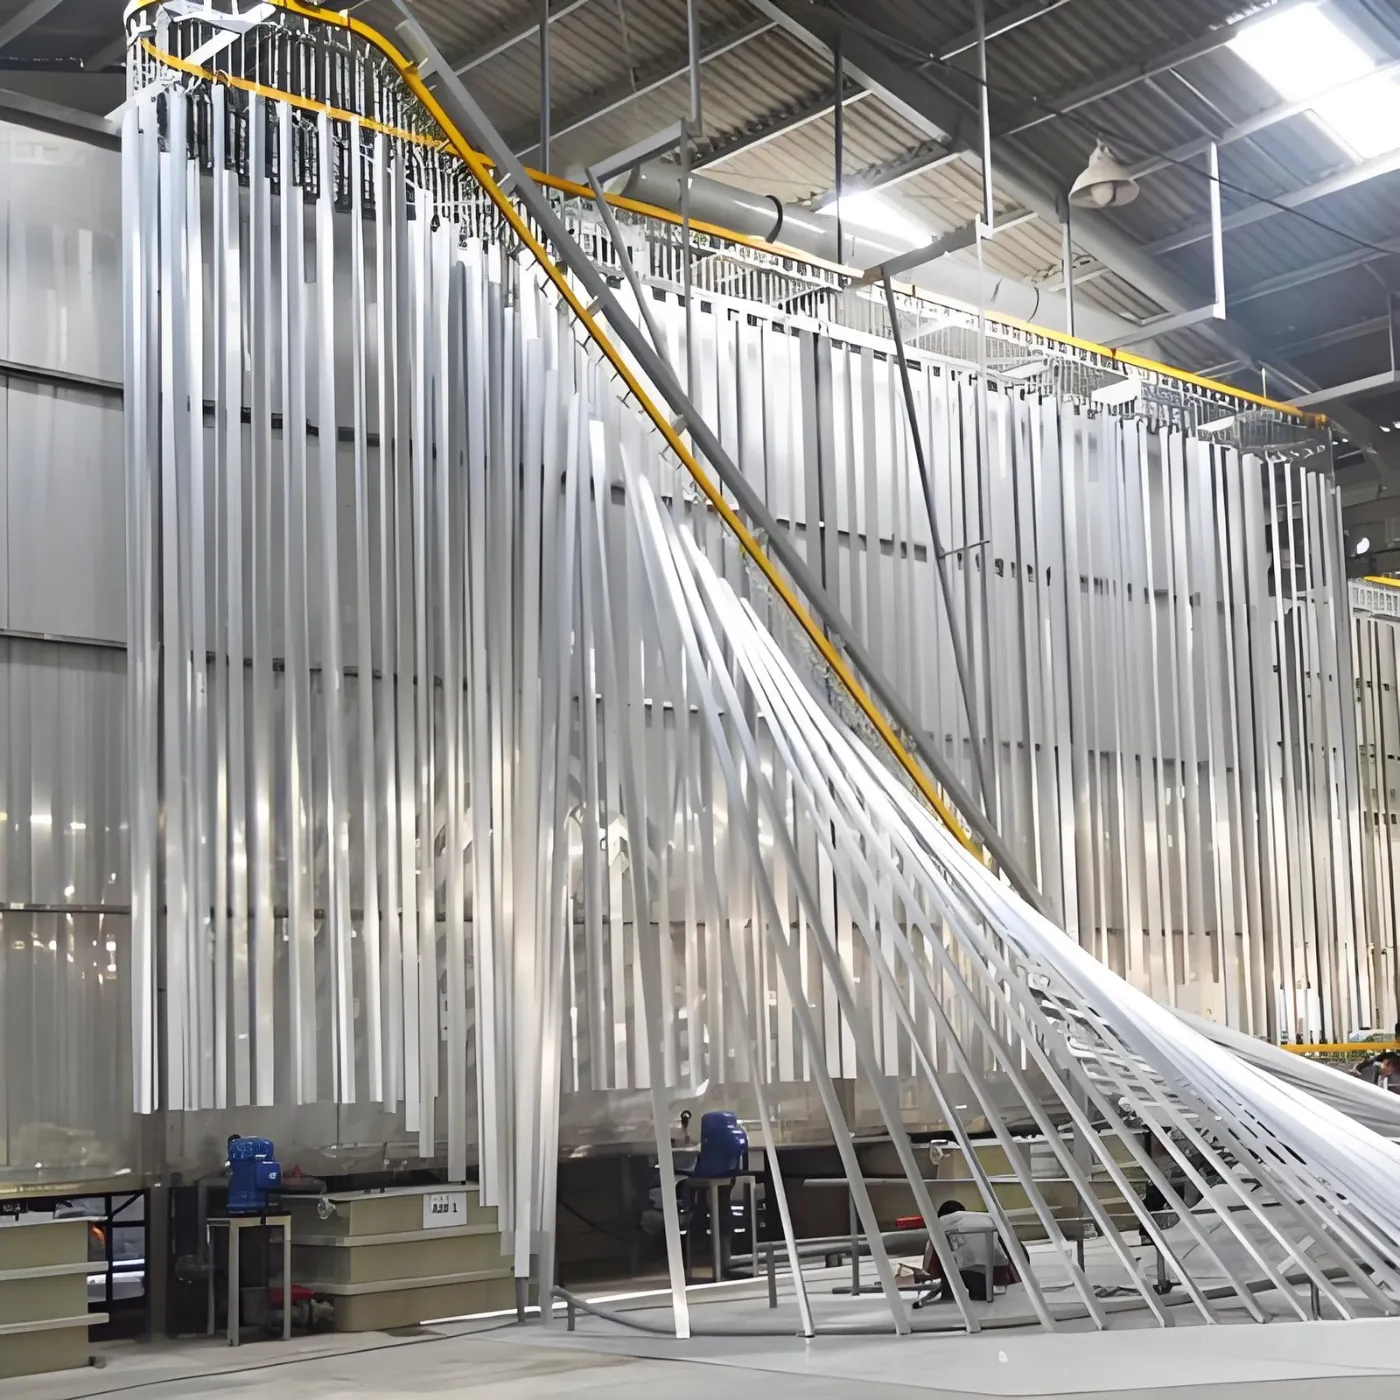
| Criterion | Vertical line | Horizontal line |
|---|---|---|
| Maximum profile length | 6-7.5 m | 6 m typical |
| Footprint for equal output | 40-60% smaller | Larger |
| Handling marks | Minimal, one hanging point | More contact points |
| Film uniformity | High | Medium |
| Indicative price | USD 350,000-1,200,000 | USD 180,000-600,000 |
| Building height needed | 10-14 m | 6-8 m |
| Best for | Architectural profile, high volume | Mixed parts, shorter profiles |
Building height is usually the deciding constraint. A vertical line needs 10-14 m of clear internal height; if the building cannot provide it, the choice is made for you.
What throughput can each configuration reach?
| Configuration | Line speed | Typical output | Colour change |
|---|---|---|---|
| Vertical, single booth | 1.2-2.5 m/min | 400-900 m2/h | 15-25 min |
| Vertical, twin booth | 1.2-2.5 m/min | 700-1,500 m2/h | Under 10 min alternating |
| Horizontal, single booth | 1.5-3.5 m/min | 250-600 m2/h | 15-30 min |
What pretreatment does aluminium need?
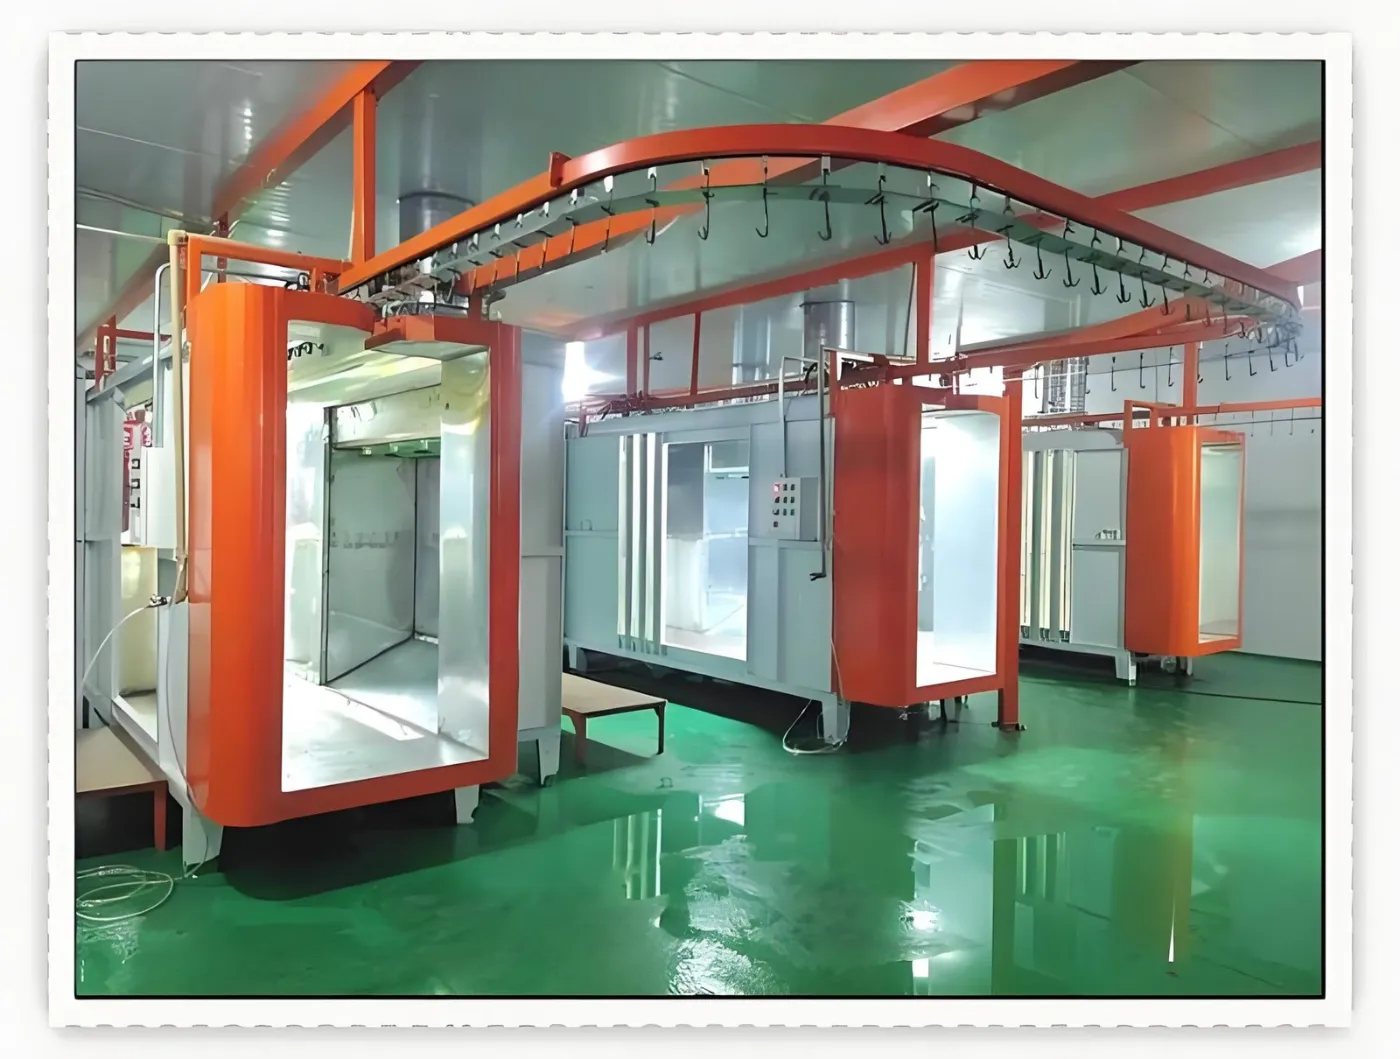
Architectural aluminium normally uses a chrome-free multi-stage process: alkaline degrease, rinse, acid etch, rinse, titanium or zirconium conversion, rinse, and deionised final rinse. Etch weight of 1-3 g/m2 is the usual target.
| Degrease | mildly alkaline, 50-60 C, 90-120 s. |
|---|---|
| Etch | acid or alkaline, removes 1-3 g/m2 of surface aluminium. |
| Conversion | chrome-free Ti/Zr, 25-35 C, 60-90 s. |
| Final DI rinse | conductivity under 30 microsiemens/cm. |
| Dry-off | 10-15 min at 100-120 C, lower than steel to avoid soft-coat issues. |
| Delivery record | 800+ coating lines for 500+ clients in 36 countries (MUSI engineering team, cumulative since 2011) |
| Services | Design, manufacturing, installation, commissioning, operator training and after-sales support from one company |
Where a Qualicoat or similar class approval is required, the pretreatment chemistry, powder and process parameters all have to come from an approved combination. Check the current Qualicoat specification before finalising chemistry.
Anodising or powder coating, and can one plant run both?
They are different processes, not competing brands of the same thing. Anodising is electrochemical: the aluminium surface is converted into a hard oxide layer that is part of the metal. Powder coating lays an organic film on top of a conversion coating. Anodising gives natural, bronze and metallic finishes with very high abrasion resistance and no colour drift; powder gives the full RAL range, wood-grain effects and a lower cost per square metre.
Plenty of architectural profile plants run both, and the search for a vertical anodizing and powder coating plant usually means exactly that: two lines under one roof. What they share is the extrusion handling — racking, vertical hanging, 6-7 m bar lengths, the same loading and unloading bays. What they do not share is almost everything else. Anodising needs rectifiers, acid and alkaline tank lines, cooling and sealing stages. Powder needs a spray booth, powder recovery, a curing oven and extraction. The two lines normally run parallel rather than in series, with shared loading, shared compressed air and, most usefully, shared wastewater treatment, because both processes produce effluent that has to be treated before discharge.
One practical layout note: the anodising line sets the building height, because the tanks and the hoist above them are taller than a powder booth. If a plant is being designed for both from the start, set the crane height for anodising first and fit the vertical powder coating line into that envelope, not the other way round.
MUSI Technology quotes the powder coating half of such a plant — pretreatment, vertical or horizontal powder line, curing, powder recovery, extraction and wastewater treatment. If the anodising line is in the same project, say so at enquiry stage so the scope split and the shared utilities are agreed before layout drawings start.
What about wood-grain transfer finishes?
Wood effect is produced by sublimation transfer after powder coating: the profile is wrapped in printed film or passed through a transfer machine, then held at 180-200 C for 3-8 minutes so the ink migrates into the powder film. It adds a transfer oven and a wrapping or vacuum station to the line, typically USD 30,000-120,000.
Powder for wood-grain work must be a transfer-compatible polyester; standard architectural powders do not accept the ink evenly.
What does an aluminium profile coating line cost in 2026?
| Item | Indicative price (USD, ex-works) |
|---|---|
| Horizontal line, 6 m profiles, single booth | 180,000-600,000 |
| Vertical line, 6.5 m profiles, single booth | 350,000-800,000 |
| Vertical line, twin booth, high output | 800,000-1,200,000 |
| Wood-grain transfer station and oven | 30,000-120,000 |
| Chrome-free pretreatment tunnel | 60,000-180,000 |
Estimates are ex-works China for budgeting. Building height, local emission limits and Qualicoat requirements move these figures significantly.
Why source an aluminium coating line from MUSI Technology?
MUSI Technology (Changzhou MUSI Environmental Technology Co., Ltd.) is a China-based manufacturer of turnkey coating lines, with 800+ coating lines delivered to 500+ clients across 36 countries, including aluminium extrusion coating plants.
- Vertical and horizontal configurations engineered to your profile length and building height.
- Chrome-free pretreatment tunnels and optional wood-grain transfer stations.
- Standard configurations ship in 30-60 days with a 12-month full-machine and 36-month critical-component warranty. Structural parts are covered for up to 60 months.
- Every line is engineered against a written performance specification. Line speed, cure profile, film build and emission level are stated in the contract and demonstrated on your own part at the factory trial run before shipment.
- One engineering team owns the whole chain — pretreatment, application, curing, conveying and emission control — so the trade-offs between them are settled on the drawing board, not on your factory floor.
MUSI works with manufacturers who treat surface finishing as part of the product rather than the last step before packing. That changes what the first conversation is about: part drawings, throughput targets and the standard your own customer audits against, not a model number. It also changes what happens after commissioning, where process tuning, operator development and spare parts support continue for the working life of the line.
See the vertical powder coating system and the aluminium profile coating solutions.
Frequently asked questions
Is a vertical or horizontal aluminium coating line better?
Vertical lines hang profiles upright, giving more even film build, fewer handling marks and a footprint 40-60% smaller for the same output, but they need 10-14 m of clear building height and cost 30-50% more. Horizontal lines are cheaper, fit lower buildings and handle mixed part shapes, at the cost of more contact marks and larger floor area.
What building height does a vertical aluminium coating line need?
Between 10 and 14 m of clear internal height for 6-7 m profiles, allowing for hanging gear, conveyor and oven structure above the profile. Building height is usually the constraint that decides between vertical and horizontal, so confirm it before specifying anything else.
What pretreatment does aluminium profile need before powder coating?
A chrome-free multi-stage process: alkaline degrease at 50-60 C, rinse, acid or alkaline etch removing 1-3 g/m2, rinse, titanium or zirconium conversion at 25-35 C, rinse, and a deionised final rinse below 30 microsiemens/cm. Steel phosphate chemistry is not suitable for aluminium.
What throughput can an aluminium profile line reach?
A vertical line with one booth typically produces 400-900 m2/h at 1.2-2.5 m/min. Twin-booth vertical lines reach 700-1,500 m2/h and allow near-continuous colour change. Horizontal single-booth lines produce 250-600 m2/h.
How is a wood-grain aluminium finish produced?
By sublimation transfer after powder coating. The coated profile is wrapped in printed film or passed through a transfer machine, then held at 180-200 C for 3-8 minutes so the ink migrates into the powder film. It requires a transfer-compatible polyester powder and adds a transfer oven costing USD 30,000-120,000.
What does an aluminium profile coating line cost?
Indicative 2026 ex-works ranges are USD 180,000-600,000 for a horizontal line, USD 350,000-800,000 for a single-booth vertical line, and USD 800,000-1,200,000 for a twin-booth high-output vertical line. A chrome-free pretreatment tunnel adds USD 60,000-180,000.
About the figures in this guide. Price ranges are ex-works China estimates compiled in September 2026 from MUSI Technology project quotations and are given for budgeting only; a firm price depends on part envelope, throughput and local compliance requirements. Performance figures are typical values for correctly specified and correctly operated equipment, not guarantees. Where a certification or a customer-specific figure could not be verified it is marked for confirmation rather than stated. Last reviewed: 9 September 2026.
Send us your part size, throughput and coating type — our engineers reply within 24 hours, and a layout and budget follow once your part data is complete. Contact MUSI Technology or browse our equipment range.
What to send for a quotation: part drawings or photos, the largest part size and weight, the material, the required output per shift and cycle time, the coating type (powder, liquid, UV or 2K) and the number of colours, and the available floor space, ceiling height, power or gas supply and local emission requirements.
Related technical guides
Powder coating defects: causes and solutions — the twelve faults you will actually see, and which station on the line causes each one.
- Sandblasting & Shot Peening Equipment Guide 2026
Compare rotary table, hook type, tumble belt and roller conveyor blast machines: working principle, specifications, applications and cost ranges. - Importing a Coating Line from China: Full Guide
What it takes to import a spray coating line from China: container count, Incoterms, typical payment terms, customs codes, installation time on site and. - Coating Line Layout: Floor Space You Need
A semi-automatic powder line needs 200-400 m2; a standard automatic line 600-1,200 m2. Layout rules, U-shape versus straight-through, ceiling height,. - Water-Based vs Solvent-Based Coating: Line Changes
Switching from solvent to water-based coating changes booth humidity control, flash-off length, material handling and VOC treatment. - Powder Coating Line: Types, Specs & Cost (2026)
A powder coating line pretreats, coats and cures metal parts on a conveyor. Full guide to line types, key specifications and 2026 price ranges.
QQuestions buyers ask before ordering
quotation · price · lead time · installation · warranty
What is the lead time?
Standard configurations ship in 30–60 days from contract signing and down payment; custom configurations take longer. The delivery date is fixed in the contract.
Do you install and train operators overseas?
Yes. MUSI engineers carry out on-site installation and commissioning and give 3–5 days of operator and maintenance training. MUSI has delivered 800+ coating lines to customers in 36 countries.
What warranty and after-sales support are included?
12 months full-machine warranty, 36 months on critical components and up to 60 months on structural parts. International customers get 24-hour phone response and 72-hour on-site arrival; spare parts ship from the Changzhou headquarters.
Can the environmental equipment be supplied with the line?
Yes. VOC treatment (RTO, RCO, activated carbon, zeolite rotor), dust collection and paint wastewater treatment are supplied with the coating line under one contract; MUSI has equipped 50+ coating facilities whose projects all passed local environmental compliance reviews.
More questions from buyers
When is horizontal powder coating the better choice?
Horizontal powder coating is the better choice when the building is lower than 10-14 m clear height, when the line also coats mixed part shapes, or when the budget is limited: a horizontal line for 6 m profiles costs about USD 180,000-600,000 against USD 350,000-800,000 for a vertical line. Output is 250-600 m2 per hour on a single booth.
Are vertical lines used for aluminium extrusions?
Yes. Vertical lines are the standard for aluminium extrusions in volume: profiles of 6-7.5 m hang upright from one point, which removes bow and hook marks and gives 400-900 m2 per hour on a single booth.
Related: vertical powder coating line