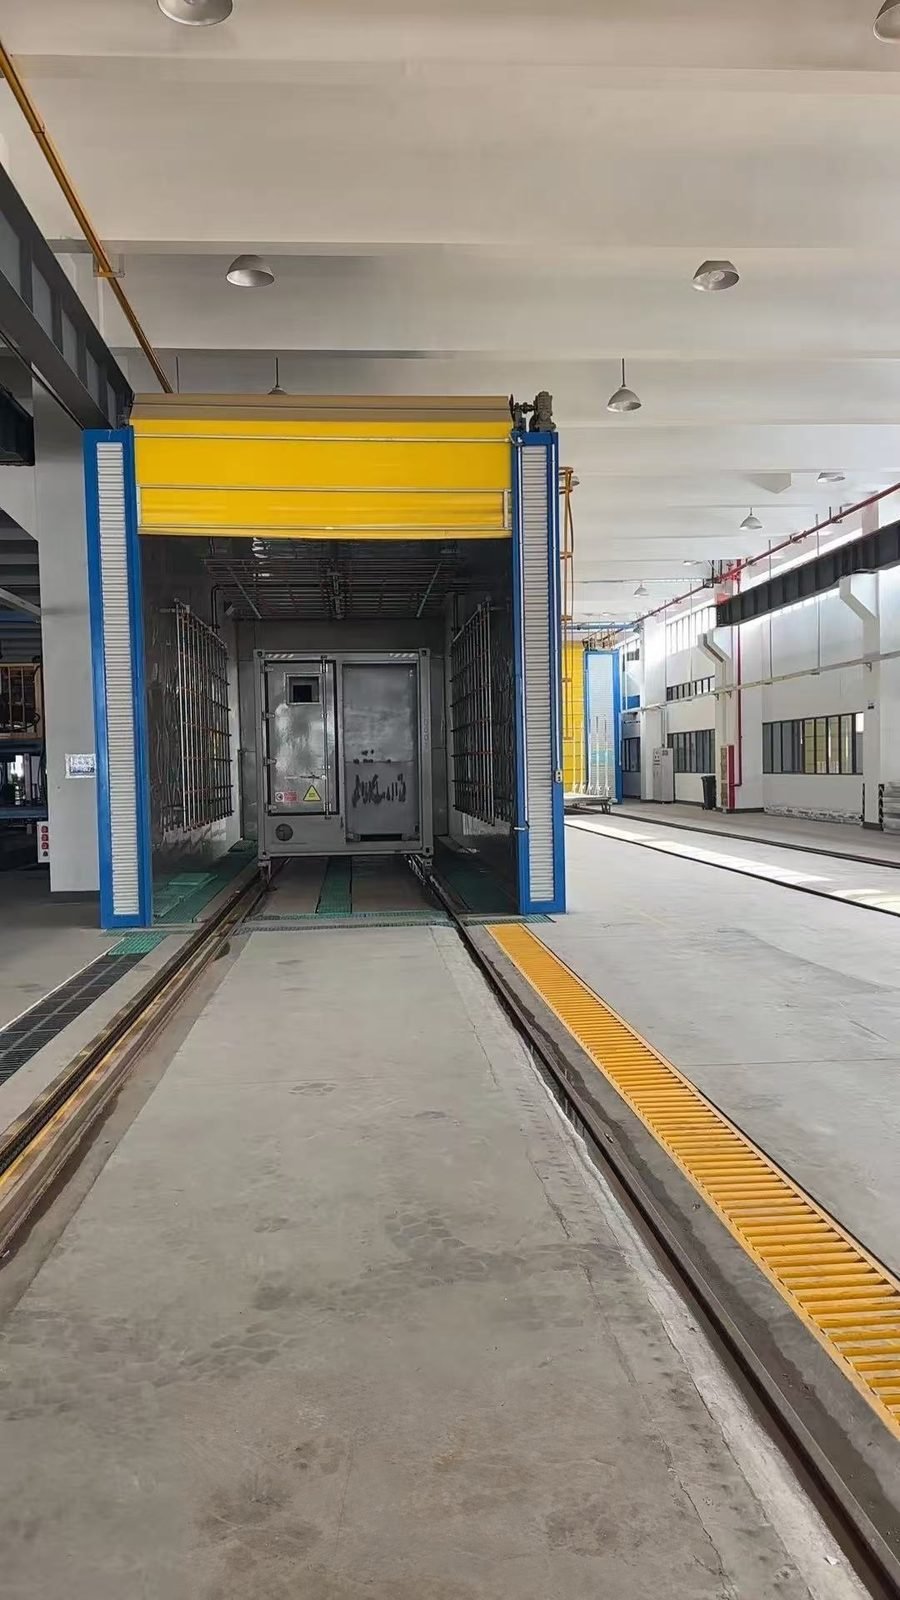
Case Study: Energy-Storage Cabinet Spray Coating Line, Jiangsu
Summary
A spray coating line for residential and commercial and industrial (C&I) energy-storage enclosures at a sheet-metal enclosure manufacturer in Jiangsu that supplies Jiangsu Zhitai New Energy, a battery and energy-storage system maker founded in 2018 with a Jiangsu base in volume production since 2024 at 4 GWh of prismatic cell capacity. The line comprises surface preparation for steel boxes and cabinets, spray booths with room to reach doors, frames and interior faces, drying and cooling, a transfer system between stations, and exhaust with VOC treatment, so home storage boxes and C&I cabinets receive the same film build on every face. The line is in production in 2026; the supply relationship was stated by the client to MUSI.
Project Background
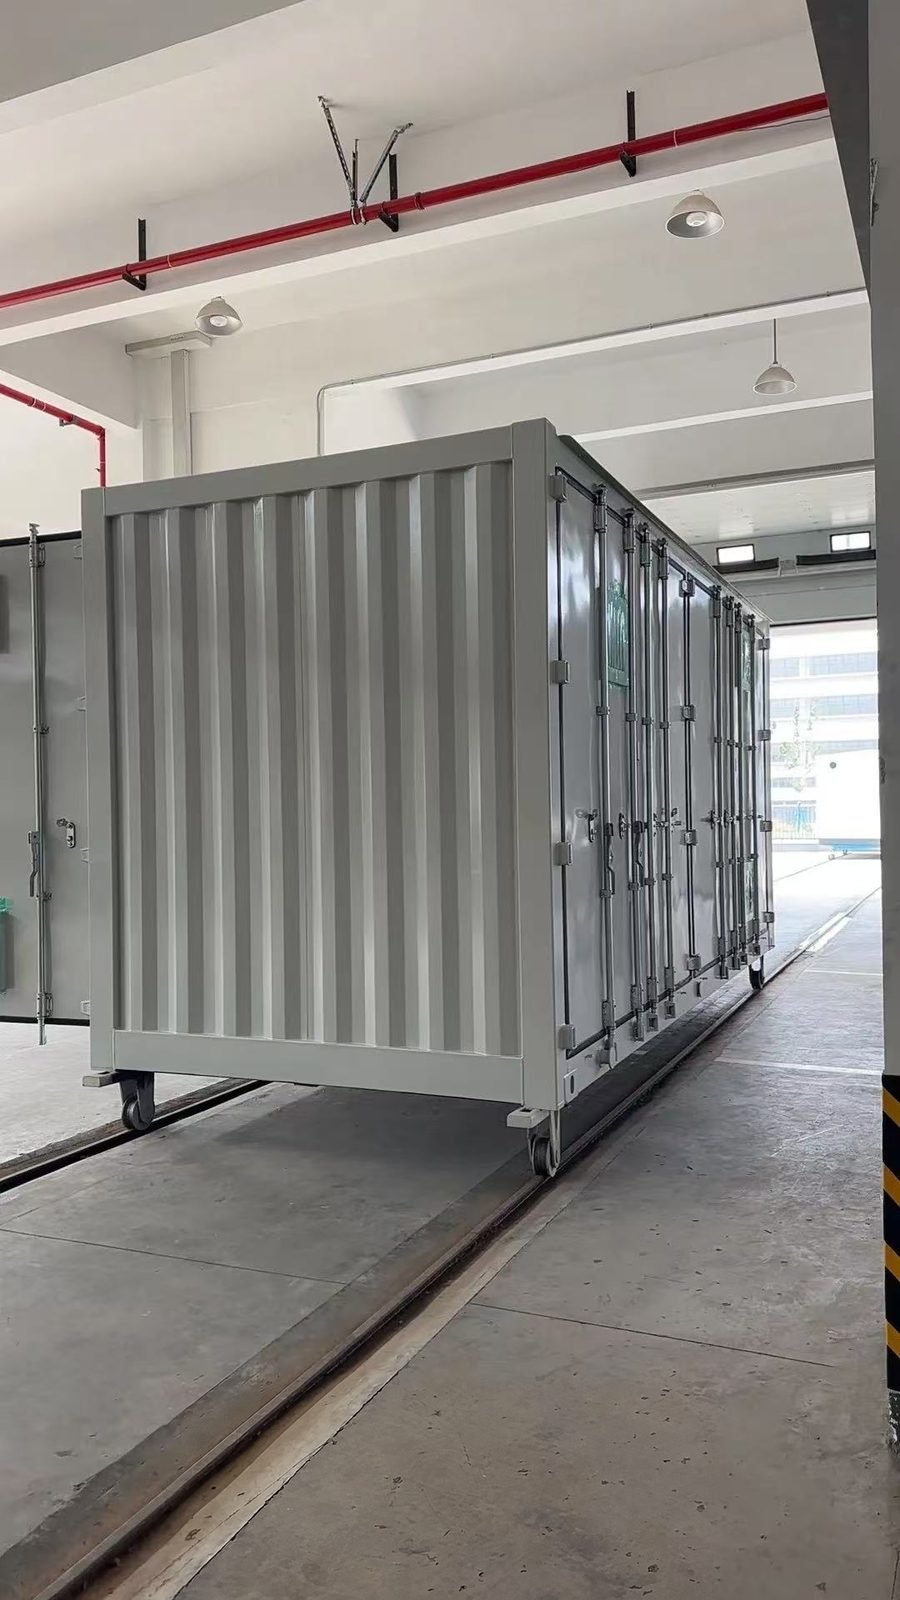
The client is a sheet-metal enclosure manufacturer in Jiangsu that builds the steel boxes and cabinets for residential and commercial and industrial (C&I) energy-storage systems, and is a supplier to Jiangsu Zhitai New Energy, a battery and energy-storage system maker founded in 2018 whose Jiangsu base started volume production in 2024 with 4 GWh of prismatic cell capacity and whose products include residential systems, containers and outdoor cabinets. Rising orders for home and C&I storage enclosures required a dedicated spray coating line, and MUSI supplied it.
The enclosures leave the client as bare painted steel and are fitted out by Zhitai with battery modules, BMS and power electronics, so the finish has to survive outdoor service for the life of the system and match Zhitai's colour and appearance standard from the first batch.
The Challenge
An outdoor energy-storage cabinet stands in sun, rain and salt air for the whole life of the battery system inside it. The steel enclosure needs a durable, even finish on every face, door and seam, including the inside surfaces, and the paint shop has to keep up as the battery maker it supplies scales from cells to complete systems.
MUSI's Solution
MUSI supplied a spray coating line sized for cabinet enclosures: surface preparation, spray booths with room to reach doors, frames and interior faces, drying and cooling, with cabinets moved between stations so each one follows the same sequence and receives the same film build.
Equipment Scope
- Surface preparation for steel cabinet enclosures
- Spray booths with access to doors, frames and interior faces
- Drying and cooling
- Transfer system between stations
- Exhaust and VOC treatment
Results
The line coats the client’s outdoor energy-storage cabinets, giving the enclosure maker a finishing step that meets the appearance and corrosion requirements of the battery-system maker it supplies.
Selection logic: why this configuration
Booths sized for access to doors, frames and interior faces were chosen over standard container booths because a home storage box or C&I cabinet is far smaller than a container but has more openings per square metre of surface, and the inside faces are coated to the same standard as the outside because the battery maker inspects them. A transfer system between fixed stations was preferred to a continuous conveyor so that both product sizes follow the same sequence at the client's current volume, with room to add stations as Zhitai's orders grow.
Scope of supply and key components
| Item | Specification | Notes |
|---|---|---|
| Surface preparation | For steel enclosures: residential boxes and C&I cabinets | |
| Spray booths | Access to doors, frames and interior faces | Primer and topcoat |
| Drying and cooling | ||
| Transfer system | Between stations, both product sizes | |
| Exhaust and VOC treatment |
Key components
Key components are available from international brands, configurable per customer specification, so that spare parts can be sourced locally over the life of the line. Brand names below are the usual options for this type of equipment; the brands actually fitted are fixed in the contract specification.
| Component | Brands available on request |
|---|---|
| Automatic liquid guns, pumps and 2K proportioners | Graco ProMix 2KS, Sames Airmix, WAGNER AirCoat, Nordson, Binks (Carlisle Fluid Technologies) |
| Automatic powder guns and powder feed | Gema OptiGun, Nordson Encore, WAGNER PEA-X1, Sames (formerly SAMES KREMLIN) |
| Oven and dryer gas burners | Riello RS series, Weishaupt monarch WM-G, Baltur TBG, Honeywell Maxon OVENPAK, Eclipse |
| PLC and HMI | Siemens SIMATIC S7-1500, Mitsubishi Electric MELSEC iQ-R, Schneider Electric Modicon, OMRON NX, Rockwell Automation Allen-Bradley |
| Variable-frequency drives | ABB ACS580, Siemens SINAMICS G120, Danfoss VLT, Schneider Electric Altivar, Yaskawa, Mitsubishi Electric |
| Booth ceiling and intake filter media | Freudenberg Viledon, AAF SureStop, Camfil, MANN+HUMMEL |
| Pretreatment pumps and chemistry | Grundfos CR, KSB Etanorm, Xylem; Henkel BONDERITE, Chemetall Gardobond, PPG Zircobond, Nippon Paint |
| RTO ceramic media and burners | Lantec MLM, Honeywell Maxon line burners, Riello RS, Eclipse |
Not included in the scope of supply
- Civil works, foundations and pits
- Building services up to the battery limit: power supply, gas, compressed air, water and drainage
- Local permits, emission approvals and third-party inspections
- Paint or powder supply, unless stated in the contract
Services included with every line: engineering design, manufacturing, shipping documentation, installation supervision, commissioning, operator training, warranty and spare parts.
Typical programme
The durations below are typical for equipment of this class and are given for planning; they are not the recorded schedule of this project. A complete line usually runs 90–180 days from contract to acceptance, a single unit 30–60 days.
| Stage | Typical duration | What happens |
|---|---|---|
| Site survey and workpiece review | 5–10 days | Remote review of drawings and photos, or an engineer visit |
| Layout and detail design | 15–30 days | Layout drawing, utilities list and specification sign-off |
| Manufacturing | 45–90 days | Booths, ovens, conveyor, pretreatment and controls built and pre-assembled at the works |
| Shipping | 20–45 days | Sea freight; equipment shipped in sections for on-site assembly |
| Installation | 15–40 days | MUSI supervision with the client's installation crew or MUSI crew |
| Commissioning, training and acceptance | 7–15 days | Trial runs on the client's parts, operator training, acceptance record |
Applicability and limits
The configuration suits residential boxes and C&I cabinets in the volumes of an enclosure supplier to one or two battery-system makers; a plant producing 20-ft containers at high takt uses the container-scale layout in the related case studies. The corrosion system and colour are set by the battery-system maker's specification.
Results shown in this case study reflect the stated operating conditions and should not be interpreted as guaranteed performance under different feed, production, environmental, or site conditions.
After-sales and spare parts
Warranty on a MUSI coating line runs from acceptance: 12 months on the complete line excluding consumables, 36 months on critical components such as motors, drives and the PLC, and 60 months on structural parts such as steel structure, ducting and oven bodies. Failures within warranty, excluding misuse, are repaired free of charge.
Support starts remotely: the service line is staffed around the clock, a preliminary diagnosis with recommendations is given within 2 hours, and where a site visit is needed an engineer reaches any major city within 72 hours. A spare-parts inventory is held at the Changzhou headquarters with same-day shipping, and customers can keep a dedicated parts stock at MUSI for emergencies. Details are on the after-sales service page.
FAQ
What is different about coating enclosures for a battery-system maker? The battery maker specifies colour, film build and corrosion performance and inspects interior faces as well as exterior ones, so booths are sized for access and every box follows the same recipe.
Can residential boxes and C&I cabinets share one line? Yes; both are steel enclosures with doors and seams, and the transfer system moves each size through the same surface preparation, primer, topcoat and drying sequence.
Why a transfer system rather than a conveyor? At an enclosure supplier's volume, fixed stations with a transfer system keep every unit on the same sequence with less equipment, and stations can be added as orders grow.
What surface preparation is used for storage enclosures? Degreasing and a conversion coating, or light blasting, depending on the steel and the corrosion system the battery maker specifies.
Who is the end customer of these enclosures? Jiangsu Zhitai New Energy, which fits the painted enclosures with battery modules, BMS and power electronics for residential and C&I storage systems.
Next step: a configuration proposal for a similar line
If your parts, volumes or plant conditions are close to this project, MUSI can return a line configuration and layout proposal. To prepare it we need four things:
- Photos and dimensions of the workpieces, with weight and material
- Required output (pieces per hour or per day, and shifts)
- Number of colours and how often colour changes are needed
- Available floor space and ceiling height, with the utilities on site
Message us on WhatsApp with these details, or use the quotation form.
Published 2026-09-26 · Updated 2026-09-30 · Last technical review: 2026-09-30
Get a Similar Solution
If your industry and requirements match this case, contact MUSI to schedule a free consultation. We'll design an optimal solution based on your specific workpieces, capacity, and facility.
Provided by Lin Cong, Technical Director, MUSI Technology