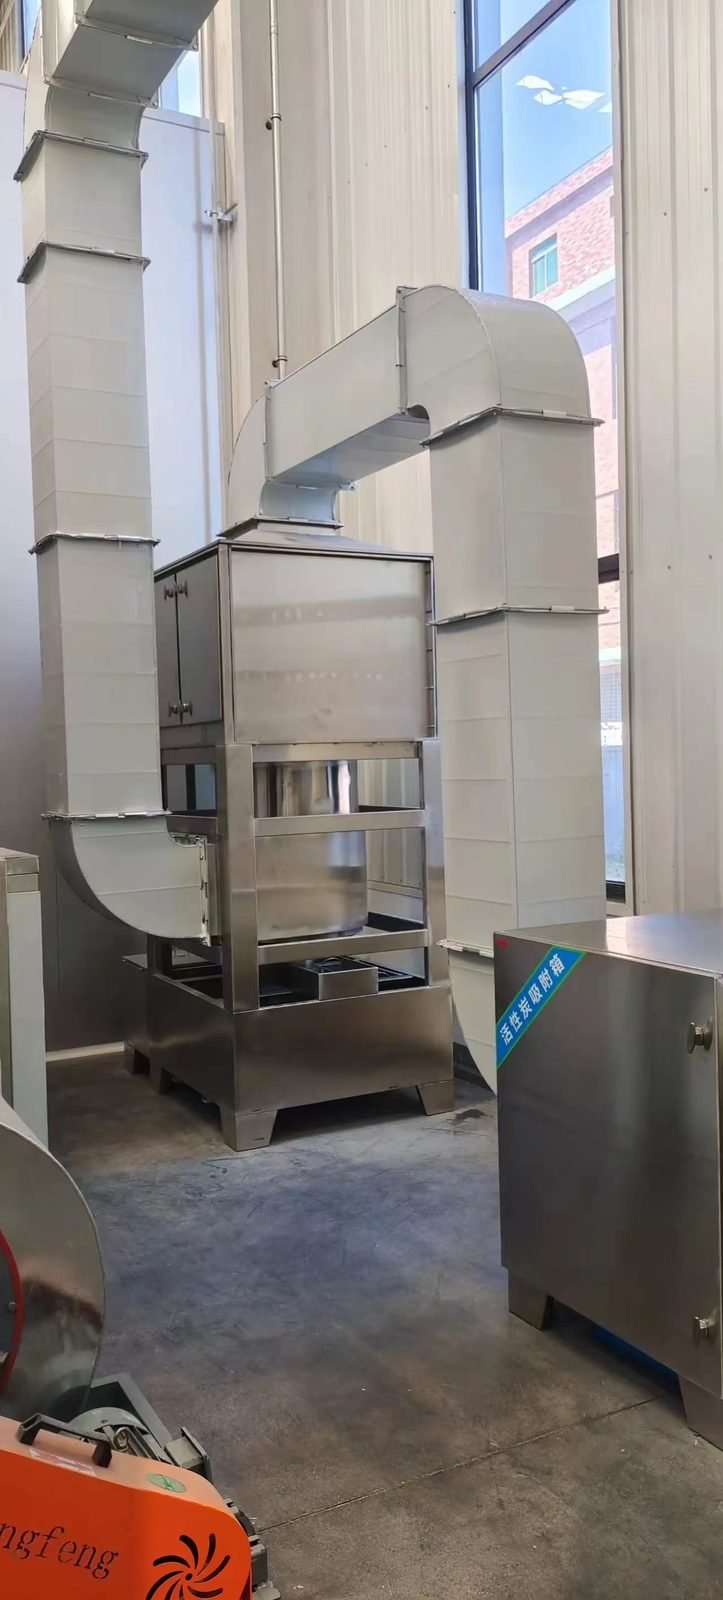
Oil-Film Paint Mist Purifier
Paint overspray capture unit that traps mist on oil-wetted surfaces instead of throw-away filters — 98% or more mist removal, oil drained and refilled on a schedule, and clean air delivered to the carbon or RCO stage behind it.
Built for booths that paint every day with high-build epoxies and polyurethanes, where dry filters would be changed too often and a water curtain is not wanted.
Technical Specifications
Values below are typical ranges for this equipment; the figures for your unit are fixed in the written specification after we review your booth, paint consumption and emission limit.
| Mist removal | 98% or more of paint overspray (design value) |
|---|---|
| Unit size | Typical 1,800 x 1,800 x 3,450 mm per unit; 2-3 units per 12-13 m booth |
| Airflow per unit | Typical 10,000-18,000 m3/h at 0.3 m/s or more booth cross-draft |
| Capture medium | Circulating oil film on stainless or galvanised plates, no water, no flocculant |
| Consumable | Paint-laden oil drained and replaced; interval set by paint volume |
| Downstream | Activated carbon boxes or adsorption-catalytic (RCO) unit |
| Construction | 1.5-2 mm galvanised or stainless housing, inspection doors, drain valve |
| Pressure drop | Low and stable; no rise with paint load as in dry media |
| Fan | Centrifugal exhaust fan sized for the booth, VFD optional |
| Noise | 85 dB(A) or less at the fan |
Configuration
- Oil-film capture modules in series at the booth exhaust wall
- Oil sump with level gauge, drain valve and refill connection
- Mist eliminator section before the outlet
- Galvanised ducting to the exhaust fan and treatment unit
- Differential pressure gauge and inspection doors
- Optional stainless construction for aggressive solvents
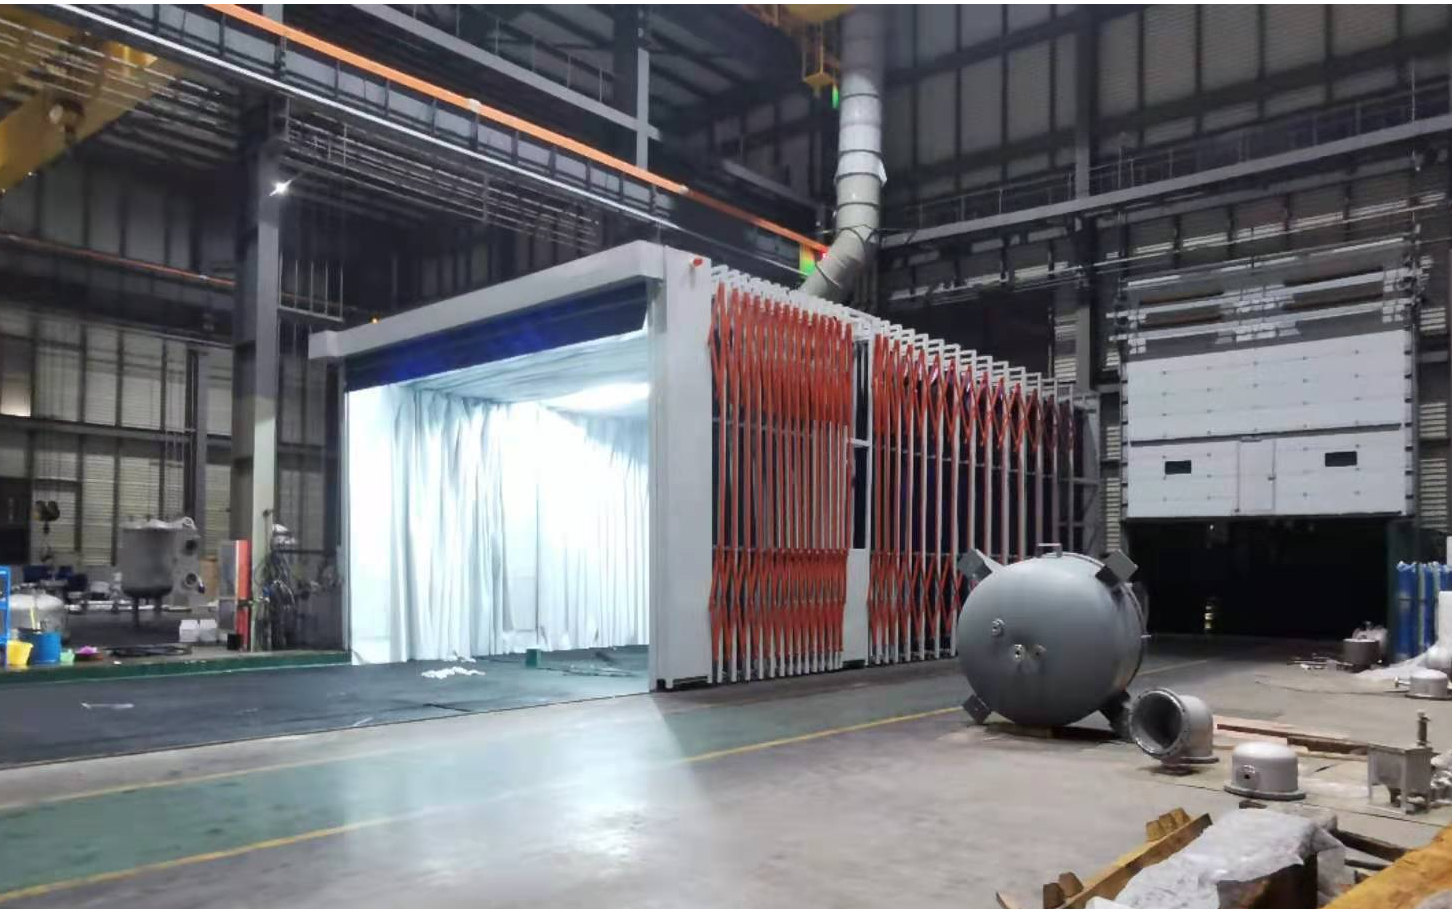
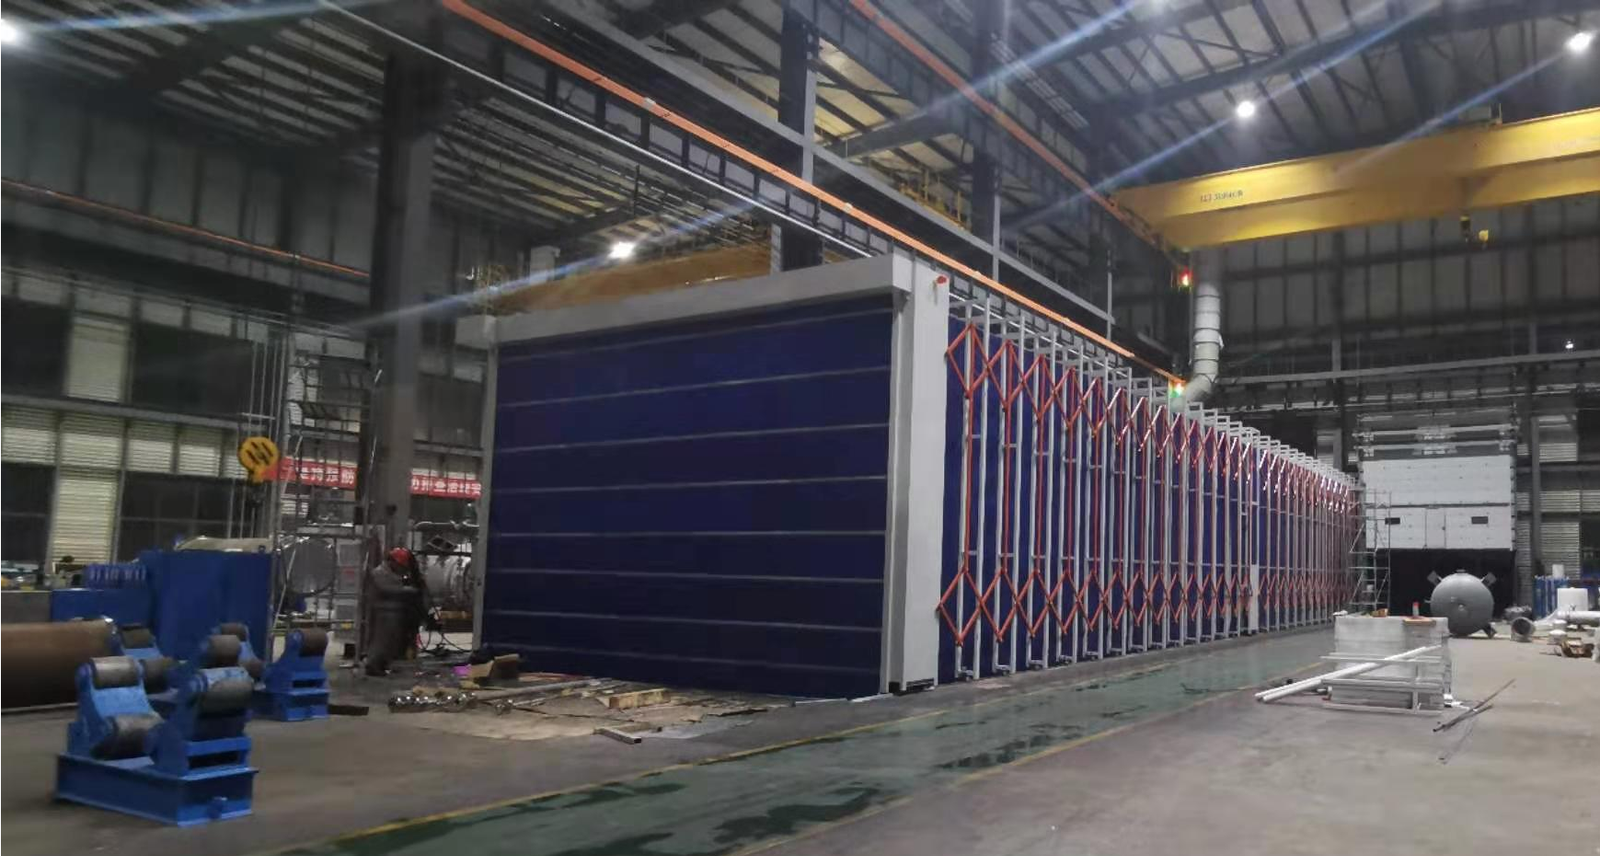
Oil-Film Paint Mist Purifier in Practice
Application References
Pressure vessel and tank builders, machinery and crane manufacturers, shipyards and any liquid spray booth with daily painting where filter waste and catalyst protection matter.
Engineering Commitment
Every unit is engineered against a written performance specification. Mist capture, airflow, pressure drop and noise are stated in the contract and demonstrated at commissioning. One engineering team owns the booth, the capture stage and the exhaust treatment behind it, so the three are sized as one system.
Service & Delivery
Standard configurations ship in 30-60 days with a 12-month full-machine and 36-month critical-component warranty. On-site installation, commissioning and operator training are available worldwide, and filter media, oil and carbon supply continue for the working life of the unit.
Frequently Asked Questions
When is oil film better than dry filters?
When the booth paints every day: the oil is drained and replaced instead of filters being thrown away, the pressure drop stays stable, and the clean air protects a carbon or catalyst stage downstream.
Does it replace VOC treatment?
No. It removes the paint droplets; solvent vapour still goes to carbon, UV or RCO treatment behind it.
How many units does a booth need?
Follows the booth cross-section and airflow; a 12 x 7 m booth at 0.3 m/s uses three units, a 13 x 5 m booth two.
What happens to the used oil?
It is drained into drums and handled as paint-contaminated waste under local rules; the sump is refilled with fresh oil.
What do you need for a quotation?
Booth width and height, daily paint consumption and paint type, and the treatment unit the air will go to.