Telescopic Spray Booths for Steel Structure Fabrication: Beams, Columns and Trusses
Quick answer: In a structural steel shop the crane already moves every beam and column, so a telescopic booth on rails in the painting bay lets the crane set members on stands, the booth close over them, and the painters apply primer and topcoat with airless guns while the exhaust fan draws overspray into a dry filter wall. A 20 x 10 x 4 m booth covers a batch of 12-15 m members; a 12 x 5 m booth suits smaller sections and connection plates.
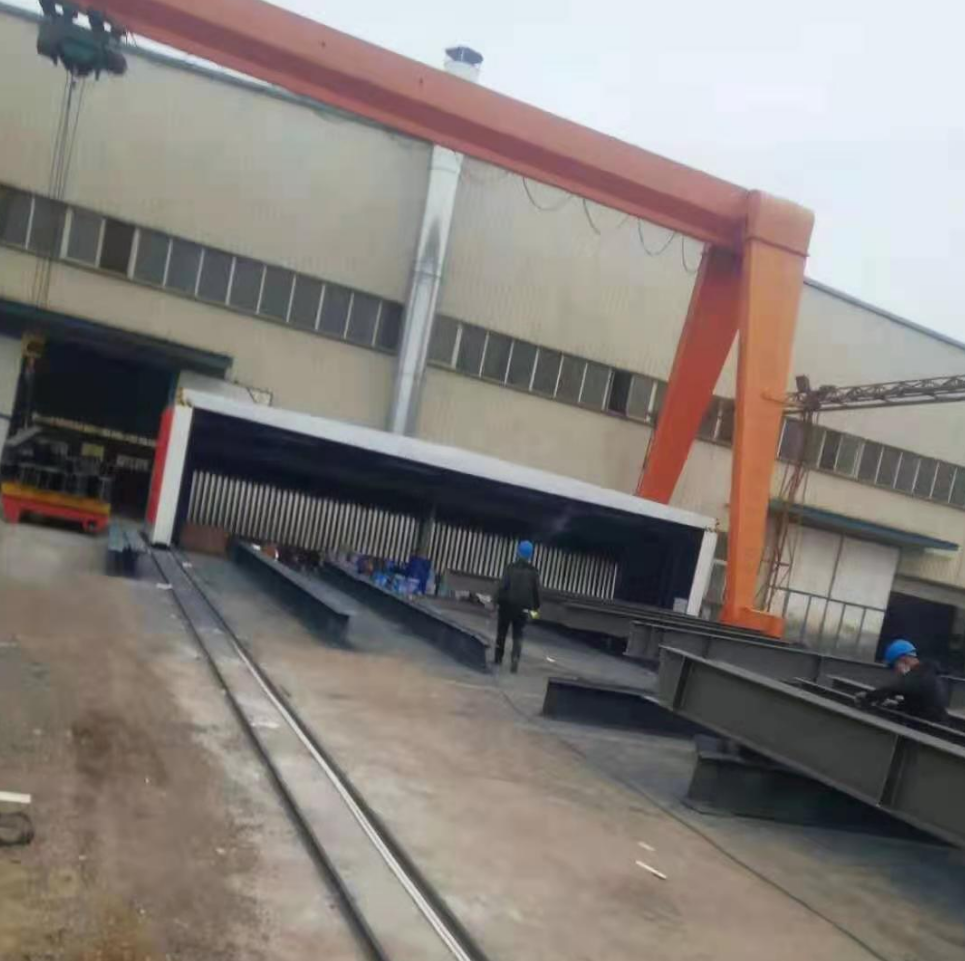
What does the workflow look like?
Members come from blasting on rollers or by crane and are set on stands inside the booth footprint, spaced so painters can reach all faces. The booth is driven closed, the fan and lights are started, and primer is applied by airless spray. After flash-off the topcoat follows, or the members are moved to a drying area and the next batch loaded. Because the booth retracts to about 3 m, the same bay is used for fit-up when painting stops.
Indoor or outdoor?
Where the shop has no spare bay, the booth is laid on rails outside under the gantry crane. The fixed end with the filter wall, fan and stack stays in one place; the fabric is UV-stabilised. Members are laid across the rail centreline on stands so the retracted booth clears them.
How is the booth sized for steel?
Length follows the longest member plus 2 m; width follows the number of members painted at once (a 10 m wide booth takes four or five beams on stands with walking space); height follows the tallest column laid flat plus 1.5 m. At 0.3 m/s cross-draft a 10 x 4 m section needs about 43,000 m3/h, typically a 75 kW fan. Zinc-rich primers and high-build epoxies are heavy on overspray, so the labyrinth paper filter stage is essential ahead of the glass-fibre bags and the carbon or RCO unit.
| Item | Typical |
|---|---|
| Primer | zinc-rich epoxy, 60-80 microns |
| Intermediate | epoxy MIO where specified |
| Topcoat | polyurethane or polysiloxane |
| Total DFT | 200-320 microns for ISO 12944 C4-C5 |
| Application | airless spray, 1-4 painters |
| Booth | 12-20 m long, dry filter, carbon or RCO |
What about drying?
Structural coatings are normally air-dried on stands or in a warm drying area; where the schedule needs forced drying, a separate drying room is laid out next to the booth and members are moved by crane after flash-off. The booth itself is used for painting only, which keeps its fabric enclosure simple.
FAQ
Can the booth handle 15 m members? Yes, length is built in 1 m modules; 20 m booths are standard.
How many painters work at once? One to four, each with an airless unit; the airflow is sized for the section, not the painter count.
Is blasting done in the same booth? No; blasting needs an abrasive recovery floor. Use a shot blasting machine or blast room first.
What emission treatment is usual for steel shops? Carbon boxes for intermittent work; RCO where the shop paints every day.
Where MUSI Technology fits
MUSI supplies telescopic booths for steel fabricators together with roller-conveyor shot blasting and drying rooms where a full line is required. Product details, typical sizes and the quotation checklist are on the telescopic mobile spray booth page.
Provided by Lin Cong, Technical Director, MUSI Technology
Send us your part size, throughput and coating type — our engineers reply with a layout and budget within one working day. Contact MUSI Technology or browse our equipment range.
Related technical guides
- Metal Hardware Coating Line: Design & Cost per Part
Hardware plants live on variety, not volume. Dense hanging, 10-25 minute colour change, rack design and the real cost per coated part, with line. - Industrial Dust Collection Systems: Sizing & Cost
An industrial dust collector keeps coating and blasting shops under the 10-20 mg/m3 particulate limit. Types, airflow sizing formulas and 2026 cost ranges. - Aluminium Profile Coating Line: Vertical vs Horizontal
Vertical aluminium profile coating lines handle 6-7 m extrusions with less handling damage and a smaller footprint; horizontal lines cost less and suit. - Blasting Media Selection Guide: Which Abrasive?
Which abrasive for which job: steel shot and grit, garnet, aluminium oxide and glass bead compared on hardness, profile produced, reuse cycles,. - Sandblasting & Shot Peening Equipment Guide 2026
Compare rotary table, hook type, tumble belt and roller conveyor blast machines: working principle, specifications, applications and cost ranges.